IN SUMMER TRAINING REPORT AT ARVIND LIMITED
BY
ANUPAM BHOWMICK
DEPARTMENT OF TE FIBER TECHNOLOGY
INSTITUTE OF JUTE TECHNOLOGY
UNIVERSITY OF CALCUTTA
IN KNITS FINISHING DIVISION
ACKNOWLEDGEMENT
As part of our syllabus, I have undergone industrial training in Arvind Limited at
KHATRAJ KNITS MARKETING DIVISION, from 01-07-2016 to 31-08-2016. First of all, I
are very thankful to whole Arvind Group for providing me the best facility & good
environment during the whole training period.
I would like to express our heartiest gratitude to Mr. Subhanish Malhotra (H.R.
Manager) and Ms. Krupa Raval (HR) who granted us the permission to undergo training
in such a prestigious organization. I am also very grateful to our instructors Mr. Kalyan
Bhattacharyya (Head of Knits Marketing) and Mr. Hiren B. Patel (Manager) & Mr.
Azaruddin Solanki who gave their valuable time, guidance and gave attention on us
during our whole training period.
Finally I would like to thank all the mill employees for their cooperation and support
without which it would not have been possible for us to make such an understanding
about the different aspects. I am very happy to have attended this training because of
the support every person of the department extended to us; they gave us a lot of
information and knowledge about the machines.
I am also greatly indebted to the teachers of our institution, Prof. Swapan Kumar
Ghosh (H.O.D.) and Prof. Debasish Das who helped in coordinating the program. I am
very grateful to all our teachers at Institute of Jute Technology, Department of Jute and
Fibre Technology, University of Calcutta who developed our knowledge and widened
our view, instilled interest in the subject and encouraged us to undertake this training
in a renowned industry even so far away from our University.
OBJECTIVE OF THE MILL TRAINING
The making of a technologist not only comprises of theoretical knowledge
but it should be supplemented by through practical knowledge.
It is necessary for young technologist to undergo a rigorous onsite training
schedule to master the technology of actual machinery set up and
production procedure, as well as intricacies of personal dealings.
Both with management staff and also with actual production operations.
The training programme also enables a trainee to face situation both
beneficial and adverse and to react on them in proper and satisfied
manner. Under the proper guidance of seniors, this online practical
training gives a much needed experience to the fresher to get accustomed
to the working condition of the mill, before stepping in the real business of
serving in industry.
Therefore the education of a technical student is never complete until and
unless he perceives the whole.
KNITTING:
Knitting is the technique of fabric formation by
interlooping one or one set of yarn. The most
essential unit in a knit fabric is the loop or stitch. A
vertical row of stitches is called a ‘wale’; the
horizontal or crosswise row of stitches is known as a
‘course’.
BASIC KNIT FABRICS PRODUCED IN ARVIND MILL
Plain(J)
Rib(R)
Interlock(I)
Pique(P)
Special(SP)
TYPES OF FIBRE AND FIBRE BLEND USED IN ARVIND MILL
100% cotton
100% viscose
Cotton lycra blend
Viscose lycra blend
Polyester cotton blend
Viscose cotton blend
STYLE CODE of ARVIND MILL
It is very much important too read the style code for finishing purpose.
From this code we can easily understand the parameters of the fabric like
knit pattern , fiber used, count, etc.
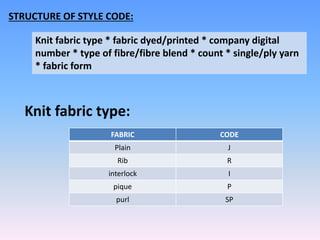
STRUCTURE OF STYLE CODE:
Knit fabric type * fabric dyed/printed * company digital
number * type of fibre/fibre blend * count * single/ply yarn
* fabric form
Knit fabric type:
FABRIC CODE
Plain J
Rib R
interlock I
pique P
purl SP
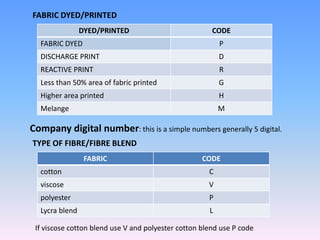
FABRIC DYED/PRINTED
DYED/PRINTED CODE
FABRIC DYED P
DISCHARGE PRINT D
REACTIVE PRINT R
Less than 50% area of fabric printed G
Higher area printed H
Melange M
Company digital number: this is a simple numbers generally 5 digital.
TYPE OF FIBRE/FIBRE BLEND
FABRIC CODE
cotton C
viscose V
polyester P
Lycra blend L
If viscose cotton blend use V and polyester cotton blend use P code
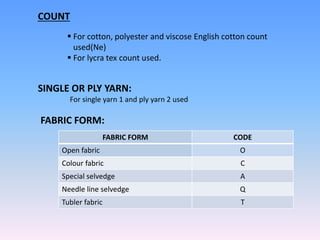
COUNT
 For cotton, polyester and viscose English cotton count
used(Ne)
 For lycra tex count used.
SINGLE OR PLY YARN:
For single yarn 1 and ply yarn 2 used
FABRIC FORM:
FABRIC FORM CODE
Open fabric O
Colour fabric C
Special selvedge A
Needle line selvedge Q
Tubler fabric T
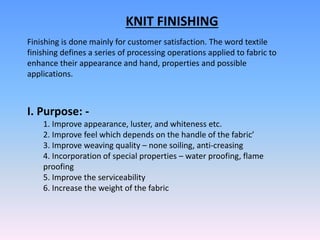
KNIT FINISHING
Finishing is done mainly for customer satisfaction. The word textile
finishing defines a series of processing operations applied to fabric to
enhance their appearance and hand, properties and possible
applications.
I. Purpose: -
1. Improve appearance, luster, and whiteness etc.
2. Improve feel which depends on the handle of the fabric’
3. Improve weaving quality – none soiling, anti-creasing
4. Incorporation of special properties – water proofing, flame
proofing
5. Improve the serviceability
6. Increase the weight of the fabric
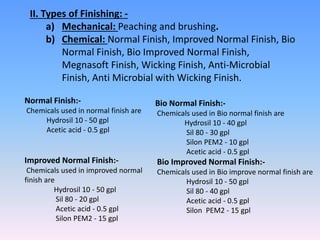
II. Types of Finishing: -
a) Mechanical: Peaching and brushing.
b) Chemical: Normal Finish, Improved Normal Finish, Bio
Normal Finish, Bio Improved Normal Finish,
Megnasoft Finish, Wicking Finish, Anti-Microbial
Finish, Anti Microbial with Wicking Finish.
Normal Finish:-
Chemicals used in normal finish are
Hydrosil 10 - 50 gpl
Acetic acid - 0.5 gpl
Improved Normal Finish:-
Chemicals used in improved normal
finish are
Hydrosil 10 - 50 gpl
Sil 80 - 20 gpl
Acetic acid - 0.5 gpl
Silon PEM2 - 15 gpl
Bio Normal Finish:-
Chemicals used in Bio normal finish are
Hydrosil 10 - 40 gpl
Sil 80 - 30 gpl
Silon PEM2 - 10 gpl
Acetic acid - 0.5 gpl
Bio Improved Normal Finish:-
Chemicals used in Bio improve normal finish are
Hydrosil 10 - 50 gpl
Sil 80 - 40 gpl
Acetic acid - 0.5 gpl
Silon PEM2 - 15 gpl
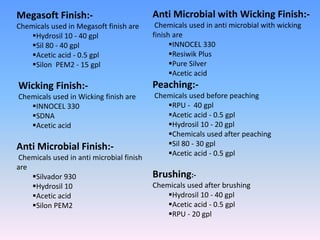
Megasoft Finish:-
Chemicals used in Megasoft finish are
Hydrosil 10 - 40 gpl
Sil 80 - 40 gpl
Acetic acid - 0.5 gpl
Silon PEM2 - 15 gpl
Wicking Finish:-
Chemicals used in Wicking finish are
INNOCEL 330
SDNA
Acetic acid
Anti Microbial Finish:-
Chemicals used in anti microbial finish
are
Silvador 930
Hydrosil 10
Acetic acid
Silon PEM2
Anti Microbial with Wicking Finish:-
Chemicals used in anti microbial with wicking
finish are
INNOCEL 330
Resiwik Plus
Pure Silver
Acetic acid
Peaching:-
Chemicals used before peaching
RPU - 40 gpl
Acetic acid - 0.5 gpl
Hydrosil 10 - 20 gpl
Chemicals used after peaching
Sil 80 - 30 gpl
Acetic acid - 0.5 gpl
Brushing:-
Chemicals used after brushing
Hydrosil 10 - 40 gpl
Acetic acid - 0.5 gpl
RPU - 20 gpl
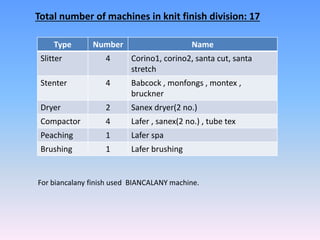
Total number of machines in knit finish division: 17
Type Number Name
Slitter 4 Corino1, corino2, santa cut, santa
stretch
Stenter 4 Babcock , monfongs , montex ,
bruckner
Dryer 2 Sanex dryer(2 no.)
Compactor 4 Lafer , sanex(2 no.) , tube tex
Peaching 1 Lafer spa
Brushing 1 Lafer brushing
For biancalany finish used BIANCALANY machine.
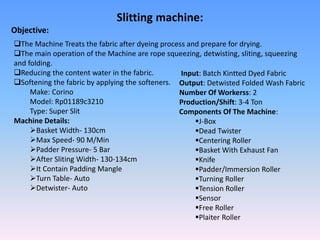
Slitting machine:
Objective:
The Machine Treats the fabric after dyeing process and prepare for drying.
The main operation of the Machine are rope squeezing, detwisting, sliting, squeezing
and folding.
Reducing the content water in the fabric.
Softening the fabric by applying the softeners.
Make: Corino
Model: Rp01189c3210
Type: Super Slit
Machine Details:
Basket Width- 130cm
Max Speed- 90 M/Min
Padder Pressure- 5 Bar
After Sliting Width- 130-134cm
It Contain Padding Mangle
Turn Table- Auto
Detwister- Auto
Input: Batch Kintted Dyed Fabric
Output: Detwisted Folded Wash Fabric
Number Of Workerss: 2
Production/Shift: 3-4 Ton
Components Of The Machine:
J-Box
Dead Twister
Centering Roller
Basket With Exhaust Fan
Knife
Padder/Immersion Roller
Turning Roller
Tension Roller
Sensor
Free Roller
Plaiter Roller
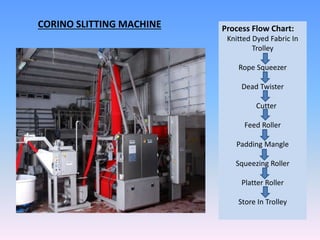
Process Flow Chart:
Knitted Dyed Fabric In
Trolley
Rope Squeezer
Dead Twister
Cutter
Feed Roller
Padding Mangle
Squeezing Roller
Platter Roller
Store In Trolley
CORINO SLITTING MACHINE
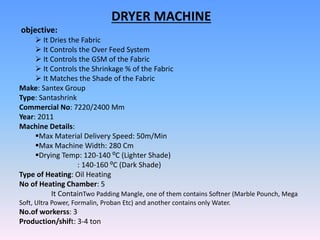
DRYER MACHINE
objective:
 It Dries the Fabric
 It Controls the Over Feed System
 It Controls the GSM of the Fabric
 It Controls the Shrinkage % of the Fabric
 It Matches the Shade of the Fabric
Make: Santex Group
Type: Santashrink
Commercial No: 7220/2400 Mm
Year: 2011
Machine Details:
Max Material Delivery Speed: 50m/Min
Max Machine Width: 280 Cm
Drying Temp: 120-140 ⁰C (Lighter Shade)
: 140-160 ⁰C (Dark Shade)
Type of Heating: Oil Heating
No of Heating Chamber: 5
It ContainTwo Padding Mangle, one of them contains Softner (Marble Pounch, Mega
Soft, Ultra Power, Formalin, Proban Etc) and another contains only Water.
No.of workerss: 3
Production/shift: 3-4 ton
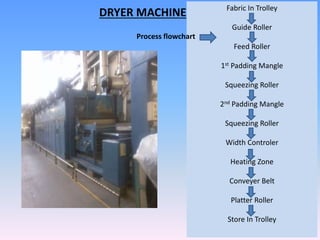
Fabric In Trolley
Guide Roller
Feed Roller
1st Padding Mangle
Squeezing Roller
2nd Padding Mangle
Squeezing Roller
Width Controler
Heating Zone
Conveyer Belt
Platter Roller
Store In Trolley
DRYER MACHINE
Process flowchart
Objective:
Width of the fabric is control the stenter
Heat setting is done for lycra, synthetic and blend fabric
Finishing chemical apply on the fabric by the stenter
Loop of the knit fabric is control
Moisture of the fabric is control
Spirality of the fabric is control
GSM of the fabric is control by the stenter
Fabric is dried by the stentering process
Shrinkage property of the fabric is control by the stenter
Curring treatment for resin, water repellent of fabric is
done by the stenter
STENTER MACHINE
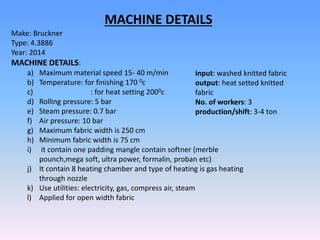
Make: Bruckner
Type: 4.3886
Year: 2014
MACHINE DETAILS:
a) Maximum material speed 15- 40 m/min
b) Temperature: for finishing 170 0c
c) : for heat setting 2000c
d) Rolling pressure: 5 bar
e) Steam pressure: 0.7 bar
f) Air pressure: 10 bar
g) Maximum fabric width is 250 cm
h) Minimum fabric width is 75 cm
i) it contain one padding mangle contain softner (merble
pounch,mega soft, ultra power, formalin, proban etc)
j) It contain 8 heating chamber and type of heating is gas heating
through nozzle
k) Use utilities: electricity, gas, compress air, steam
l) Applied for open width fabric
input: washed knitted fabric
output: heat setted knitted
fabric
No. of workers: 3
production/shift: 3-4 ton
MACHINE DETAILS
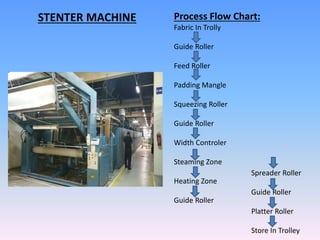
Process Flow Chart:
Fabric In Trolly
Guide Roller
Feed Roller
Padding Mangle
Squeezing Roller
Guide Roller
Width Controler
Steaming Zone
Heating Zone
Guide Roller
Spreader Roller
Guide Roller
Platter Roller
Store In Trolley
STENTER MACHINE
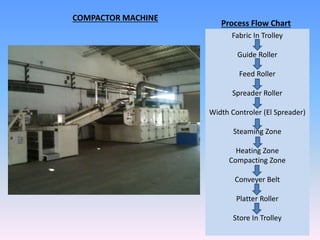
COMPACTOR MACHINE
OBJECTIVE:
A) It Controls the GSM of the Fabric
B) It Controls the Shrinkage %
C) It Increases Smoothness of Fabric
D) Heat Setting is done for Fabric
Santex New & old(open width compactor )
Make: Santex
Model: New Santa Compact 240
Year: 2004
Machine Details:
Fabric Speed: 5- 50 M/Min
Temperature: 110- 140 ⁰C
Maximum Fabric Width: 220
Cm
Minimum Fabric Width: 90cm
Air Pressure: 6 Bar
Steam pressure: 6bar
saturated steam
Used utilities: electricity,
compress air, steam
Applied for: open width
Input: dry fabric
Output: compacted fabric
Number of workerss: 3
Production/shift: 2-3 ton
Fabric In Trolley
Guide Roller
Feed Roller
Spreader Roller
Width Controler (El Spreader)
Steaming Zone
Heating Zone
Compacting Zone
Conveyer Belt
Platter Roller
Store In Trolley
Process Flow Chart
COMPACTOR MACHINE
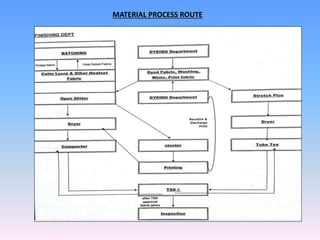
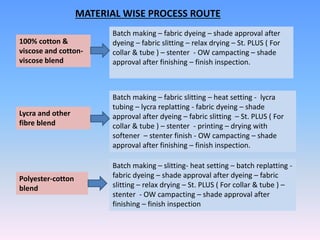
MATERIAL PROCESS ROUTE
Batch making – fabric dyeing – shade approval after
dyeing – fabric slitting – relax drying – St. PLUS ( For
collar & tube ) – stenter - OW campacting – shade
approval after finishing – finish inspection.
Batch making – fabric slitting – heat setting - lycra
tubing – lycra replatting - fabric dyeing – shade
approval after dyeing – fabric slitting – St. PLUS ( For
collar & tube ) – stenter - printing – drying with
softener – stenter finish - OW campacting – shade
approval after finishing – finish inspection.
Batch making – slitting- heat setting – batch replatting -
fabric dyeing – shade approval after dyeing – fabric
slitting – relax drying – St. PLUS ( For collar & tube ) –
stenter - OW campacting – shade approval after
finishing – finish inspection
MATERIAL WISE PROCESS ROUTE
100% cotton &
viscose and cotton-
viscose blend
Lycra and other
fibre blend
Polyester-cotton
blend
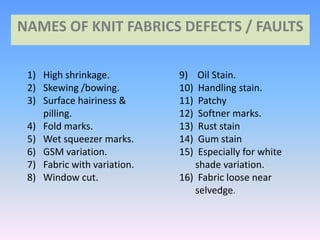
NAMES OF KNIT FABRICS DEFECTS / FAULTS
1) High shrinkage.
2) Skewing /bowing.
3) Surface hairiness &
pilling.
4) Fold marks.
5) Wet squeezer marks.
6) GSM variation.
7) Fabric with variation.
8) Window cut.
9) Oil Stain.
10) Handling stain.
11) Patchy
12) Softner marks.
13) Rust stain
14) Gum stain
15) Especially for white
shade variation.
16) Fabric loose near
selvedge.
DEFECTS CAUSES AND THEIR REMEDIES
High shrinkage: The original intended measurement of the garment go haywire during storage and after the very fast
wash.
Causes: 1) High stresses and strains exerted on the fabric during processing of the fabric and the fabric not being
allowed to relax properly, thereafter. 2) This is done due to the fabric being subject to high tension during
processing.
Remedies:
1) Keep the fabric during processing in loose platted form. 2) Allow the fabric to relax properly, before it is cut.
3) Store the finished fabric also in the platted form and not in the roll form.
4) Give maximum overfeed to the fabric during the processing on stenter and compactor machine.
Skewing and Bowing : Bowing and skewing appears as row of courses or yarn dyed or printed stripes forming bow
and skew shape along the fabric width.
Causes: Uneven distribution of tensions across the fabric width while dyeing or finishing.
Remedies: 1) Bowing and skewing can be corrected by reprocessing the fabric by feeding it from the opposite end .
2) a special arrangement (MAHLO) is also available for correcting this in fabric.
Surface hairiness and piling: it appears the form of access superfluous fibers on the surface of the fabric. Piling
appears as small fibre balls formed on the surface of the fabric.
Causes:
1) abrasion due to contact with rough surface. 2) Rough dyeing process and abrasive Machine surface.
3) Reprocessing of the fabric is also a major cause.
Remedies:
1) control shrinkage by maximum fabric relaxation and overfeed in the processing.
2) regularly inspect the fabric contact points on all the Machine s , for any rough and sharp surface.
3) avoid repeated reprocessing of the fabric. 4) use anti-piling chemical treatment for the fabric prone to piling.
DEFECTS CAUSES AND THEIR REMEDIES (cont’d)
Fold marks: it appears as distinct pressure marks along the length of the fabric.
Causes:
Too much pressure of the feeding rolls of the stenter and compactor.
Remedies: Adjust the gap between two rolls as per the fabric thickness.
Wet squeezer mark: it appears as distinct lines along the length of the fabric.
Causes:
These marks are caused due to the excessive pressure of the squeezer rolls of the padding mangle on
the wet fabric while rinsing.
Remedies:
Use the padding mangle only for the application of the softener.
GSM Variation: the fabric will appears to have a visible variation in the density , from roll to roll or
within the same roll of the same dye lot.
Cause:
1) roll to roll variation in the process parameters. 2) roll to roll variation in the fabric loop length.
Remedies:
All rolls in a lot are processed under the same process parameters.
Fabric width variation: defferent rolls of the same fabric lot having difference in the finished width of
the fabric.
Causes:
Roll to roll difference in the dyed fabric stressed with, while feeding the fabric on the stenter and
compactor.
Remedies:
The stretched width of the fabric should remain constant during processing on the stenter and
compactor.
DEFECTS CAUSES AND THEIR REMEDIES (cont’d)
Handling, Oil, Rust, Gum stain: It appears as spots or patchy of geese oil or dyes of different colour
or patchy of rust and spots of gum in a neat and clean finished fabric surface.
Causes:
1) dyeing Machine not cleaned thoroughly after dyeing a lot.
2) grease and oil stains from the unguarded moving Machine parts.
3) fabric touching the floats and other soiled places during transportation in the trolleys.
4) handling of the fabric with soiled hands and steeping on to the stored fabric with dirty feet or
shoes on.
5) improper rotation of gum wheel and improper density of gum at stenter and compactor
machine.
Remedies:
1) wash and clean the dyeing Machine thoroughly after dyeing every dye lot.
2) all the lubricated moving parts should be protected with safety guard.
3) make sure that the fabric is neatly packed in or covered with polythene sheets while transporting
and storage.
4) handle the fabric carefully. 5) check gum wheel rotation and gum condition.
Window cut: it appears like window form hole on fabric .
Causes: Inexperienced operator and care less operations.
Remedies:
Operator should be experienced and operate carefully.
DEFECTS CAUSES AND THEIR REMEDIES (cont’d)
Patchy: it appears , as random irregular patches on the surface of the dyed fabric.
Causes:
1) inadequate scouring of the fabric. 2) improper levelling agent . 3) correct pH value not
maintained. 4) Machine stoppage and fabric entanglements in the dyeing Machine. 1) scour
the fabric thoroughly.
Remedies:
2) use appropriate leveling agent, 3) maintain the correct pH., 4) avoid Machine stoppage.
Shade variation: difference in the depth of shade between roll to roll and from place to place in
the same roll.
Causes: 1) shade variation can be as a result of mixing the fabric of different lots.
2) variation in the process parameters, 3) variation in the GSM of the fabric.
Remedies:
1) ensure that the gray fabric used for one shade is knitted from same lot of the yarn.
2) maintain the proper process parameters.
Softner Marks: softner marks appears as distinct irregular patches in the dried fabric after the
application of softner.
Causes: Softner not being uniformly dissolved in water.
Remedies:
1) ensure that the Softner is uniformly dissolved in the water and does not remain undissolved as
lumps or suspensions.
2) use the right Softner and correct procedure for the application.
3) maintain the correct pH value of the Softner before application.
Spirality: it appears in the form of a twisted garment after washing.
Causes: 1) high TPI of yarn. 2) unequal rate of fabric feed on the stenter and compactor machine .
Remedies: 1) Use proper TPI in yarn. 2) Ensure uniform rate of feed.
ANUPAM BHOWMICK
B.TECH. IN JUTE & FIBRE TECHNOLOGY
(7TH SEMESTER)
DEPARTMENT OF JUTE AND FIBRE TECHNOLOGY
UNIVERSITY OF CALCUTTA