winding
MD MAHBUBAY RABBANI MIM
DHAKA UNIVERSITY OF ENGINEERING
AND TECHNOLOGY(DUET),GAZIPUR
Contact number:-01767281858
At A
Glance
2
ABOUT WINDING MACHINE
WHAT IS WINDING?
Definition: The process of transferring yarn from small packages like hank,
bobbing etc to a large package such as cones, pirns, cheese etc, containing
considerable length of yarn is called winding.
 Example: From hanks to bobbins, bobbins to cone, cone to pirn etc.
3
Objectives :
 To transfer yarn from one package to another suitable
package, this can be conveniently used for weaving purpose.
 To remove yarn faults like hairiness, neps, slubs and foreign
matters.
 To clean yarn.
 To improve the quality of yarn.
 To get a suitable package.
 To store the yarn.
 To make easier the next process.
 To preparing soft package of yarn dyeing.
4
5A BASIC DIAGRAM OF WINDING M/C:
It has three sections:
I. The unwinding zone.
II. The tension & clearing
zone.
III. The winding zone.
Types of Winding
 Precision Winding
Machine
 Non Precision Winding
M/C
According to Drive
 Direct Drive
 Indirect Drive
According to WindingAccording to the package
 Pirn Winding Machine
 Cop Winding Machine
 Spool Winding Machine
 Cone Winding Machine
 Cheese Winding Machine
 Warp Winding Machine
 Flange Bobbin Winding
M/C
6
Types of Winding Packages
 Pirn
 Cop
 Flanged
bobbin
Cross Wound
Package
 Cone
 Cheese
Near Parallel Wound
Package
Parallel wound package
 Warp beam
Weavers beam
7
8
Precision winding Non precision winding
1. The wound coil is arranged parallel or near
parallel.
1. The coil is cross wise wound.
2.The yarn density of the package
Is high.
2. The yarn density of the package
Is low.
3.Flanged bobbin may be used. 3.Not used of flanged.
4.The yarn package is hard & more compact 4. The yarn package is soft and less compact.
5.Low stability of the package. 5.High stability of the package.
6.winding angle is 90° or near 90°. 6.Winding angle is less than 80°.
7.The bobbin is wound with precision winding. 7.The bobbin is wound with non precision winding.
8.Yarn tension is comparatively high. 8.yarn tension is comparatively less.
Difference between precision winding and non-precision
winding :
Two flanged contain both side of the package &
yarns are wound parallel. In this process there is no
necessity of traversing.
Parallel Winding :
9
Advantages :
 Many yarns can be wound at a
time.
 No need of traversing
mechanism.
 Side withdrawal is possible.
 The density of yarn is more.
 No change of number of turns
per inch.
Disadvantages:
 Two sides of the package
need flanged.
 For yarn unwinding, need
separate mechanism.
 Can not be over withdrawal.
Advantages & Disadvantages of Parallel Wound
Package
10
Near parallel winding
:
11
This package contains only one yarn & yarn is
wound near parallel. Layers contain
continuously inner side of the package.
Advantages & Disadvantages of Near Parallel
Wound Package
Advantages:
 No need of flanged
 Can be side withdrawal.
 No change of number of yarn
turns per inch during winding.
Disadvantages:
 Need of traversing
mechanism.
 Can not be side withdrawal.
12
Cross wound
package:
13
This is wound crossly by
single yarn.
Advantages: Disadvantages:
 No need of flange . Can not
be side with drawl.
 Can be over withdrawal.
 Yarn package is stable.
 Number of yarn turns per inch
is changed in this method.
 Quality of yarn is less.
 Need of traversing
mechanism.
Various types of tension device
(According to working principle) :
14
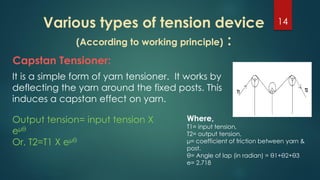
It is a simple form of yarn tensioner. It works by
deflecting the yarn around the fixed posts. This
induces a capstan effect on yarn.
Capstan Tensioner:
Output tension= input tension X
eµθ
Or, T2=T1 X eµθ
Where,
T1= input tension,
T2= output tension,
μ= coefficient of friction between yarn &
post.
θ= Angle of lap (in radian) = θ1+θ2+θ3
e= 2.718
Additive
Tensioner:
15
In this device a dead load or spring is used
to give a fixed increment of tension. The
yarn is passed through middle of the two
surfaces in contact & the force is applied
above to give suitable tension to the yarn.
Here, T2=T1 + 2μF Where,
T1= input tension
T2= output tension
μ= coefficient of friction between yarn &
post F= applied force.
Combined
Tensioner :
16
It is the combined system of capstan
& additive tensioner. The device
permits the tension level to be raised
to any desired extent, but it does not
permit a reduction in tension.
Here, T2=T1eµθ+ T1 + 2μF Where,
T1= input tension,
T2= output tension,
μ= coefficient of friction between yarn &
post.
θ= Angle of lap (in radian) = θ1+θ2+θ3
e= 2.718
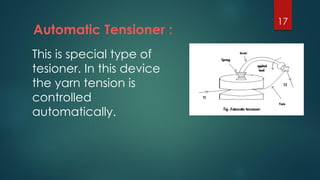
Automatic Tensioner :
This is special type of
tesioner. In this device
the yarn tension is
controlled
automatically.
17
Factor influences for selection of
tensioner :
18
 The device must be reliable to control uniform tension.
 It must be easily threaded.
It must not introduce differences in twist.
 It must not be affected by the presence of oil & dirt.
 It must be easily adjustable.
It must be capable of easy cleaning.
 The operating surfaces must be smooth.
 It must be cheap.
 It must be simple in design & operation.
 It must not damage for yarn.
Depending On the type of the
working member acting on the
yarn : Ball type
 Washer type
 Disc type
 Roller type
 Comb type
 Two zone type
19
Types of Yarn guides: 20
Type- A : Yarn end is required for
threading.
 Takes extra time for threading.
 Yarn passed through the guide
hole.
 Occur more friction with the
yarn.
 No possibility to run out the yarn.
Type- B: Yarn end is not required for threading 21
 Treading is very easy
 Operations time less
 Low cost
 Possibility to run out the yarn
Yarn withdrawal or Unwinding:
22
Unwinding process of yarn from a package is
called withdrawal of yarn.
There are two types of withdrawal:
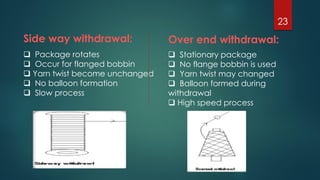
1. Sideway withdrawal.
2. Over end withdrawal.
Side way withdrawal:
 Package rotates
 Occur for flanged bobbin
 Yarn twist become unchanged
 No balloon formation
 Slow process
Over end withdrawal:
 Stationary package
 No flange bobbin is used
 Yarn twist may changed
 Balloon formed during
withdrawal
 High speed process
23
Ballooning: The appearance of the
curved paths of running yarns during
spinning, doubling or winding on or while
they are being withdrawal over-end from
packages under appropriate yarn
winding conditions e.g.; when yarn is
withdrawal through a guide ( often
called balloon eye) placed above and
in the line with the axis of the package at
an adequate distance from it. The yarn
(travelling at sufficient yarn winding
speed) assumes the appearance of a
balloon shape as it is revolves during
withdrawal from a package. This is called
ballooning.
Balloon Theory : 24
WINDING EFFICIENCY : 25
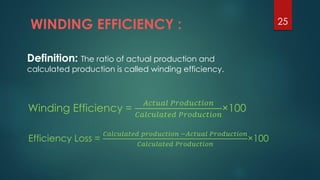
Definition: The ratio of actual production and
calculated production is called winding efficiency.
Winding Efficiency =
𝐴𝑐𝑡𝑢𝑎𝑙 𝑃𝑟𝑜𝑑𝑢𝑐𝑡𝑖𝑜𝑛
𝐶𝑎𝑙𝑐𝑢𝑙𝑎𝑡𝑒𝑑 𝑃𝑟𝑜𝑑𝑢𝑐𝑡𝑖𝑜𝑛
×100
Efficiency Loss =
𝐶𝑎𝑙𝑐𝑢𝑙𝑎𝑡𝑒𝑑 𝑝𝑟𝑜𝑑𝑢𝑐𝑡𝑖𝑜𝑛 −𝐴𝑐𝑡𝑢𝑎𝑙 𝑃𝑟𝑜𝑑𝑢𝑐𝑡𝑖𝑜𝑛
𝐶𝑎𝑙𝑐𝑢𝑙𝑎𝑡𝑒𝑑 𝑃𝑟𝑜𝑑𝑢𝑐𝑡𝑖𝑜𝑛
×100
Winding Faults :
26
 Breakage of yarn
 Soft or Hard package
 Incorrect winging
speed
 Twist variation
 Tension variation
 Dirty package
 Oil or grease package
 Hairiness package
 Poor unwinding
 Slack Knot
 Overlapping