By Robel L.
Department of Textile Technology
Winding Process
2
Winding
 Winding is the process of transferring yarn or thread from one
type of package to another to type of package.
Objectives of winding
(i) To convert a smaller package into a larger package
containing a sufficiently long length of yarn.
(ii) To remove the impurities such as weak places, snarls,
slubs, thick places, etc from the yarn.
3
Technical Requirements of Winding Process
 The physical and mechanical properties of the yarn should not be
impaired.
 Package should be built to ensure easy running off during warping
at high speed.
 The package should contain maximum length of yarn.
4
Cont.…
The yarn ends should be tied with strong knots of correct
structure easily passing at subsequent processing.
The process should remove the objectionable fault.
Yarn wastes must be as small as possible.
The yarn tension should be regular and ensure constant winding
condition
Based on the operation of the machine and the equipment
flexibility, winding machines can be classified as
(i) Non automatic winder
(ii) Automatic winder
6
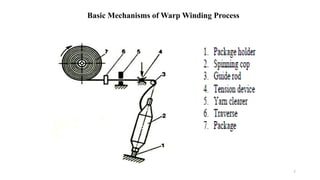
Basic Mechanisms of Warp Winding Process
7
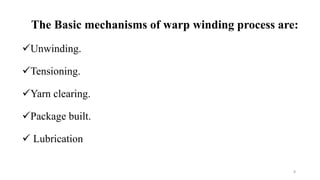
The Basic mechanisms of warp winding process are:
Unwinding.
Tensioning.
Yarn clearing.
Package built.
 Lubrication
8
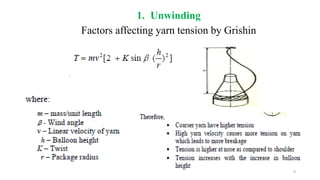
1. Unwinding
Factors affecting yarn tension by Grishin
9
 As the yarn is unwound from the package at high speed, centrifugal force causes it to
follow a curved path(ballooning).
 If balloon size increases tension on the yarn will increase and it will create contact with
the m/c parts, this leads to yarn breakage.
 Therefore, unwinding accelerator (anti-balloon device) should be used.
 The anti-balloon device decreases the tension by having more number of loops. So we
can go for high unwinding speed.
 When 75% of the package unwinds from the spinning cop, tension of yarn will be
increased considerably.
10
2. Tensioning
 The needs for tensioning are:
It gives required winding density.
It gives suitable tension to the yarn.
 It facilitates winding.
It aids to remove weak yarns
11
Cntd…
Tensioning devises can be classified in to four groups:
(I) Multiplicative type (Post type or Capstan)
(II) Additive type
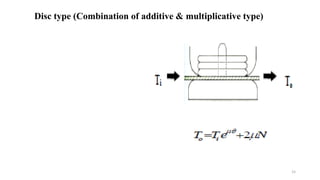
(III) Disc type (Combination of additive & multiplicative type)
(IV) Automatic tensioner
12
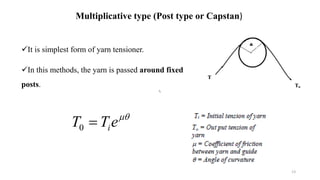
Multiplicative type (Post type or Capstan)
It is simplest form of yarn tensioner.
In this methods, the yarn is passed around fixed
posts.
13
0
T

e
T
T i

0
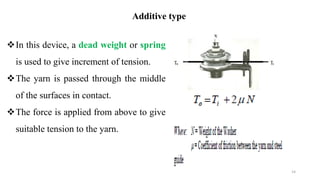
Additive type
In this device, a dead weight or spring
is used to give increment of tension.
The yarn is passed through the middle
of the surfaces in contact.
The force is applied from above to give
suitable tension to the yarn.
14
Disc type (Combination of additive & multiplicative type)
15
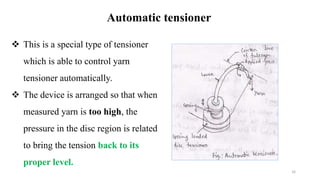
Automatic tensioner
 This is a special type of tensioner
which is able to control yarn
tensioner automatically.
 The device is arranged so that when
measured yarn is too high, the
pressure in the disc region is related
to bring the tension back to its
proper level.
16
3.Yarn Clearing/slub catcher
 Yarn clearer or slub catcher is a device which is used to remove yarn faults in order to
improve yarn quality and weaving efficiency.
Faults removed by yarn clearer:
 Thick & thin places in the yarn.
 Slubs & neps.
 Loose fiber.
 Foreign matters.
17
Type of Yarn clearer
Yarn clearer can be grouped in to:
i. Mechanical clearer
ii. Electromechanical clearer
iii. Electronic clearer
 Capacitance type
 Photoelectric type
18
Cntd…
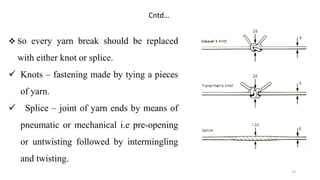
 So every yarn break should be replaced
with either knot or splice.
 Knots – fastening made by tying a pieces
of yarn.
 Splice – joint of yarn ends by means of
pneumatic or mechanical i.e pre-opening
or untwisting followed by intermingling
and twisting.
19
4.Package Formation
 During winding the yarn undergoes two motions.
 It is wound around the package by the package drive and
 It is given a lateral motion to cover the package by the traverse mechanism.
There are two ways to drive the yarn take up package.
1. Spindle winder (by direct drive to the package spindle with constant and variable speed)
 It is important that the yarn be wound under as uniform tension as possible.
2. Drum winder (by surface contact)
20
i. Direct package driving at constant RPM/Speed.
 In this system, the yarn package is placed on a spindle and the
spindle gets motion by motor and gearing system.
So the package gets a constant angular speed and here yarn take up
rate is directly proportional to the package diameter.
In spindle drive winders the tension is unequal throughout the
package ,so a variable speed winder is used.
21
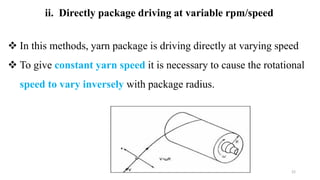
ii. Directly package driving at variable rpm/speed
22
 In this methods, yarn package is driving directly at varying speed
 To give constant yarn speed it is necessary to cause the rotational
speed to vary inversely with package radius.
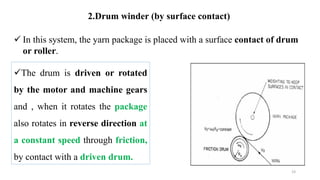
2.Drum winder (by surface contact)
The drum is driven or rotated
by the motor and machine gears
and , when it rotates the package
also rotates in reverse direction at
a constant speed through friction,
by contact with a driven drum.
23
 In this system, the yarn package is placed with a surface contact of drum
or roller.
5. Yarn Lubrication
 Lubricants are used for reduction of friction.
 A lubricant (wax) is applied for knitting yarn and weft yarn
because the level of twist is low.
 In winding of warp yarn, lubricants are not used.
24
Winding defects
If patches are formed on the yarn.
If winding speed is incorrect.
Variation of yarn tension.
If packages are dirty.
Incorrect shape of yarn package.
Too much knots in the yarn.
Excessive full bobbin.
Piecing up.
Over lapping
Two end winding
THANK YOU!