YoucaN
4.4- Formability of sheet metal
YoucaN
Sheet metal formability is generally defined as
the ability of a sheet to undergo the desired shape
change without failure such as necking and
tearing.
Three factors have a major influence on
formability:
1. Properties of the sheet metal as discussed
before
2. Friction and lubrication at various interfaces in
the operation
3. Characteristics of the equipment, tools, and dies
used
Several techniques have been developed to test
the formability of sheet metals, including the
ability to predict formability by modeling the
particular forming operation
1. Cupping test
2. Tension test
3. Bulge test
4. Forming-limit diagrams
Formability of sheet metals
The earliest tests developed to predict formability of sheet
metal were cupping tests, namely, the Erichsen tests
1. In the Erichesn test, a sheet-metal specimen is clamped over a
flat die with a circular opening and a load of 1000 kg
2. A 20 mm diameter steel ball is then hydraulically pressed into the
sheet until a crack appears on the specimen
3. The distance d, in mm, is the Erichsen number
Erichsen test
The greater the value of d the greater is the formability
d = Erichsen number
Because the stretching under the ball is
axisymmetric, they do not at all simulate
the exact conditions of actual forming
operations
YoucaN
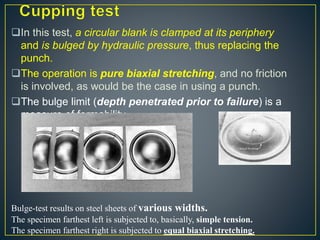
In this test, a circular blank is clamped at its periphery
and is bulged by hydraulic pressure, thus replacing the
punch.
The operation is pure biaxial stretching, and no friction
is involved, as would be the case in using a punch.
The bulge limit (depth penetrated prior to failure) is a
measure of formability
Bulge-test results on steel sheets of various widths.
The specimen farthest left is subjected to, basically, simple tension.
The specimen farthest right is subjected to equal biaxial stretching.
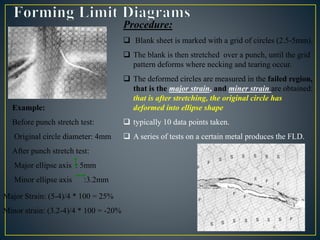
Procedure:
 Blank sheet is marked with a grid of circles (2.5-5mm).
 The blank is then stretched over a punch, until the grid
pattern deforms where necking and tearing occur.
 The deformed circles are measured in the failed region,
that is the major strain, and miner strain are obtained:
that is after stretching, the original circle has
deformed into ellipse shape
 typically 10 data points taken.
 A series of tests on a certain metal produces the FLD.
Major Strain: (5-4)/4 * 100 = 25%
Minor strain: (3.2-4)/4 * 100 = -20%
Example:
Before punch stretch test:
Original circle diameter: 4mm
After punch stretch test:
Major ellipse axis : 5mm
Minor ellipse axis :3.2mm
• During stretching in shee
metal, volume is constant
l + w + t = 0
• Major strain always large
than minor strain
If the surface area of ellipse after stretching is larger than the original circle, we know
the thickness of the sheet has changed, its thinner due to stretching.
Although the major strain is always positive (because forming sheet metal takes
place by stretching in at least one direction), the minor strain may be either
positive [strain occur in the transvers direction greater than the original] or
negative or shrinking [strain occur in the transvers direction smaller than the
original] or zero [ No strain occur in the transvers direction ]in the transverse
direction
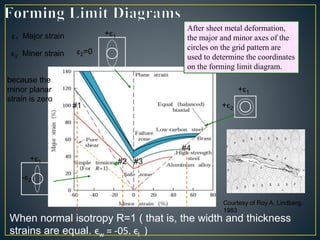
#1
+ε1
-ε2
+ε1
+ε2
+ε1
ε2=0
#3
#4
#2
Courtesy of Roy A. Lindberg,
1983
After sheet metal deformation,
the major and minor axes of the
circles on the grid pattern are
used to determine the coordinates
on the forming limit diagram.
ε1 Major strain
ε2 Miner strain
because the
minor planar
strain is zero
When normal isotropy R=1 ( that is, the width and thickness
strains are equal. ϵw = -05. ϵl )
The most basic and common test used to evaluate formability.
It determines important properties of the sheet metal such as:
- total elongation of the sheet specimen at fracture.
- strain hardening exponent, n.
- the normal anisotropy (R) and
-the planar anisotropy (delta R).
YoucaN
YoucaN
YoucaN
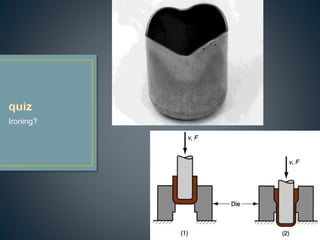
Ironing?
If the thickness of the sheet as it enters the die cavity is more
than the clearance between the punch and die, it has to be
reduced by a deformation called ironing.
By controlling the clearance, C, ironing produce a cup with a
constant wall thickness.
Because of the volume constancy, an ironed cup will be
longer than a cup produced with a large clearance.
Thus, ironing can correct earing that occurs in deep drawing.
Ironing
Ironing to achieve a more uniform wall thickness in a drawn cylindrical cup.
YoucaN
YoucaN