# Quality Control in the Pharmaceutical Industry
## Introduction
Quality Control (QC) is one of the most important components of the pharmaceutical industry because the quality, safety, efficacy, and consistency of medicines directly influence patient health. Pharmaceutical products are expected to meet predetermined standards throughout their lifecycle, beginning with raw materials and continuing through manufacturing, packaging, storage, distribution, and, in many cases, post-marketing surveillance. Quality Control provides a systematic scientific approach for testing, evaluating, and confirming that pharmaceutical materials and finished products comply with established specifications.
The pharmaceutical industry operates under highly regulated conditions because even a small variation in the composition, strength, purity, stability, or performance of a medicine can have serious consequences. Therefore, pharmaceutical companies establish comprehensive Quality Control systems supported by validated analytical methods, qualified equipment, trained personnel, documented procedures, and appropriate regulatory standards.
Quality Control should not be considered only as laboratory testing of finished products. It is an integrated system involving sampling, testing, documentation, investigation of deviations, evaluation of analytical results, environmental monitoring, stability studies, and release or rejection of materials and products. The ultimate objective of QC is to ensure that every pharmaceutical product released to the market is safe, effective, pure, and of consistent quality.
## 1. Meaning and Importance of Quality Control
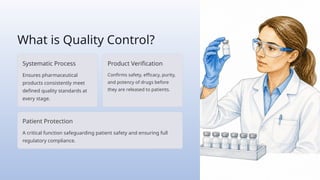
Quality Control refers to the operational techniques and activities used to fulfill specified quality requirements. In pharmaceutical manufacturing, QC involves laboratory and related activities that determine whether raw materials, in-process materials, packaging materials, and finished products meet predefined specifications.
The importance of Quality Control can be understood from several perspectives. First, it protects patients from poor-quality medicines. A product containing an incorrect quantity of active pharmaceutical ingredient (API), unacceptable impurities, microbial contamination, or inappropriate physical characteristics may result in therapeutic failure or adverse effects.
Second, QC ensures batch-to-batch consistency. Pharmaceutical manufacturers produce medicines in large quantities, and every batch should demonstrate comparable quality characteristics. Analytical testing helps verify that manufacturing processes consistently produce products within approved specifications.
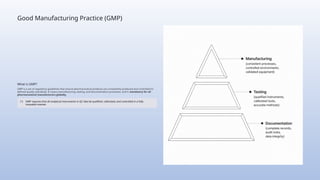
Third, Quality Control supports regulatory compliance. Pharmaceutical companies must comply with requirements established by regulatory authorities and recognized standards such as Good Manufacturing Practices (GMP), pharmacopoeial standards, and applicable national and international regulations.
Fourth, effective QC helps p