DCS’s A. R. A. College of Pharmacy Nagaon, Dhule
Lecture On
IP-II (Industrial Pharmacy-II)
Unit1-‘PILOT PLANT SCALE UP TECHNIQUES’
(B-Pharm Vll Semester)
At
DCS’s A R A College of Pharmacy Nagaon Dhule.
Lecture By
Mr. Yogesh S Lohar
(M Pharm. Pharmacology)
DCS’s A. R. A. College of Pharmacy Nagaon, Dhule
Content
1. Introduction
2. General Consideration
3. Significance of Personnel Requirement
4. Significance of Space Requirement
5. Significance of Raw Material
6. Pilot Plant Scale up Consideration for Solids
7. Pilot plant Scale up Consideration for Orals
8. Relevant Documentation
9. SUPAC Guidelines
10.Introduction to Platform Technology
DCS’s A. R. A. College of Pharmacy Nagaon, Dhule
1. Introduction
 “Pilot plant is a small industrial system which is operated to generate the information
about the exact behaviour of system which is use in design of large facilities for large
scale production”.
 Pilot plant are design for learning and are typically more flexible at the expense of
economy.
 “Pharmaceutical industry pilot plant is a part of industry where lab scale formula is
transformed into commercial product by the development of reproducible procedures
for manufacturing”.
DCS’s A. R. A. College of Pharmacy Nagaon, Dhule
1. 1 Objectives of Pilot Plant
 Evaluation and the validation of process and the equipment use in pharmaceutical
pilot plant.
 Identification of the critical feature of the specific process.
 To design the guideline for the production and process control.
 To provide the master manufacturing formula with mandatory instruction for
manufacturing of the procedure essential for pharmaceutical production.
 To avoid, minimize and mitigate the problems were arising during the scale up
procedure.
DCS’s A. R. A. College of Pharmacy Nagaon, Dhule
1.2 Functions of Pilot Plant
 Determination of required physical space and layout
 Raw material availability
 Evaluation, validation and finalization of production process.
 Records and Reports.
 To provide the Data for minimization the problems associated with production.
 To develop and validate the potential procedure which is required for the production of
Product.
 Identification of the critical feature of specific scale up process.
DCS’s A. R. A. College of Pharmacy Nagaon, Dhule
1.3 Application of Pilot Plant
 Used to evaluate the result obtained from the laboratory trials.
 To make the process and product with less error with large correctness.
 Used to test and verify as well as validate the new technology with less errors.
 The knowledge is helpful for application in full scale production and manufacturing
of pharmaceuticals.
 Also highlights the further research objectives.
DCS’s A. R. A. College of Pharmacy Nagaon, Dhule
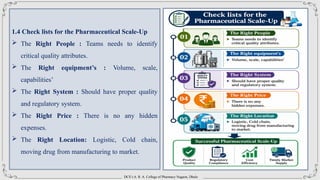
1.4 Check lists for the Pharmaceutical Scale-Up
 The Right People : Teams needs to identify
critical quality attributes.
 The Right equipment’s : Volume, scale,
capabilities’
 The Right System : Should have proper quality
and regulatory system.
 The Right Price : There is no any hidden
expenses.
 The Right Location: Logistic, Cold chain,
moving drug from manufacturing to market.
DCS’s A. R. A. College of Pharmacy Nagaon, Dhule
2. General Consideration of Pilot Plant
 Pilot Plant must have a section for new product and for already existing drug.
 Always follow the procedure which is same for commercial size manufacturing of
Pharmaceuticals products.
 During pilot plant always use formula which determine the ability for large scale.
 The consideration of pilot plant for example Tablets, it mainly enlisted followingly,
most importantly the consideration is depend on the goal of scale up study.
 Granulations feed rate
 Compression parameters
 Temperature control
 Rate of drying
DCS’s A. R. A. College of Pharmacy Nagaon, Dhule
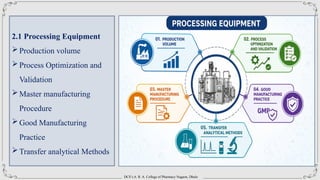
2.1 Processing Equipment
Production volume
Process Optimization and
Validation
Master manufacturing
Procedure
Good Manufacturing
Practice
Transfer analytical Methods
DCS’s A. R. A. College of Pharmacy Nagaon, Dhule
3. Significance of Personnel Requirements
Team must have personnel with scientists having well experience.
To have knowledge about physicochemical properties of materials use for pilot plant scale
up.
Have good theoretical knowledge about preformulation and different formulation.
Personnel are most preferable because they are capable for understanding the objectives.
All personnel are employed in pilot plant scale up should have required qualification for
specific position.
Blending with good theoretical knowledge parallelly with good pharmacy and
pharmaceutical engineering and pharmaceutical industries.
DCS’s A. R. A. College of Pharmacy Nagaon, Dhule
4. Significance of Space Requirement
 Pilot Plant must have a
Administrative and Information Processing
 There should be adequate office and desk space
for scientist, formulations and documentation.
 This space is near by the actual space area.
A. Physical Testing Area
 Should be adequate working area for IPQC
 Analysis helps in early identification of
production or any other type of error.
 Area provide the bench top space for routine
use testing parameter Example: Weighing
balance, pH meter, viscometer etc.
B. Equipment Floor Space
 In this space all the required equipment are
installed,
 For this the arrangement must be make sure that
quality of scale up data collected is prudent with
expensive material.
C. Storage Area
 There should be the separate provision for the
storage of drugs and other materials like
excipients.
 Also the separate are fir the experimental scale-
up batch materials and other finished bulk
DCS’s A. R. A. College of Pharmacy Nagaon, Dhule
5. Significance of Raw Material
 Material used in the processing of pilot plant should not be taken for granted.
 All excipients and raw material were use in pilot plant have well approved and validated.
 Ther drug used at laboratory scale need to meet the rising requirement of the product during the
higher scale production.
 Various differences in the properties of material like particle size, shape or morphology, that may
result in difference in density, rate of solubility and flow properties as batch size is enlarge.
 Sometime a single supplier are create the problems with respect to price and quality of material
would be supplied.
 During the pilot manufacturing several batches of product are to be produced with another
alternative materials this happed with change in price and quality.
DCS’s A. R. A. College of Pharmacy Nagaon, Dhule
6. PILOT PLANT SCALE UP CONSIDERATION FOR SOLIDS
1. Laboratory Scale Up
 Role of Formulation scientist in formulation development
 Upgradation of levels from small scale to large commercial scale
 Main purpose is to assure data, information and findings.
 Normally the batch size for lab scale with 1 to 5 Kg and 10 to 100 kg batch size for pilot plant scale up.
Pharmaceutical process involve in solid dosage form manufacturing
1. Granular product
 By dry granulation and wet granulation
 Use various series of equipment
DCS’s A. R. A. College of Pharmacy Nagaon, Dhule
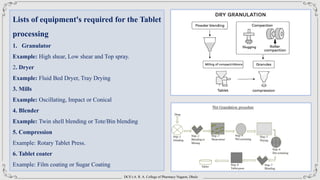
Lists of equipment's required for the Tablet
processing
1. Granulator
Example: High shear, Low shear and Top spray.
2. Dryer
Example: Fluid Bed Dryer, Tray Drying
3. Mills
Example: Oscillating, Impact or Conical
4. Blender
Example: Twin shell blending or Tote/Bin blending
5. Compression
Example: Rotary Tablet Press.
6. Tablet coater
Example: Film coating or Sugar Coating
DCS’s A. R. A. College of Pharmacy Nagaon, Dhule
Directly compressed
For directly compressed tablet products, a typical
equipment were use and they are enlisted below
 1. Blender
Example: Twin Shell Blending, Bin Blending and
Ribbon Blending etc.
 2. Compression
Example: Rotary tablet Press,
 3. Tablet coater
Example: Film and Sugar Coating,
DCS’s A. R. A. College of Pharmacy Nagaon, Dhule
1. High Shear Granulator
Example: Granulator size, Number and Arrangement
of Blade.
2. Tray Dryer
Example: Dryer size, Volume of Air, Number size.
3. Fluid bed dryer
Example: Granule bed height, Volume of air
4. Size Reduction
Example: Type of mill and mechanism involved in it.
5. Blending
Example: Blender capacity, shape and its
configuration
6. Tablet Compression
Example : type of feeder its mechanism, turret
speed and dwell time.
7. Tablet Coating
Example: Type of spray nozzle, atomizer and
spray setting.
8. Additional Facilities: Air conditioning,
humidity control and type of material transfer.
DCS’s A. R. A. College of Pharmacy Nagaon, Dhule
Manufacturing Equipment Attributes/credits or features
 Always preferred to use equipment of similar design at both lab scale and pilot scale.
 In some cases to run the large scale production the similar equipment are not available example,
vacuum foam dryer for processing thermolabile drugs.
 It is always advice that, existing use equipment always familiar with cGMP (Current Good
Manufacturing Practice).
 Always known fact that the pilot batch approximately 1/10th
of scale use for commercial
manufacturing.
 Complex process and lengthy processing time reduces the operational efficiency of plants.
DCS’s A. R. A. College of Pharmacy Nagaon, Dhule
Availability of Raw material
 NCE’s New Chemical Entity
 Its Depends upon NCE’s only few hundreds of
grams or a few kilograms of materials are
available for use.
 Well established raw material is relatively cheaper
when compare to NCE’s.
DCS’s A. R. A. College of Pharmacy Nagaon, Dhule
Granulation
 Process engineers make necessary alteration.
 Changes in amount of granulating fluid
required.
 Due to manufacturing efficiency of equipment
the granulation flid at lab scale required more
fluid then commercial scale.
 Some formulations required more granulating
fluid at lower scale to achieve a desired
granulation.
Drying
 It is critical operation in tablet manufacturing
process where in significant changes may
observed.
 It primarily depends upon dryer capacity,
handle amount and air volume.
 Volume of air flow has the most impact on the
process.
 Seasonal variations
 Tray dryer
DCS’s A. R. A. College of Pharmacy Nagaon, Dhule
Milling
 Size reduction significantly affect the scale-up
process.
 Wide variety of mills were employed to reduce
the size of material
 Different attrition rated generates different result.
 Screen size
 Mill speed
 Milling efficiency
 Some mills imparts more attrition at higher mill
speed.
 Important to match and validate the mill type,
screen size and mill speed.
Blending
 V-blender is commonly preferred
 Blending time
 Size of Blender
 Blending efficiency
 Blend sample 1-3
DCS’s A. R. A. College of Pharmacy Nagaon, Dhule
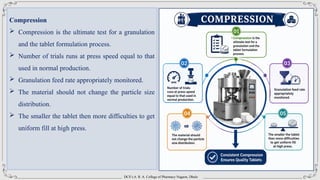
Compression
 Compression is the ultimate test for a granulation
and the tablet formulation process.
 Number of trials runs at press speed equal to that
used in normal production.
 Granulation feed rate appropriately monitored.
 The material should not change the particle size
distribution.
 The smaller the tablet then more difficulties to get
uniform fill at high press.
DCS’s A. R. A. College of Pharmacy Nagaon, Dhule
General Scale Up Consideration
a) Solutions
b) Suspensions
c) Emulsions
Process Variations
Mixing
Mass Transfer
 Power law approach
 Dimensionless number method
 Scale of Agitation Approach
Heat Transfer
Particle size reduction
Principles of similarity
 Geometrical Similarity
 Mechanical Similarity
 Thermal Similarity
 Chemical similarity
Scale Up Liquid Orals
Modular Scale up
Improving Scalability
7. PILOT PLANT SCALE UP CONSIDERATION FOR LIQUIDS-ORALS
DCS’s A. R. A. College of Pharmacy Nagaon, Dhule
Solutions
 Parameters like Tank Size
 Impeller and its diameter
 Speed Numbers, mixing capabilities.
 Number of baffles
 Clearance between bafflers and tank walls.
 Protection of drug using buffers, antioxidants,
and preservatives.
 Using appropriate colouring agent, Stabilizers,
and anti-microbial preservatives.
 Taste and smell masking.
Suspensions
 Parameters like additions and dispersion of
suspending agent.
 Lab scale sprinkling method are use and at
large scale vibration feed system were
employed.
 Suspending agent, time, temperature.
 Selection of equipment as per batch size.
 High mixing speed may leads to air
entrapment.
DCS’s A. R. A. College of Pharmacy Nagaon, Dhule
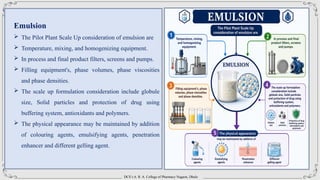
Emulsion
 The Pilot Plant Scale Up consideration of emulsion are
 Temperature, mixing, and homogenizing equipment.
 In process and final product filters, screens and pumps.
 Filling equipment's, phase volumes, phase viscosities
and phase densities.
 The scale up formulation consideration include globule
size, Solid particles and protection of drug using
buffering system, antioxidants and polymers.
 The physical appearance may be maintained by addition
of colouring agents, emulsifying agents, penetration
enhancer and different gelling agent.
DCS’s A. R. A. College of Pharmacy Nagaon, Dhule
Process variation
1. Geometrical similarity of equipment's: The
scale up becomes successful when the
equipment's are same at each manufacturing
scale.
2. Geometric similar means the shape and
dimensions are same.
3. Scalability of equipment's: Manufacturer
describes about scalability of equipment’s
4. It does not ensure the mechanical thermal and
chemical similarity of scaled system.
5. Process are depends on volume, area and
length.
6. Area dependent process: Such as heat transfer,
particle dispersion are area dependant process.
7. Volume dependent process: Such as water
coalescence in an emulsion.
DCS’s A. R. A. College of Pharmacy Nagaon, Dhule
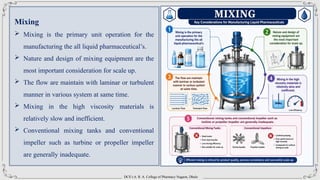
Mixing
 Mixing is the primary unit operation for the
manufacturing the all liquid pharmaceutical’s.
 Nature and design of mixing equipment are the
most important consideration for scale up.
 The flow are maintain with laminar or turbulent
manner in various system at same time.
 Mixing in the high viscosity materials is
relatively slow and inefficient.
 Conventional mixing tanks and conventional
impeller such as turbine or propeller impeller
are generally inadequate.
DCS’s A. R. A. College of Pharmacy Nagaon, Dhule
Mass Transfer
 Gorsky had proposed following three methods for scale-ups liquids
A) Power law Approach
 Non-Newtonian materials can be characterized by power law function.
 It involves in geometrical similarity.
B) Dimensionless Number method
Such as Reynold’s number or Froud number
C) Scale of Agitation Approach
 This approach facilitate scale up under condition of geometric similarity
DCS’s A. R. A. College of Pharmacy Nagaon, Dhule
Heat Transfer
The heat transfer at lab scale occurs
rapidly because volume of surface are
ratio is relatively small.
In the pilot plant and production scale the
heating and cooling of formulation
components take finite time.
Example, Jacketed vessels and immersion
heaters and cooling units becomes
necessity.
Particle Size Reduction
Suspension and emulsion often required
the particle size reduction.
To prevent the agglomerate the suspended
particles.
Milling can disrupt the agglomerates and
make the suspension more homogenous.
In emulsion the dispersion of one liquid
as a droplet in another liquid can be
expressed in a Weber Number
DCS’s A. R. A. College of Pharmacy Nagaon, Dhule
8. Relevant Documentation
 Adequate records and reporting arrangement are essential component in scale up.
 Are integral part of smooth transfer of product from bench scale to pilot scale.
Forms of Documentations
 Various nature of forms are generated during the scale-up operation.
 At earlier times it may in the form of hard copy reports.
 Todays due to advancement of technologies the previous hard copy are replace with soft copy.
 It should be provide it the well organize way of sharing of knowledge
Types of Document
There are two types of Documents
a. Permanent Document and
b. Temporary Document
DCS’s A. R. A. College of Pharmacy Nagaon, Dhule
Structure and Circulation of Documents
 Orderly, documentation with proper indexing
required for scale up.
 Whenever possible categorise the documents
into various units and topic wise.
 Main advantages are the store information can
be review, finalize and approve without any
waiting.
 The categorization will helps to the team
member only to deal with the content that is
relevant to them.
 The main aim is to restrict and minimize the
documentation from most complex one.
Document at Start of Scale up
 Document shall be simple to get easy tracked.
 Various Document management toolset were use for
big scale up.
 There are various documents managements system
were available includes catalogue of all control
documents.
 Example, Description, purpose, objective form and
format, responsibilities and right for review.
 Usually the permanent document need to be updated
if something changes after it has been finalized.
 Where temporary documents may be left as only
historic record an they have not important if project
were completed once.
DCS’s A. R. A. College of Pharmacy Nagaon, Dhule
Document Tracking Progress and Status
 There are certain documents to trach the progress and status
of subject.
 It includes planned Date of Completion, current status and
effective date.
 The lists if projects team members.
 The team members have responsibility to store and issue the
template version of each documents.
 The authorise team member check and provides the update
of appropriate documents.
 To provide the search access and view access to information
are important issue with related to project progress.
 Lastly the document flow should be maintained analysed
and updated with the progress of project.
Document During the Project
 Project manager and relevant project office tracks the
documents status.
 They look which documents are in initial stage and
which one at final stage.
 The documents are made to easy, and efficient as
possible for audit.
DCS’s A. R. A. College of Pharmacy Nagaon, Dhule
9. SUPAC (Scale Up And Post Approval Changes)
Guidelines introduction part
 The laboratory scale batches used in clinical trials were
expands to pilot scale and finally to commercial scale
production.
 The 1991-92 Workshop held by AAPS-USFDA and
USP it explore principles related to compositional
changes in drug product post approval.
 It includes process changes, process scale changes and
process site or campus changes.
 This workshop proceeding are published as a guidance
by the USFDA with title “ SUPAC- Scale-Up and Post
Approval Changes”.
 In 30 November 1995 SUPAC Guidance for
Immediate Release Product was Published.
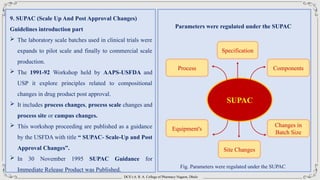
Parameters were regulated under the SUPAC
SUPAC
Specification
Components
Changes in
Batch Size
Site Changes
Equipment's
Process
Fig. Parameters were regulated under the SUPAC
DCS’s A. R. A. College of Pharmacy Nagaon, Dhule
1. Site Changes
New manufacturing equipment's location should have
a satisfactory cGMP inspection.
Level 1
a. Test Documentation
b. Filing Documentation
Level 2
c. Test Documentation
d. Filing Documentation
Level 3
e. Test Documentation
f. Filing Documentation
2. Changes in Batch Size (Scale-up/scale-Down)
 Change from the batch size from scale-up to large
production after NDA or ANDA require
submission of additional information.
 All changes should be properly validated.
 USFDA has divided scale-up into two levels.
Level-1
 10 times the size of pilot scale.
 Same design and Principles are required.
Level-2
 Beyond the factor of 10 time from pilot scale.
 Requirement are same as level 1.
DCS’s A. R. A. College of Pharmacy Nagaon, Dhule
3. Manufacturing Changes
A) Equipment
Level-1
a. Definition of Changes
b. Test Documentation
c. Filling Documentation : Annual Report
Level-2
a. Definition of Level
b. Test documentation
Filing Documentation: Annual Report
B) Process
Level-1
Level-2
Level-3
4. In Vitro Dissolution Data
 Are given in current United state Pharmacopeia/
National Formulary (USPNF) section 711.

DCS’s A. R. A. College of Pharmacy Nagaon, Dhule
5. In-Vivo Bioequivalence studies
a. Objectives
b. Design
c. Selection of Subject
d. Procedure
e. Restrictions
f. Blood sampling
g. Analytical methods
h. Pharmacokinetic analysis
a. Objectives
To compare the rate and extent of absorption of the drug from
product for which the manufacture has been changed.
b. Design
It should be single dose, two-treatment, two period cross over etc.
c. Selection of Subject: The subject should be determined
statistically to account intra-subject variability.
d. Procedure:
Treatment dose administered followed by overnight fast at least 10
hours,
e. Restriction
Water were allow for some one desire (ad libitum) except 1 hour
before and after of treatment.
DCS’s A. R. A. College of Pharmacy Nagaon, Dhule
10. INTRODUCTION TO PLATFORM
TECHNOLOGY
1. Nanotechnology
2. Microsphere Technology
3. Liposomal Technology
4. Hot Melt Extrusion Technology
5. Sustained release Formulation technology
6. Multiple-Unit Pallet System Technology
7. Orally Disintegrating Formulation Technology
8. Inhalation Technology
 Metered dose Inhalers
 Dry powder inhaler
 Auto haler
 Nasal Sprays
 Orally Disintegrating Tablet Technology
 Effervescent Technology
 Sprinklers
 Stem Cell Based Products
 Magnetic Targeted carriers
DCS’s A. R. A. College of Pharmacy Nagaon, Dhule