PILOTPLANTANDSCALEUP
TECHNIQUES
Shubham D Ghodke
 CONTENTS
 Definition
 Significance
 General Consideration
 GMP Considerations
 Product Considerations
 Advantages
 Disadvantages
DEFINITIONS
 Plant:- It is a place where the 3 M's that are Man, Material and
Money are brought together for the manufacturing of products.
 Pilot Plant:- It is the part of the pharmaceutical industry where
a lab scale formula is transformed into a viable product by
development of liable practical procedure of manufacturing.
 Scale-up:- The art for designing of prototype usingthe data
obtained from the pilot plant model.
 SIGNIFICANCE
 Permits close examination of formulae to determine its ability to withstand
batch scale and process modification.
 Review of Equipment - most compatible with theformulation & most
economical, simple and reliable in producing product
 .Raw materials - consistently meet the specifications required to produce
the product can be determined.
 Production rate adjustment after considering marketing requirements.
 Give rough idea about physical space required and of related functions.
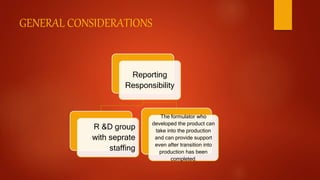
GENERAL CONSIDERATIONS
Reporting
Responsibility
R &D group
with seprate
staffing
The formulator who
developed the product can
take into the production
and can provide support
even after transition into
production has been
completed.
2. Personnel Requirements
 Scientists with experience in pilot plant operations as well as
in actual production area are the most preferable
 .*As they have to understand the intent of the formulator as
well as understand the perspective ofthe production
personnel.
 Engineering principles
 Knowledge of computers & electronics
Standard Pilot-plant Equipment Floor Space :-
 Discreet pilot plant space, where the equipment needed for manufacturing
all types of dosage form is located.
 Intermediate-sized and full scale production equipment is essential in
evaluating the effects ofscale-up of research formulations and processes.
 Equipments used should be made portable where ever possible. So that
after use it can be stored in the small store room.
Raw materials
 One purpose/responsibility of the pilot-plant is the approval & validation of
the active ingredient & excipients raw materials.
 Raw materials used in the small scale production cannot necessarily be
the representative for the large scale production.
 Ingredients may change in particle size, shape or morphology which result
in differences in bulk density, static charges, rate of solubility, flow
properties, color, etc.
Equipment
 The most economical, simplest & efficient equipment which are capable of
producing product within the proposed specifications are used.
 The size of the equipment should be such that the experimental trials run
should be relevant to the production sized batches.
 If too small the process developed will not scale up.
 If too big then the wastage of the expensive active ingredients.
 Ease of cleaning
 Time of cleaning
Production Rates:-
 The immediate as well as the future market trends/requirements are
considered while determining the production rates.
GMP CONSIDERATIONE
 equipment qualification
 Process validation
 Regularly process review & revalidation
 Relevant written standard operating procedures
 The use of competent technically qualifiedpersonnel
 Adequate provision for training of personnel
 A well-defined technology transfer system
 Validated cleaning procedures
 An orderly arrangement of equipment
ADVANTAGES
 Members of the production and quality control divisions can readily
observe scale up runs.
 Supplies of excipients & drugs, cleared by the quality control division, can
be drawn from the more spacious areas provided to the production
division.
 Access to engineering department personnel is provided for equipment
installation, maintenance and repair.
DISADVANTAGES
 The frequency of direct interaction of the formulator with the production
personnel in the manufacturing area will be reduced.
 Any problem in manufacturing will be directed towards it's own pilot-plant
personnel.
PRODUCT CONSIDERATIONSSOLID DOSAGE FORM
 Soliddosageform
 Material Handling
 Laboratory Scale
 Deliver accurate amount to the destination
 Large Scale*
1. Lifting drums
2. More Sophisticated Methods-
 Vacuum Loading System
 -Metering Pumps
 Prevent Cross Contamination by
 Validation Cleaning Procedures.
2. Dry Blending
 Powders should be used for encapsulation or to be
 granulated prior to tabletting must be well blend
 ensure good drug distribution.
 Inadequate blending could result in drug content
 uniformity variation, especially when the tablet or capsule
 is small & the drug concentration is relatively low.
 Ingredients should be lumps free, otherwise it could cause
 flow problems.
3. GranulationsReasons :-
 To improve the flow properties.
 To increase the apparent density of the powder.
 To change the particle size distribution so that the
 binding properties on compaction can be improved.
 Types:
a) Wet Granulation
b) Dry Granulation
c) Direct Compression Method
 A small amount potent active ingredient can be dispersed
 most effectively in a carrier granulation, when the drug is
 dissolved in granulating solution and addedduring the
 granulating process.
4. Drying
 Hot air oven
1. air temperature
2. rate of air flow
3. depth of granulation on the trays
 Fluidized Bed Dryer
1. optimum loads
2. rate of airflow
3. inlet air temperature
4. humidity
TABLET COATING
 Equipments :-
1. conventional coating pan
2. perforated pans of fluidized-bed coating column
 Types :-
1. Sugar coating
2. Film coating
 Tablet must be sufficiently hard to withstand the the
 tumbling to which they are subjected while coating.
 Operation conditions to be established for pan or column
 operation are optimum tablet load, operating tablet, bed
 temperature, drying air flow rate, temperature, solution
 application rate.
CAPSULES
 To produce capsules on high-speed equipment, the
 powder blend must have,
 uniform particle size distribution
 bulk density
 formation of compact of the right size and of sufficient
 cohesiveness to be filled into capsule shells.
 Equipments:-
1. Zanasi or Mertalli - Dosator(hollow tube)
2. 2. Hoflinger - Karg - Tamping pins
3. Weight variation problem can be encountered with these two methods
4. .Overly lubricated granules - delaying disintegration.
THANK YOU