Institute of Technology Tallaght
Department of Mechanical Engineering
ProjectTitle: Microstructural & Micro Hardness Analysis of Defective
and Defect Free Multi-pass Welded Coupons
Supervisor - Brian O’Brien
Student name - Joseph Stynes
Student number - X00105837
Date of Submission: 24/04/16
Declaration
I hereby declare that this is my original work produced without the help of any
third party.
Signed:
Date: 24/04/16
Lecturer Feedback
i
Abstract
Multi-pass welds are different in nature to single pass welds, not simply because of the
number of weld passes but because of the effect that repeated thermal cycling has on the final
microstructure. Because the initial weld is not exposed to the cooling ambient air for any
length of time, as would be the case with a single pass weld, its final mechanical properties
are quite different. The initial heat energy required, to raise the material to a point where the
material becomes molten within the weld fusion zone, decreases with successive weld passes.
Once the initial weld pass has been completed then the material temperature has greatly
increased. The re-heating of the previous weld metal deposit by subsequent weld passes acts
to normalise the previous weld microstructure. This ensures that any residual stresses within
the material are reduced.
The nature of multi-pass welds guarantee a level of preheat into the material and, upon
completion of the welding operation, slows the cooling rate down and greatly reduces the
likelihood of the formation of cracks within the welds and the parent material. When the final
weld is completed, whether it is a multi-pass fillet weld or a multi-pass butt weld, its
microstructure differs significantly from the previous welds. This is because the final weld is
exposed to the cool ambient air, unlike the previous welds. This ensures that the final welds
have a different cooling rate than the underlying welds and therefore a higher level of
hardness. By sectioning these multi-pass weld specimens and hot mounting them using a
phenolic resin they are then subject to successive planar grinding and polishing. They are
then finally etched with a 2% nitric acid solution to highlight the grain structure of the
material. This is done to allow for the microscopic examination of the weld microstructure.
Photographic images are taken to further examine the microstructure from the parent metal
through to the heat affected zone and the weldment. This is a crucial step to help clearly
identify any flaws that maybe present. Vickers Micro Hardness tests are then carried out to
determine the hardness values of the different zones of interest.
Acknowledgements
I wish to thank my supervisor Brian O’Brien for his ongoing support and encouragement
throughout this project. I would also like to thank Elaine McGeough for patiently training me
on the use of the metallographic equipment in the materials lab. I am also very thankful for
the knowledge and help given to me by Brian O’Donnchadha on the use of the hardness
testing and microscopy equipment in the metrology lab. Thanks also to Alan Somers for
allowing me access to the manufacturing lab anytime that I needed it. A special thanks
to Chris Keogh for his help with a critical part of this project.
ii
Contents
Institute of Technology Tallaght.............................................................................................1
Chapter 1 Project Introduction..............................................................................................1
1.1 Project proposal & Project description........................................................................1
1.2 Why was the project being undertaken? .....................................................................1
1.3 Aims and Objectives ...................................................................................................1
1.4 Objectives for the Literature review............................................................................2
1.5 Methodology of approach to undertaking of project...................................................2
1.6 The preparation and welding of the selected samples .................................................3
1.7 Material needed for weld coupons ..............................................................................3
1.8 The preparation of the welded samples to be mounted and polished ready for
Microscopic inspection..........................................................................................................4
1.9 The Testing for hardness variation across the welded samples using Vickers Micro
Hardness testing.....................................................................................................................4
Chapter 2 Literature review..................................................................................................5
2.1 Introduction.................................................................................................................5
2.2 Microstructural analysis of steels................................................................................5
2.3 Ferrite ..........................................................................................................................6
2.4 Cementite ....................................................................................................................7
2.5 Pearlite.........................................................................................................................7
2.6 Austenite......................................................................................................................8
2.7 Martensite....................................................................................................................9
2.8 Previous research and analysis of Carbon steel microstructure ................................10
2.9 Welding processes.....................................................................................................10
2.10 Welding procedure.................................................................................................11
2.11 Welding technique .................................................................................................12
2.12 Welding consumable material selection ................................................................12
2.13 Material selection...................................................................................................13
2.14 Heat treatment procedure.......................................................................................13
2.15 Welding of samples ...............................................................................................13
2.16 Mounting of welded samples.................................................................................14
2.17 Grinding and polishing of mounted samples .........................................................14
2.18 Microscopic analysis of weld samples ..................................................................15
2.19 Hardness testing and analysis of weld samples .....................................................15
iii
2.20 A review of research papers into the field of weld microstructures and their
defects and the causes of such defects .................................................................................16
Chapter 3 Preparation of test samples ................................................................................24
3.1 Design of welded coupons ........................................................................................24
3.2 Preparation of MMA welded carbon steel pipe (API 5L).........................................24
3.3 Preparation of TIG welded carbon steel pipe (API 5L) ............................................25
3.4 Preparation of MMA welded mild steel plate ...........................................................25
3.5 Preparation of TIG welded mild steel plate ..............................................................26
3.6 Preparation of MMA and TIG welded medium carbon steel flat (EN 8) .................26
3.7 Preparation of MMA and TIG welded high carbon tool steel flat (O1tool steel) .....27
3.8 Welding procedure for test samples..........................................................................28
3.9 Sectioning of weld samples.......................................................................................31
3.10 Compression mounting of samples........................................................................31
3.11 Planar grinding and polishing of samples..............................................................32
3.12 Table of variables for planar grinding and polishing.............................................33
Chapter 4 Methods of Evaluation of Project Data..............................................................35
4.1 Macroscopic analysis ................................................................................................35
4.2 Microscopic analysis.................................................................................................35
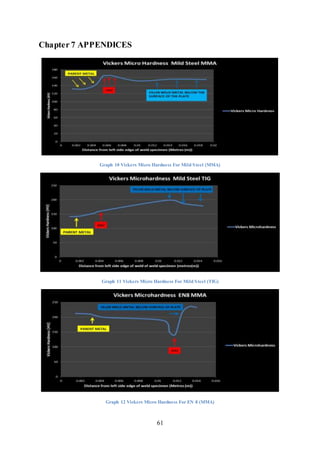
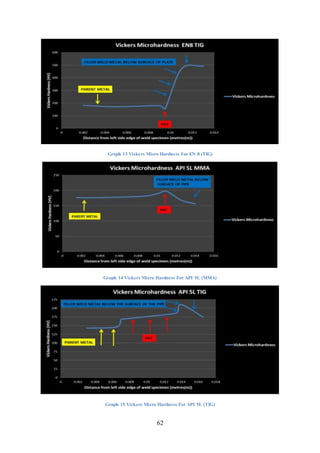
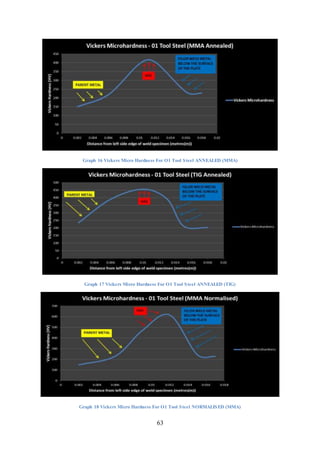
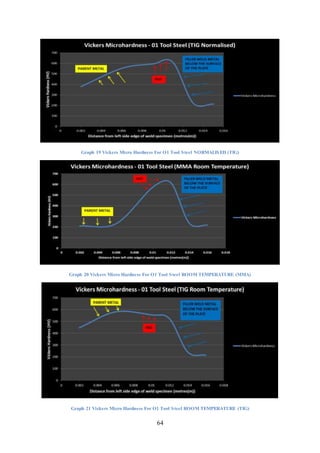
4.3 Micro Hardness testing..............................................................................................35
4.4 Representing the micro hardness results graphically using Microsoft Excel............36
4.5 Sample Table of Results for Vickers Micro Hardness Tests ....................................36
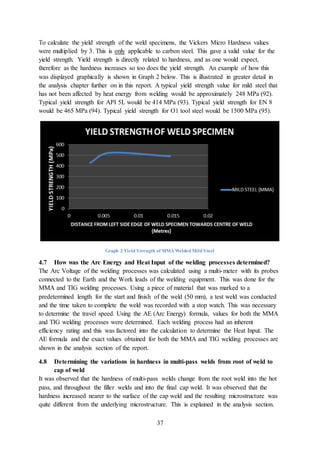
4.6 Determining the Yield Strength of the Weld specimens...........................................36
4.7 How was the Arc Energy and Heat Input of the welding processes determined? ....37
4.8 Determining the variations in hardness in multi-pass welds from root of weld to cap
of weld..................................................................................................................................37
Chapter 5 Analysis of results..............................................................................................38
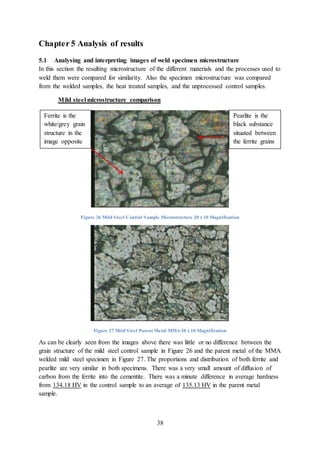
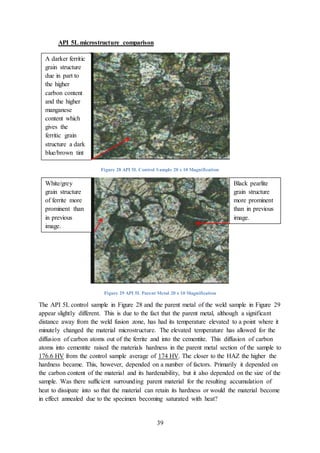
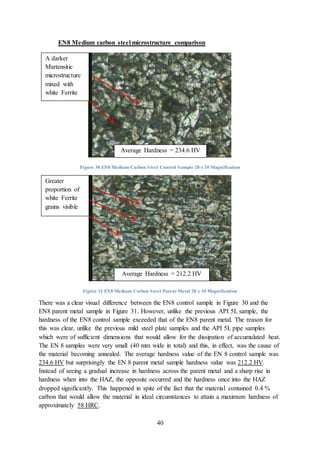
5.1 Analysing and interpreting images of weld specimen microstructure ......................38
5.2 Comparing the HAZ of the four steels......................................................................42
5.3 Analysing & interpreting macroscopic images of defective and defect free weld
specimens.............................................................................................................................43
5.4 Sample graphs of Vickers hardness plots..................................................................47
5.5 The formation and propagation of cracks in welded specimens ...............................48
Chapter 6 Discussion..........................................................................................................49
6.1 Differences in Arc Energy and Heat Input of MMA and TIG..................................49
iv
6.2 The effect of multiple weld passes on the mechanical properties .............................50
6.3 Yield strength of weld specimens .............................................................................51
6.4 Hardenability.............................................................................................................52
6.5 Strengthening by Grain Size Reduction....................................................................54
6.6 Phase Transformations in Weld Specimens..............................................................55
6.7 Heat Treatment of Carbon Steels ..............................................................................56
6.8 Conclusions ...............................................................................................................58
Chapter 7 APPENDICES ...................................................................................................61
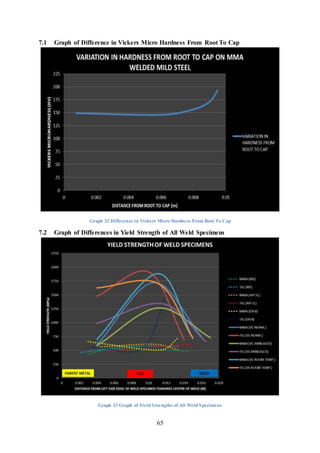
7.1 Graph of Difference in Vickers Micro Hardness From Root To Cap .......................65
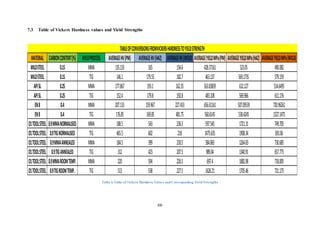
7.2 Graph of Differences in Yield Strength of All Weld Specimens ..............................65
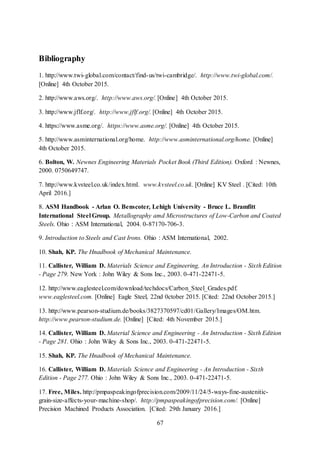
7.3 Table of Vickers Hardness values and Yield Strengths ............................................66
Bibliography.............................................................................................................................67
1
Chapter 1 Project Introduction
1.1 Project proposal & Project description
To investigate the microstructure and micro hardness of defective and defect free welded
coupons using low carbon mild steel, API 5L carbon pipe, medium carbon steel (EN8), and
O1 tool steel utilising two different welding processes, MMA and TIG. The photographic
images taken were compared so as to illustrate the differences in microstructure. Micro
hardness tests were conducted using Vickers micro hardness testing, the results from testing
the different materials were compared graphically on an Excel chart. The Vickers hardness
values were used to determine the yield strength of the materials.
1.2 Why was the project being undertaken?
This project was undertaken to investigate the effect of the heat input of the welding
processes MMA and TIG on the microstructure of low carbon mild steel, API 5L carbon
pipe, and medium carbon steel (EN8) as well as the alloy O1 tool steel. Sound defect free
samples, welded to ASME IX standard, and defective samples created using poor technique
were made. They were subjected to microscopic examination so as to graphically illustrate
and compare the varying effects on the microstructure from heat input during the welding
operation on the different grades of carbon steel and tool steel.
There was a need to conduct various hardness tests on the prepared samples so as to
investigate whether or not there is a change in hardness across the zones of the sample, from
the base metal to the Heat Affected Zone (HAZ) and through to the weldment on all four
steel grades. There was a need to examine the effect of imparting differing levels of heat into
the material.
1.3 Aims and Objectives
The main aims of this project are as follows:
 To investigate and analyse the effects of welding on the microstructure of mild steel,
API 5L carbon pipe, medium carbon steel (EN8), and O1 tool steel. The
microstructure from parent metal to Heat Affected Zone (HAZ) and weldment are to
be identified.
 To analyse, interpret and compare the different structures of the mild steel, API 5L
carbon pipe, medium carbon steel (EN8), and 01 tool steel welded coupons, and
discuss their differences.
 To investigate and compare the effects of heat input caused by utilizing different
welding processes, namely MMA & TIG.
 To identify and explain the causes of any weld defects present. Different weld defects
will occur using different welding processes, this was achieved by intentionally
utilizing poor operator technique.
 To conduct Rockwell hardness and Vickers Micro Hardness tests on mild steel, API
5L carbon pipe, medium carbon steel (EN8), and O1 tool steel welded coupons to
ascertain if the hardness changed across the zones from parent metal to HAZ to
weldment.
2
1.4 Objectives for the Literature review
The main aims of the Literature review
The main aims of the literature review was to review relevant technical literature relating to
the project that was undertaken and that has been published and peer reviewed by experts in
the field of welding technology.
Questions askedand areas that were examined
 What was the effect of welding on the micro structure of mild steel and API 5L,
medium carbon steel and O1 tool steel?
 How was the microstructure of medium carbon steel and O1 tool steel affected by
improper pre-weld and post-weld heat treatment?
 Did the varying levels of heat input from different welding processes have an effect
on the microstructure of the different steels being welded?
 What were the type and nature of the weld defects present in the steels being welded
using both MMA and TIG?
 What difference in hardness values were recorded between mild steel, API
5L,medium carbon steel (EN 8), and O1 tool steel across the different areas of the
welded coupons from the parent metal into the heat affected zone (HAZ) and the
weldment itself ?, did they compare to published results ?
Sources used for the literature review
Sources used include those listed below but also contain many others
 The Welding Institute Cambridge (TWI) (1).
 The American Welding Society (AWS) (2).
 The James F Lincoln Foundation (3)
 The American Society of Mechanical Engineers (ASME) (4)
 The American Society of Materials (ASM) (5)
 The Newnes Engineering Materials Handbook (6).
1.5 Methodology of approach to undertaking of project
Plan of practical work to be undertaken
 Phase one – This phase included the cutting, machining, and welding of a selection of
steels.
 Phase two – This phase encompassed both the sectioning and mounting of the welded
samples as well as the planar grinding and polishing of the samples.
 Phase three – The final phase was the microscopic examination and photographic
imaging of the material microstructures as well as the Vickers micro hardness testing
of welded samples.
3
1.6 The preparation and welding of the selectedsamples
The aim of Phase one of this project was to weld a selection of joints using four different
materials, mild Steel, API 5L carbon pipe, medium carbon steel (EN8), and O1 tool steel that
had been prepared to specific criteria. These criteria were as follows:
 Joint type and Joint configuration
 Joint bevel angle
 Joint root gap dimension
 Joint root face dimension
 Pre-heat and post-heat temperature (where applicable)
The project used a selection of welded coupons that were welded to a defect free standard
(ASME IX 1G, 3G, 6G). Other samples were welded knowingly using an improper technique
to induce defects into the weldments for the purpose of examination. These samples were
welded using two processes, MMA (Manual Metal Arc), and TIG (Tungsten Inert Gas). Once
those materials had been prepared in the correct manner the welding operation was carried
out according to industry standard WPS (Welding Procedure Specification), these standards
and procedures were clearly explained and referenced further in the report. However to
intentionally introduce defects into a selection of samples a number of steps were taken.
These steps included inadequate gas shielding so as to introduce porosity into the weldment,
inadequate amperage and improper welding technique so as to introduce lack of fusion
between the weldment and the base metal. The parameters are clearly laid out in Table 1
below.
1.7 Material needed for weld coupons
Material Mild
steel
plate
Mild
steel
plate
API 5L
seamless
pipe
API 5L
seamless
pipe
Medium
carbon
steel
(EN8)
flat
Medium
carbon
steel
(EN8)
flat
01 Tool
steel flat
01 Tool
steel flat
Joint type Butt Butt Butt Butt Butt Butt Butt Butt
Inclusive
bevel angle
70o 70o 70o 70o 35o 35o 35o 35o
Number of
coupons
2 2 2 2 2 2 2 2
Material
thickness
10 mm 10 mm 9mm
Sch. 80
9mm
Sch. 80
5 mm 5 mm 6 mm 6 mm
Welding
processes
MMA TIG MMA TIG MMA TIG MMA TIG
Welding
consumable
electrode
Oerlikon
E7016/
Lincoln
E7018-1
Oerlikon
ER 70s-2
Oerlikon
E7016/
Lincoln
E7018-1
Oerlikon
ER 70s-2
ESAB
OK 68.81
E312
Stainless
SIF
ER 312
Stainless
ESAB
OK
68.81
E312
Stainless
SIF
ER 312
Stainless
Heat
treatment
None None None None None None Yes
(Specified
later)
Yes
(Specified
later)
Table 1 Materials & Processes and Welding consumables
4
1.8 The preparation of the welded samples to be mounted and polished ready for
Microscopic inspection
The aim of Phase two of the project was to microscopically analyse and interpret the effects
of welding on the micro structure of the test samples then to compare the results. This,
however, was only possible once the welded coupons had been prepared in the proper fashion
by cutting the specimens to the required dimensions and then preparing them for mounting
and polishing using the metallographic grinding & polishing machine, then the microscopic
examination commenced. When conducting the microscopic examination, photographic
images were taken of the weld specimen microstructure.
1.9 The Testing for hardness variation across the welded samples using Vickers Micro
Hardness testing
The aim of Phase three of the project was to conduct hardness tests using the Buehler
Vickers Micro Hardness testing machine. Once the hardness tests had been completed then
photographic images were taken of the hardness test indentations.
How were the test data and results presented?
The photographic images recorded were used to graphically illustrate different zones within
the microstructure and to show the point at which these zones changed from parent metal to
HAZ to weldment and how the grain size changed across those zones. The Vickers hardness
test results were displayed on Excel graphs. The different zones that the values were obtained
from were clearly labelled on graphs to explain how hardness changed across zones.
Analysis of the primary results and test data
The photographic imaging and the Vickers micro hardness test data were analysed to identify
and determine:-
 How the microstructure changed across weld zones
 How hardness changed
 The effects that material composition as well as welding technique had on weld
strength
 The location and cause of weld defects
Analysis of secondary results and test data
 Yield strength of weld specimens – Comparing the yield strength of the welded
specimens to those of raw materials that have not been affected by the heat energy of
welding, and determining if this is a problem for design.
 Arc Energy and Heat Input – Comparing the arc energy and heat input from of the
two welding processes MMA & TIG and determining if there are differences. What
effect would those differences in heat input have on the resulting microstructure?
5
Chapter 2 Literature review
2.1 Introduction
The aim of the literature review
The aim of this chapter was to familiarise the reader with Microstructural & Micro Hardness
analysis of welded coupons of various grades of carbon steel as well as alloyed tool steel. The
literature review included referenced research into the changes in the micro structure and
micro hardness of the materials due to the heat input caused by the welding operation and the
addition of filler materials into the weldment. The review detailed published work to date on
the effects of various welding processes on the microstructure and micro hardness of various
steels as seen in Table 2 below.
Material Mild steel API 5L Grade
B
EN 8 Medium
carbon steel
01 Tool steel
Carbon content 0.10% - 0.15% 0.25% - 0.30% 0.40% - 0.45% 0.90% - 0.95%
Table 2 Material Carbon Content (7)
Typical applications for these materials are as listed below:-
 Mild steel – Probably the most broadly used steel used in general fabrication. Used in
the fabrication of a vast array of things such as roof trusses, fire escapes, gates,
railings etc. etc. Excellent weldability.
 API 5L Grade B – API 5L Grade B seamless carbon steel pipe is used in the
petrochemical industry for the transport of oil and gas. It is also used in the power
generation industry for the transport of steam. Good weldability.
 EN8 Medium carbon steel – This material is used in the fabrication of shafts, pins,
rolls, spindles, gears etc. etc. Good weldability provided precaution is taken to follow
the heat treatment process required.
 01 Tool steel – 01 Tool steel is used in the fabrication of cutting tools such as high
quality combat knives, taps & dies, reamers, intricate forging dies, paper cutting
machine knives. Poor weldability, even if proper heat treatment procedure is
followed. This gives a clearer understanding of the different materials that were used
in this investigation and their common uses & applications within industry.
2.2 Microstructural analysis of steels
Microstructural analysis is the inspection and interpretation of grain structure, including
anomalies and flaws within metallic structures at the microscopic level. The arrangement of
the grain structure can be viewed microscopically to understand the importance of stringent
materials manufacturing processes and welding procedures as well as engineering design in
general. Flaws within a material structure or the welds joining such materials must be
avoided. With varying carbon content present in the different samples, it was shown that the
samples have a varied grain structure when viewed microscopically. In the past,
microstructures of various carbon steels have been examined and although different due to
their varying carbon content and the heat treatment processes they undergo they are still
similar in some ways.
6
They mainly contain five different regions:-
 Ferrite
 Cementite
 Pearlite
 Austenite
 Martensite.
The largest constituent part of low carbon steel would be ferrite. It is crucial to this literature
review and to the project as a whole to understand the nature of these different regions. The
need to identify and interpret these regions within the metallic structure and how they interact
to produce defective structures or sound defect free structures is crucial. The nature of these
structures and how they are formed are discussed and graphically illustrated in the course of
this chapter.
2.3 Ferrite
Ferrite has a BCC (Body Centred Cubic) crystal structure and is, to the greatest part, pure
iron with a negligible carbon content of approximately 0.005%. (8) This however is not
counting the other small alloying elements such as manganese, silicon, and phosphorous,
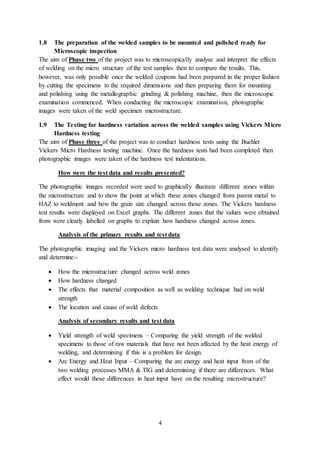
sulphur, and copper. In Figure 3 of the image below, a ferrite grain structure of AISI 1010
steel can be seen. The ferrite grains are the large white patches and the pearlite (containing
layers of ferrite and cementite) are the small black spots interspersed throughout the material.
AISI 1010 is the American designation for the European equivalent of low carbon mild steel
with a carbon content of maximum 0.1 % - 0.13 % carbon. (9)
Figure 1 Ferrite with Pearlite at the grain boundaries (10)
7
2.4 Cementite
Cementite is formed when the amount of carbon present in the steel has exceeded the amount
of carbon that the ferrite has the ability to dissolve within its microstructure below 727o C, the
excess carbon turns into a very hard brittle substance called iron carbide or Fe3C. (11) Iron
Carbide is the component which gives steel its strength, however this is not always
favourable if this exceeds the amount of Fe3C required for desired strength. This is to be
avoided in low carbon steel because it can turn the material hard and brittle. It also drastically
reduces its toughness and ductility, this in turn severely limits the ability of the material to be
cold worked. (8) Cementite when combined with ferrite forms layers or lamellae called
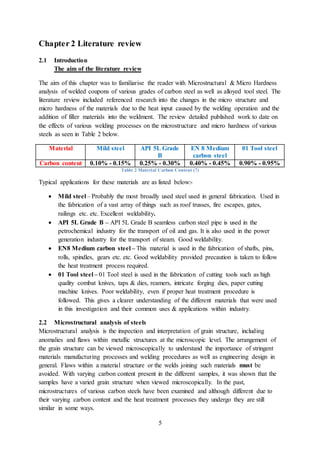
pearlite. In Figure 4 in the image below, a ferritic grain structure of AISI 1018 steel can be
seen with large dark regions which are pearlite containing ferrite and cementite. AISI 1018 is
an American designation of the European equivalent of a type of mild steel with a maximum
carbon content of 0.18 % carbon. (12)
Figure 2 Cementite & Ferrite (pearlite) at the grain boundaries of Ferrite (13)
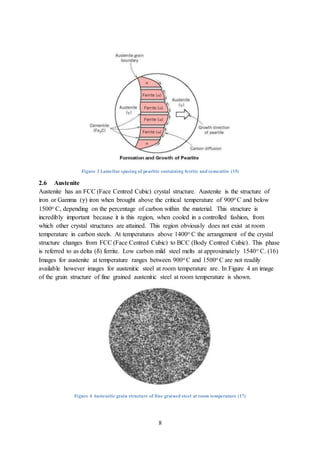
2.5 Pearlite
Pearlite is not a phase and it contains layers or lamellae of varying levels of cementite and
ferrite. Microscopically it appears as white layers of ferrite and dark layers of cementite. The
thickness of these ferrite layers and cementite layers depend on the material composition or
the manufacturing processing that the material may have undergone. (14) It is a very
desirable material property because it combines the strength and hardness of Cementite with
the property that is crucial for a vast range of steels which comes from ferrite, that property is
ductility. The fact that pearlite has a lamellar or layered structure enables the material to
inhibit the propagation of cracks, but this does not eradicate their growth. It merely makes the
growth of such cracks much more difficult. However pearlite comes in varying forms such as
coarse pearlite or fine pearlite. Coarse pearlite produces thicker lamellae and is formed when
the material is cooled slowly, this affects the mechanical properties of the material by
reducing its strength. Fine pearlite on the other hand produces thinner lamellae and is more
desirable because the strength of the material is significantly enhanced. Fine pearlite is
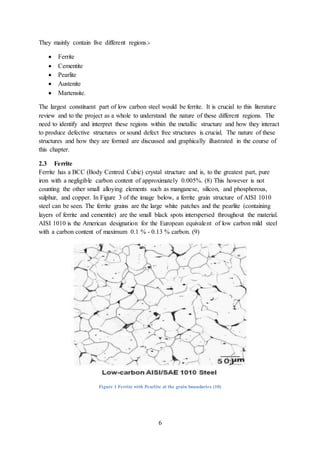
produced when the material is cooled rapidly. In Figure 3 below an image clearly shows that
there is a distinction between the lamellae of ferrite and cementite. (8)
8
Figure 3 Lamellar spacing of pearlite containing ferrite and cementite (15)
2.6 Austenite
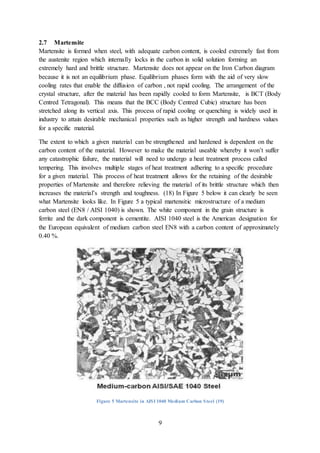
Austenite has an FCC (Face Centred Cubic) crystal structure. Austenite is the structure of
iron or Gamma (γ) iron when brought above the critical temperature of 900o C and below
1500o C, depending on the percentage of carbon within the material. This structure is
incredibly important because it is this region, when cooled in a controlled fashion, from
which other crystal structures are attained. This region obviously does not exist at room
temperature in carbon steels. At temperatures above 1400o C the arrangement of the crystal
structure changes from FCC (Face Centred Cubic) to BCC (Body Centred Cubic). This phase
is referred to as delta (δ) ferrite. Low carbon mild steel melts at approximately 1540o C. (16)
Images for austenite at temperature ranges between 900o C and 1500o C are not readily
available however images for austenitic steel at room temperature are. In Figure 4 an image
of the grain structure of fine grained austenitic steel at room temperature is shown.
Figure 4 Austenitic grain structure of fine grained steel at room temperature (17)
9
2.7 Martensite
Martensite is formed when steel, with adequate carbon content, is cooled extremely fast from
the austenite region which internally locks in the carbon in solid solution forming an
extremely hard and brittle structure. Martensite does not appear on the Iron Carbon diagram
because it is not an equilibrium phase. Equilibrium phases form with the aid of very slow
cooling rates that enable the diffusion of carbon , not rapid cooling. The arrangement of the
crystal structure, after the material has been rapidly cooled to form Martensite, is BCT (Body
Centred Tetragonal). This means that the BCC (Body Centred Cubic) structure has been
stretched along its vertical axis. This process of rapid cooling or quenching is widely used in
industry to attain desirable mechanical properties such as higher strength and hardness values
for a specific material.
The extent to which a given material can be strengthened and hardened is dependent on the
carbon content of the material. However to make the material useable whereby it won’t suffer
any catastrophic failure, the material will need to undergo a heat treatment process called
tempering. This involves multiple stages of heat treatment adhering to a specific procedure
for a given material. This process of heat treatment allows for the retaining of the desirable
properties of Martensite and therefore relieving the material of its brittle structure which then
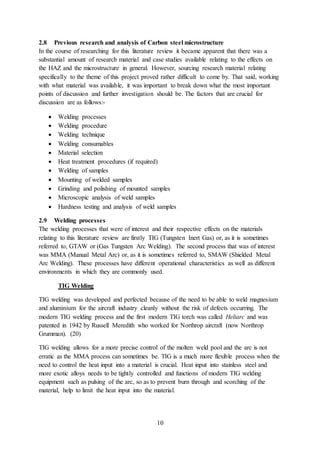
increases the material’s strength and toughness. (18) In Figure 5 below it can clearly be seen
what Martensite looks like. In Figure 5 a typical martensitic microstructure of a medium
carbon steel (EN8 / AISI 1040) is shown. The white component in the grain structure is
ferrite and the dark component is cementite. AISI 1040 steel is the American designation for
the European equivalent of medium carbon steel EN8 with a carbon content of approximately
0.40 %.
Figure 5 Martensite in AISI 1040 Medium Carbon Steel (19)
10
2.8 Previous research and analysis of Carbon steel microstructure
In the course of researching for this literature review it became apparent that there was a
substantial amount of research material and case studies available relating to the effects on
the HAZ and the microstructure in general. However, sourcing research material relating
specifically to the theme of this project proved rather difficult to come by. That said, working
with what material was available, it was important to break down what the most important
points of discussion and further investigation should be. The factors that are crucial for
discussion are as follows:-
 Welding processes
 Welding procedure
 Welding technique
 Welding consumables
 Material selection
 Heat treatment procedures (if required)
 Welding of samples
 Mounting of welded samples
 Grinding and polishing of mounted samples
 Microscopic analysis of weld samples
 Hardness testing and analysis of weld samples
2.9 Welding processes
The welding processes that were of interest and their respective effects on the materials
relating to this literature review are firstly TIG (Tungsten Inert Gas) or, as it is sometimes
referred to, GTAW or (Gas Tungsten Arc Welding). The second process that was of interest
was MMA (Manual Metal Arc) or, as it is sometimes referred to, SMAW (Shielded Metal
Arc Welding). These processes have different operational characteristics as well as different
environments in which they are commonly used.
TIG Welding
TIG welding was developed and perfected because of the need to be able to weld magnesium
and aluminium for the aircraft industry cleanly without the risk of defects occurring. The
modern TIG welding process and the first modern TIG torch was called Heliarc and was
patented in 1942 by Russell Meredith who worked for Northrop aircraft (now Northrop
Grumman). (20)
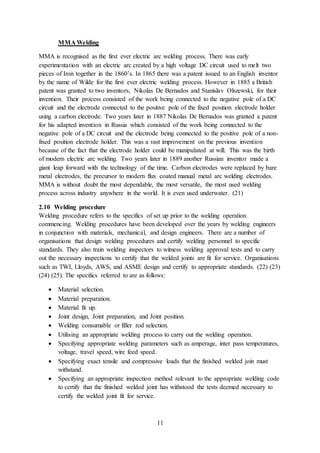
TIG welding allows for a more precise control of the molten weld pool and the arc is not
erratic as the MMA process can sometimes be. TIG is a much more flexible process when the
need to control the heat input into a material is crucial. Heat input into stainless steel and
more exotic alloys needs to be tightly controlled and functions of modern TIG welding
equipment such as pulsing of the arc, so as to prevent burn through and scorching of the
material, help to limit the heat input into the material.
11
MMA Welding
MMA is recognised as the first ever electric arc welding process. There was early
experimentation with an electric arc created by a high voltage DC circuit used to melt two
pieces of Iron together in the 1860’s. In 1865 there was a patent issued to an English inventor
by the name of Wilde for the first ever electric welding process. However in 1885 a British
patent was granted to two inventors, Nikolas De Bernados and Stanislav Olszewski, for their
invention. Their process consisted of the work being connected to the negative pole of a DC
circuit and the electrode connected to the positive pole of the fixed position electrode holder
using a carbon electrode. Two years later in 1887 Nikolas De Bernados was granted a patent
for his adapted invention in Russia which consisted of the work being connected to the
negative pole of a DC circuit and the electrode being connected to the positive pole of a non-
fixed position electrode holder. This was a vast improvement on the previous invention
because of the fact that the electrode holder could be manipulated at will. This was the birth
of modern electric arc welding. Two years later in 1889 another Russian inventor made a
giant leap forward with the technology of the time. Carbon electrodes were replaced by bare
metal electrodes, the precursor to modern flux coated manual metal arc welding electrodes.
MMA is without doubt the most dependable, the most versatile, the most used welding
process across industry anywhere in the world. It is even used underwater. (21)
2.10 Welding procedure
Welding procedure refers to the specifics of set up prior to the welding operation
commencing. Welding procedures have been developed over the years by welding engineers
in conjunction with materials, mechanical, and design engineers. There are a number of
organisations that design welding procedures and certify welding personnel to specific
standards. They also train welding inspectors to witness welding approval tests and to carry
out the necessary inspections to certify that the welded joints are fit for service. Organisations
such as TWI, Lloyds, AWS, and ASME design and certify to appropriate standards. (22) (23)
(24) (25). The specifics referred to are as follows:
 Material selection.
 Material preparation.
 Material fit up.
 Joint design, Joint preparation, and Joint position.
 Welding consumable or filler rod selection.
 Utilising an appropriate welding process to carry out the welding operation.
 Specifying appropriate welding parameters such as amperage, inter pass temperatures,
voltage, travel speed, wire feed speed.
 Specifying exact tensile and compressive loads that the finished welded join must
withstand.
 Specifying an appropriate inspection method relevant to the appropriate welding code
to certify that the finished welded joint has withstood the tests deemed necessary to
certify the welded joint fit for service.
12
2.11 Welding technique
Welding technique refers to the approach taken to the exact way in which a welding
operation will be carried out. There are a multitude of different variables that would dictate
what welding technique is appropriate for a given situation. These variables would include
material thickness, joint position, welding process, filler material selection and so on.
Different scenarios might dictate a specific deliberate hand movement of the welding rod or
torch. A certain scenario might call for stringer beads (26) to limit heat input into the material
whereas another scenario might call for a weave pass. (27) Each and every scenario,
regarding welding operations, is different and calls for a different technique to be used.
Knowing and understanding this only comes with experience.
2.12 Welding consumable material selection
Welding consumables vary hugely for the welding of different materials, using different
processes, in different environments. Welding using the manual metal arc process requires
the using of flux coated wire rods, which are inserted into the electrode holder and once
struck off the material to be welded an electric arc is initiated and welding commences. A
weld is created and the slag is chipped off. The slag acts to shield the developing molten weld
pool from oxygen and other atmospheric contaminants that would render the weld
unsatisfactory. (28)
Welding using the tungsten inert gas process requires a torch held non consumable electrode
in the form of a ground tungsten electrode which is used to initiate and maintain a high
frequency electric arc between the tungsten electrode and the base metal. Additional filler rod
material (if required) would be added to the weld pool by way of a long filler rod that is
dipped in and out of the weld pool as the tungsten is moved along the developing weld pool
without touching the base metal which would lead to unwanted contamination of the molten
weld pool. (29)
When selecting a filler material appropriate to the welding operation being carried out then
certain considerations must be taken into account. Attention to detail regarding the following
must be taken.
 Selecting a filler material with a chemical composition that closely matches the base
metal if materials joining is the focus of the welding operation.
 Do the mechanical properties of the welding consumables match or exceed those of
the base metal and those required for an in service welded joint.
 Has the proper storage procedure of the welding electrodes been stringently adhered
to, to prevent degradation of the welding electrodes.
 If surfacing was the primary focus of the welding operation, had the correct electrode
been selected bearing in mind what the surfacing layer was intended for. Was the
layer to be used as a buffer layer if indifferent materials are to be joined together or
was the purpose of the layer a hard facing layer to prevent corrosion, abrasion, or
erosion.
13
2.13 Material selection
Material selection refers to the selection of appropriate materials required for a specific
purpose. Materials, in the case of metals, would be selected as an appropriate material
required for the manufacture of sheet metal products or structural beams based on their
mechanical properties and chemical composition. If, for instance, a metal was required to
fabricate marine hardware then the material chosen would need to contain alloying elements
that would prevent or inhibit corrosion such as chromium and molybdenum. (30)
If, for instance, a material is required to enter service as a tool die in a drop forging machine
or a hydraulic punch for punching holes in other steels then this material has to possess some
very desirable qualities to withstand daily service in a very punishing environment. These
forging or punching dies would likely be made from material such as AISI O1 tool steel or
AISI D2 tool steel. (31) Therefore, as one would imagine, there are a number of variables that
would dictate what materials would be selected for the intended purpose.
2.14 Heat treatment procedure
Heat treatment is a process whereby varying levels of heat over a set time cycle is
administered to metals to impart specific mechanical properties into those metals. Heat
treatment processes such as annealing (32) may be used so as to be able to work that material
i.e. drilling, machining, welding. Welding of carbon steels with a carbon content above 0.4%
would be very difficult if not impossible to weld if that material was in its hardened state.
Another example would be if a similar material was in its annealed state and the properties
that were sought was increased hardness then, depending on the materials chemical
composition and carbon content, according to specific heat treatment procedures relating to
the specific material then it would be possible to significantly increase a materials hardness
by using a specific heat treatment procedure. This procedure, depending on composition,
would typically involve heating an annealed steel up to the austenite region and holding that
material at that temperature for a specific period of time and then quenching the material in
an appropriate medium such as oil or water. Then it would be required that the material be
tempered to regain some of the materials more desirable properties such as toughness and
ductility but, by virtue of this, the material will lose some of its hardness. It would also rid the
material of undesirable properties such brittleness. (33)
2.15 Welding of samples
The welding of samples for testing and evaluation should be carried out in as much of a
controlled environment as possible. It is imperative that when such welding operations are to
be undertaken it should be clear what procedures and protocol need to be adhered to so as to
minimise any deviation from what is required. If the object is to microscopically examine
defect free welded samples then it would be essential to limit the chance of introducing
unwanted defects into the welded samples. The welding operation including material fit up
and joint preparation should be undertaken by trained experienced personnel according to a
recognised and appropriate welding procedure specification (WPS). (34)
14
Having undertaken to work to a relevant welding procedure specification, the materials
would then need to be secured or fixed in a welding fixture so as to help limit any distortion
in the test pieces, however sometimes a small percentage of distortion is unavoidable
depending on the material being welded and how it is fixed. The joint type that would be
required for this work would be a single V open root butt weld. (35) The welds would be
completely fused at the root before being cleaned and prepared for the next runs so as to fill
up the plate and pipe chamfer with sound defect free weld metal. (36) When the entire butt
weld is completed then the finished weld metal should be slightly proud of the surface of the
base material. This would maintain the integrity of the original material thickness adjoining
the weld area.
2.16 Mounting of welded samples
The preparations required to mount a welded sample in a thermoset plastic would be done by
sectioning the sample using an appropriate cutting method. The sample would be sectioned
using a thin cutting disc which is enclosed in a sealed environment and flooded with coolant
to prevent the sample being scorched by overheating. This method would be used as opposed
to a band saw because the roughness of the finished cut of a band saw is not appropriate for
the first stage of grinding samples to prepare them for polishing. These samples are cut to the
maximum width of 25 mm according to the Buehler handbook for mounting samples. (37)
These samples would be sectioned transversely leaving the end of the weld visible and ready
for mounting.
Once the samples had been sectioned and cleaned with alcohol removing all traces of cutting
fluid they would be ready for mounting. The samples are placed inside the hollow cylindrical
chamber of a Buehler compressive mounting machine with a hydraulic ram at its base. The
sample would then be set face down with the face to be examined facing downward. A
measured amount of granulated phenolic thermoset resin (38) is poured into the chamber and
the chamber sealed shut with a twist lock clamp. The chamber would be preheated and then
the resin brought up to liquefying temperature and then pressurised by the hydraulic ram so
that the material formed a strong bond once cooled. The material then cools down and once
the cycle is finished, the sample would be extracted from the chamber and the welded sample
would be formed into a solid plastic mounting fixture similar in design to a miniature hockey
puck. (39)
2.17 Grinding and polishing of mounted samples
Mounted samples would be placed into a segmented cylindrical fixture with six slots in the
fixture which house the samples ready for grinding and polishing. The samples are then
clamped face down by a series of adjustable pneumatic actuators which exert the desired
amount of pressure onto the samples pressing them against the abrasive pads on the turntable.
(40) Depending on the material to be ground, a specific amount of pressure would be selected
and then a specific grade of abrasive used depending on which stage of grinding the samples
are undergoing. The variables for planar grinding & polishing and the pressures required as
well as the time required are laid out in Table 3 on page 34 further on in this report. The first
stage in grinding would be to use a relatively coarse water lubricated abrasive pad to remove
any surface deformation due to sectioning of the sample prior to mounting.
15
Continuing on from this would be progressively finer stages of abrasion using finer abrasive
pads to guarantee a clean flat surface with which to commence the initial stages of polishing.
The first stage of polishing removes any remnants of surface deformation to provide a smooth
mirror like finish. Multiple stages of polishing using a progressively finer water based
solution containing diamonds in suspension from 30 microns down to 1 micron would be
used. To highlight the area of interest ready for microscopic examination it would be
appropriate to use an etching solution that would increase the definition of the microstructure
ready for inspection. This step would be crucial to reveal the detail of the microstructure and
grain boundaries of the welded sample. (41)
2.18 Microscopic analysis of weld samples
Sometimes it is possible to see the grain structure of materials and any possible defects they
may have at the macroscopic level, that is to say the structural components can be viewed
with the naked eye. However to understand and interpret the microstructure of polished and
etched samples it would be necessary to view them microscopically so as to identify the
different regions within the sample and to identify defects, if any, present within the grain
structure of the material. (42)
When materials are to be viewed microscopically, depending on what level of detail one
wishes to observe, microscopy equipment with varying power of magnification is necessary
for the investigation. The most common and most accessible form of microscopy is optical
microscopy. For this kind of microscopic examination to be viable the samples to be
examined need to be highly polished and have a mirror like finish. Depending on what
regions of the grain structure and grain boundaries that are of interest, would dictate what
kind of etching solution would be required.
Chemical etching is necessary to reveal a metal’s microstructure, it is by selective use of
particular etching solutions that chemically degrade a particular area of the grain structure
preferentially to another. The areas that are likely be attacked by the etching solutions would
be points of high energy such as areas where defects are present as well as the grain
boundaries. (43)
2.19 Hardness testing and analysis of weld samples
There are multiple hardness test techniques that are used to determine the hardness of
materials such as Rockwell, Brinell, Vickers. There is also another technique that is of
particular use when it is necessary to examine the micro hardness of small samples. This
micro hardness testing technique is called Vickers Micro Hardness. This technique utilises a
diamond indenter which is shaped like an inverted pyramid, this indenter is forced into the
material’s surface using specific applied loads from between 1.0 grams and 1000 grams. (44)
The indentation that is left on the surface of the material can be accurately measured, this
measurement can then be converted into a hardness number using formulae that are specific
to the Rockwell, Brinell (HB), Vickers Micro Hardness (HV) testing techniques. (45)
16
To accurately test the hardness variations across a welded sample it would be necessary to
make indentations across the sample from the base metal across into the heat affected zone
and into the weldment. These indentations are made both horizontally and vertically right
across the welded sample to obtain a truly accurate picture of the variation in hardness within
the microstructure. Those figures would be used to create a graph via an Excel spreadsheet so
as to graphically illustrate how those hardness values vary across the sample due to the
varying levels of heat input into the material. The carbon content within the material would
also be one of the main variables that determine the variation in hardness values. (46)
2.20 A review of research papers into the field of weld microstructures and their
defects and the causes of such defects
Influence of welding method on microstructural creation of welded joints. Čičo P.,
Kalincová D., Kotus M.,. Special Issue - S50-S56, Zvolen - Slovakia : Czech Agriculture
Journals, 2011, Vol. 57. (47)
The research carried out, as illustrated in this paper, relates to the analysis and interpretation
of the effects that various arc welding processes have on the microstructure and metallurgical
quality of welded steel joints. The samples were welded with the MMA welding process as
well as the MIG/MAG welding process. Analysis of the welded steel joints at the macro and
microstructural level confirmed that grain structure and grain size is influenced by the
particular welding parameters.
The material used for the welding operation was a low carbon steel. For the MMA welding
process the welding consumable used were listed under the Slovak designation of “EB-121”
– These rods are the Slovak equivalent of what is known in western Europe and America as
7018 Low Hydrogen electrodes. (48) (49) For the MIG/MAG Welding process the
consumables that were used were listed under the Slovak designation of “ESAB OK Autorod
12.58” – The western European and American equivalent of this MIG/MAG wire is known as
ER70S-3. (50)
The exponential heat change caused by the rapid input of heat energy into the material being
welded is indicative of what happens during most arc welding procedures. The resultant
microstructure is dependent on what kind of welding process is used and the heat input
necessary to create a given microstructure is directly proportional to the operational arc
voltage and welding amperage. The material thickness is related to the rate of heat dissipation
from the welded joint throughout the material. The specific temperature for the material
where austenite is formed and its rate of transformation is dependent not just on the chemical
composition and the mechanical properties of the material but also its dimensions.
According to the results obtained during the course of this investigation it was discovered that
there is more heat imparted into the base metal and, by virtue of that fact, the HAZ by the
MMA welding process than the MIG/MAG welding process. The slower deposition rate of
weld metal using the MMA process as opposed to the much quicker deposition rate of
MIG/MAG is directly related to the higher rates of heat input by the MMA process into the
material.
17
Therefore it can be concluded, according to this research, using the specific consumables &
materials and parameters that the HAZ is 20 % to 30% narrower using the MIG/MAG
process. This is a point of interest that needs to be investigated in relation to the differences in
heat input between MMA and TIG which relates directly to this project. It can be safely
asserted that the welding processes, along with the welding parameters, strongly influence the
physical and mechanical properties of the finished welded joints. This is a factor that must be
taken into account when deciding on what kind of process would be the most appropriate for
the welding operation that needs to be carried out.
Defects - Hydrogen cracks in steels - Identification. Bill Lucas, Gene Mathers,
David Abson. Cambridge : Connect (Orignal) - Amended version by The Welding Institute,
2000 (51)
Hydrogen induced cracking (HIC) comes under a few different names such as cold cracking
as well as delayed cracking. Regardless of what the defect is called, the end result of the
defect is the same. This kind of critical defect occurs in ferritic steels. These defects are
caused by the presence of diffusible hydrogen within the steel or the welding electrodes, a
microstructure prone to HIC, and sufficient tensile loads. From past research is has become
understood that in carbon manganese steels, hydrogen induced cracking originates most
frequently in the HAZ at the toes of the weld but can also travel from the HAZ and into the
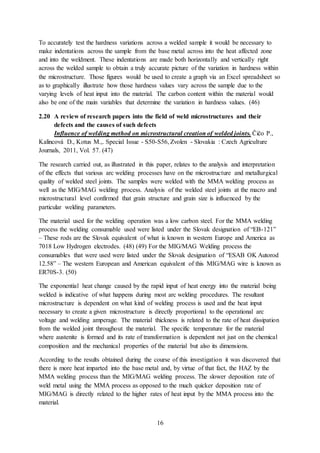
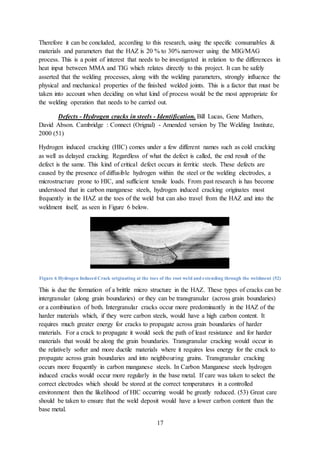
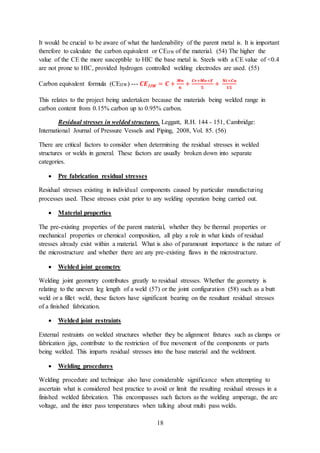
weldment itself, as seen in Figure 6 below.
Figure 6 Hydrogen Induced Crack originating at the toes of the root weld and extending through the weldment (52)
This is due the formation of a brittle micro structure in the HAZ. These types of cracks can be
intergranular (along grain boundaries) or they can be transgranular (across grain boundaries)
or a combination of both. Intergranular cracks occur more predominantly in the HAZ of the
harder materials which, if they were carbon steels, would have a high carbon content. It
requires much greater energy for cracks to propagate across grain boundaries of harder
materials. For a crack to propagate it would seek the path of least resistance and for harder
materials that would be along the grain boundaries. Transgranular cracking would occur in
the relatively softer and more ductile materials where it requires less energy for the crack to
propagate across grain boundaries and into neighbouring grains. Transgranular cracking
occurs more frequently in carbon manganese steels. In Carbon Manganese steels hydrogen
induced cracks would occur more regularly in the base metal. If care was taken to select the
correct electrodes which should be stored at the correct temperatures in a controlled
environment then the likelihood of HIC occurring would be greatly reduced. (53) Great care
should be taken to ensure that the weld deposit would have a lower carbon content than the
base metal.
18
It would be crucial to be aware of what the hardenability of the parent metal is. It is important
therefore to calculate the carbon equivalent or CEIIW of the material. (54) The higher the
value of the CE the more susceptible to HIC the base metal is. Steels with a CE value of <0.4
are not prone to HIC, provided hydrogen controlled welding electrodes are used. (55)
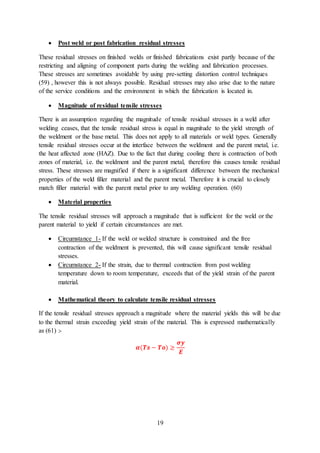
Carbon equivalent formula (CEIIW) --- 𝑪𝑬 𝑰𝑰𝑾 = 𝑪 +
𝑴𝒏
𝟔
+
𝑪𝒓+𝑴𝒐+𝑽
𝟓
+
𝑵𝒊+𝑪𝒖
𝟏𝟓
This relates to the project being undertaken because the materials being welded range in
carbon content from 0.15% carbon up to 0.95% carbon.
Residual stresses in welded structures. Leggatt, R.H. 144 - 151, Cambridge:
International Journal of Pressure Vessels and Piping, 2008, Vol. 85. (56)
There are critical factors to consider when determining the residual stresses in welded
structures or welds in general. These factors are usually broken down into separate
categories.
 Pre fabrication residual stresses
Residual stresses existing in individual components caused by particular manufacturing
processes used. These stresses exist prior to any welding operation being carried out.
 Material properties
The pre-existing properties of the parent material, whether they be thermal properties or
mechanical properties or chemical composition, all play a role in what kinds of residual
stresses already exist within a material. What is also of paramount importance is the nature of
the microstructure and whether there are any pre-existing flaws in the microstructure.
 Welded joint geometry
Welding joint geometry contributes greatly to residual stresses. Whether the geometry is
relating to the uneven leg length of a weld (57) or the joint configuration (58) such as a butt
weld or a fillet weld, these factors have significant bearing on the resultant residual stresses
of a finished fabrication.
 Welded joint restraints
External restraints on welded structures whether they be alignment fixtures such as clamps or
fabrication jigs, contribute to the restriction of free movement of the components or parts
being welded. This imparts residual stresses into the base material and the weldment.
 Welding procedures
Welding procedure and technique also have considerable significance when attempting to
ascertain what is considered best practice to avoid or limit the resulting residual stresses in a
finished welded fabrication. This encompasses such factors as the welding amperage, the arc
voltage, and the inter pass temperatures when talking about multi pass welds.
19
 Post weld or post fabrication residual stresses
These residual stresses on finished welds or finished fabrications exist partly because of the
restricting and aligning of component parts during the welding and fabrication processes.
These stresses are sometimes avoidable by using pre-setting distortion control techniques
(59) , however this is not always possible. Residual stresses may also arise due to the nature
of the service conditions and the environment in which the fabrication is located in.
 Magnitude of residual tensile stresses
There is an assumption regarding the magnitude of tensile residual stresses in a weld after
welding ceases, that the tensile residual stress is equal in magnitude to the yield strength of
the weldment or the base metal. This does not apply to all materials or weld types. Generally
tensile residual stresses occur at the interface between the weldment and the parent metal, i.e.
the heat affected zone (HAZ). Due to the fact that during cooling there is contraction of both
zones of material, i.e. the weldment and the parent metal, therefore this causes tensile residual
stress. These stresses are magnified if there is a significant difference between the mechanical
properties of the weld filler material and the parent metal. Therefore it is crucial to closely
match filler material with the parent metal prior to any welding operation. (60)
 Material properties
The tensile residual stresses will approach a magnitude that is sufficient for the weld or the
parent material to yield if certain circumstances are met.
 Circumstance 1- If the weld or welded structure is constrained and the free
contraction of the weldment is prevented, this will cause significant tensile residual
stresses.
 Circumstance 2- If the strain, due to thermal contraction from post welding
temperature down to room temperature, exceeds that of the yield strain of the parent
material.
 Mathematical theory to calculate tensile residual stresses
If the tensile residual stresses approach a magnitude where the material yields this will be due
to the thermal strain exceeding yield strain of the material. This is expressed mathematically
as (61) :-
𝜶(𝑻𝒔 − 𝑻𝒐) ≥
𝝈𝒚
𝑬
20
Where: α is the coefficient of thermal expansion for the specific material
Ts is the softening temperature (a point where yield is 10% of normal yield)
To is the ambient or room temperature
E is the Young’s modulus for the specific material
σy is the yield strength of the material at ambient temperature
 Restraint of welded joints
If a weld or welded structure is in anyway restricted in its free movement during thermal
expansion or contraction then it is said to be “restrained”. As can be imagined, in a structure
with multiple welds in multiple directions, welded joints may experience restraint in uniaxial
direction, thus developing tensile residual stresses within the fabrication. If consideration is
given to the need for pre-setting the fabrication components where possible then the restraint
experienced by the structure can be considerably less.
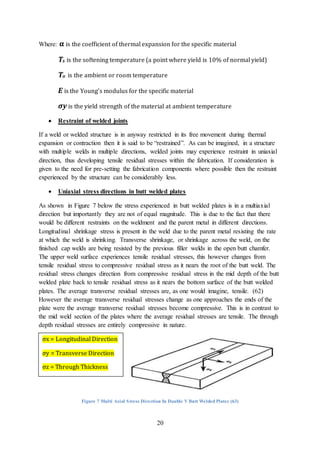
 Uniaxial stress directions in butt welded plates
As shown in Figure 7 below the stress experienced in butt welded plates is in a multiaxial
direction but importantly they are not of equal magnitude. This is due to the fact that there
would be different restraints on the weldment and the parent metal in different directions.
Longitudinal shrinkage stress is present in the weld due to the parent metal resisting the rate
at which the weld is shrinking. Transverse shrinkage, or shrinkage across the weld, on the
finished cap welds are being resisted by the previous filler welds in the open butt chamfer.
The upper weld surface experiences tensile residual stresses, this however changes from
tensile residual stress to compressive residual stress as it nears the root of the butt weld. The
residual stress changes direction from compressive residual stress in the mid depth of the butt
welded plate back to tensile residual stress as it nears the bottom surface of the butt welded
plates. The average transverse residual stresses are, as one would imagine, tensile. (62)
However the average transverse residual stresses change as one approaches the ends of the
plate were the average transverse residual stresses become compressive. This is in contrast to
the mid weld section of the plates where the average residual stresses are tensile. The through
depth residual stresses are entirely compressive in nature.
Figure 7 Multi Axial Stress Direction In Double V Butt Welded Plates (63)
σx = Longitudinal Direction
σy = Transverse Direction
σz = Through Thickness
21
Metallographic Basics Donald C. Zipperian, Ph.D.
http://www.metallographic.com/Technical/Basics.pdf.
http://www.metallographic.com. [Online] Pace Technologies. [Cited: 22nd November
2015.] (64)
Metallography is the in depth investigation and analysis of the microstructure of materials.
This is a field of study that is crucial in ascertaining whether a material has been
manufactured in the correct manner or if it has been subject to stringent post manufacturing
processes so that its microstructure and its mechanical properties have not been detrimentally
affected. For the sake of determining if a material can withstand the in service demands that
will be placed upon it, it is crucial to have proven methods of analysis that will aid in the
identification of inherent flaws or defects that are present within a material’s microstructure.
There are a number of steps that are crucial in metallographic preparation. (65) They
include:-
 Initial preparation – By documenting the original initial condition of the specimen it
would be a reference for future investigations. It is important to take this first initial
step so as to record how the specimens appear before they are exposed to the
environment for a prolonged period which may hasten corrosion.
 Cutting and sectioning – Initial cutting of specimens, especially large specimens,
maybe carried out using a conventional band saw. But when the specimens are to be
sectioned it is absolutely crucial that these specimens are sectioned within the area of
interest using an appropriate cutting method. The method that is common in the
metallographic preparation industry is using a very fine surface abrasive cutting disc
aided by coolant so as to prevent the scorching of the sample. This step is really
important because this provides the initial surface that is necessary for proper
mounting and for the first stages of planar grinding which provides controlled
abrasion for scratch removal from the sample surface.
 Compression mounting of samples – Compression mounting of samples is carried
out by fixing or “mounting” the sample within a confined shape which aids in the ease
of handling for analysis and storage. This shape is usually a circular shaped disc
approximately 30 mm to 50 mm in diameter and approximately 25 mm thick that has
the appearance of a hockey puck.
The material used for hot compressive mounting is usually a thermoset polymer
which comes in granular form. The granular thermoset is poured into a cylindrical
chamber in which the prepared and sectioned sample is housed. The housing of this
cylindrical chamber is locked shut and the cycle is commenced. This cycle consists of
a preheating period of two minutes followed by a heating period of four minutes
whereby the thermoset polymer is heated to 400oC. Depending on the exact mounting
material being used and the specimens being prepared, the sample is subjected to 300
bar of pressure. Once these phases of the cycle are complete then the final phase
commences and this is the cooling phase which last approximately two minutes. Once
this phase has finished then the cycle is complete, the sample is then released from the
compressive mounting machine and ready for the first stages of planar grinding.
22
 Planar grinding – This is the initial stage in the preparation of mounted samples.
This step is crucial for a number of reasons. It prepares the surface for stock removal
of material to attain a plain smooth surface that is devoid of deep scratches. Once the
deep scratches have been removed then the successively finer stages of abrasion can
commence. The abrasive pads are usually 240 grit, 320 grit, 400 grit, 600 grit, and
finally 800 grit. (66) The higher number of grit particles per unit area means that this
particular pad is a finer finish pad. These stages of abrasion must be adhered to and
there are no shortcuts to attaining the surface required for initial polishing. There are
various parameters that must also be adhered to such as speed of rotating head on
metallographic grinding machine, whether the sample is to be ground in a
complimentary or contradictory direction to that of the rotating head. The duration of
grinding cycle and the downward pressure per sample(s) are also important
parameters whereby proper guidelines laid out in industry standard equipment
manuals must be adhered to.
 Initial or “rough” polishing – This, as its name implies, is the first or “rough”
polishing stage which prepares the surface of the specimen for finer polishing by
removing the really fine scratches that were left on the specimen surface by the last
final abrasion stage. Once the surface has been prepared in this manner then it will
make it easier for the specimen to be polished more finely. The polishing stages, in
contrast to the abrasion stages, require only a few minutes to complete. At this stage
of preparation the grain structure of the sample would not change but the surface
would appear smoother and more polished. Rough polishing is initiated by using a 9
micron down to 3 micron diamond suspension solution as a lubricant and polishing
solution. (67) The polishing cloth that is used in conjunction with the diamond
abrasive solution is made from nylon.
 Final Polishing – The reason for the final polishing stage is that it prepares the
specimen surface for etching. This is just a final polishing stage using a 1 micron
alumina slurry in conjunction with a napped micro cloth that has the texture and
appearance of velvet. (68) This stage can only commence once all surface damage has
been removed and the previous successive rough polishing stages have properly
carried out.
 Etching – The reason for etching is because of the need to provide contrast which
highlights the features of interest in the specimen ready for microscopic inspection.
Etching allows for the visual inspection of a specimen and gives texture to the
features such as grain structure, grain boundaries, and zone boundaries. The etchant is
used to selectively corrode specific areas within the microstructure. (69) Chemical
etchants are usually of an acidic or basic nature and are used in relatively mild
solution. This gives definition and highlights the areas of interest that need to be
inspected. Once an etchant has been applied to a specimen it is allowed to take effect
for a number of minutes or a number of seconds in most cases. It is then immersed in
deionized water which ceases the chemical reaction of the etchant and then the
surface is cleaned using ethanol. The specimen is then dried under a warm air dryer.
23
 Microscopic analysis – Microscopic examination is carried out using microscopes of
varying magnification and resolution. Microscopic analysis of a specimen’s
microstructure provides the materials engineer with specific information relating to
grain structure and any changes that it may have undergone due to any heat treatment
process, welding process, or forming process. It is also crucial in identifying any
inherent flaws or defects in the microstructure of a material such as defects caused
during the manufacturing process whether this is a casting or a forging or a welded
fabrication. There is a real need to be able to examine a material’s grain structure and
to determine whether it has a fine grain structure or a coarse grain structure because
this information can help the materials engineer to determine the material’s
mechanical properties such as ductility and hardness.
 Hardness testing – Hardness testing is incredibly important and the information
attained from standardised testing procedures allows the material engineer to relate
this information to other material properties such as tensile strength, ductility, and
wear resistance. Micro Hardness testing is carried out using the Vickers procedure.
This method is carried out using indenters that are subject to loads between 1 gram
and 1000 grams of force. This procedure is used to measure the hardness of different
zones within a material such as the parent material, the heat affected zone or the HAZ
and the weldment.
Vickers Micro Hardness Formula (70) :- HV =
𝟐𝑷 𝑺𝒊𝒏(
𝜽
𝟐
)
𝑳 𝟐 =
𝟏.𝟖𝟓𝟒 𝑷
𝑳 𝟐
Where P = Applied load in kg
L = Average length of diagonals in mm
ϴ = Angle between opposite facets of diamond indenter (136o)
24
Chapter 3 Preparation of test samples
3.1 Designof welded coupons
The coupons that were welded were prepared in accordance with the ASME IX (American
Society of Mechanical Engineers section 9) welding procedure specification. (71) The
samples that were used were prepared using four different materials. Mild steel, EN 8, API
5L, and O1 Tool Steel were used for this investigation. These samples were welded using two
different electric arc welding processes, MMA and TIG. Half of the samples were welded to
a defect free standard, and the other half were purposefully welded with defects. For
comparison there was a control sample of each material to show the difference between the
microstructure of the material which had not been subjected to any kind of microstructural
change due to heat input from welding or any heat treatment process.
3.2 Preparation of MMA welded carbon steel pipe (API 5L)
The pipe that was used was 4.5” schedule 80 seamless carbon steel pipe (carbon content
approx. 0.25%). (72) The pipe bevel was machined in the lathe with a 65o to 70o inclusive
angle (.i.e. 32.5o to 35o for each chamfered pipe) with a 2.5mm root gap to accommodate the
MMA electrode diameter of 2.5 mm. The root face or landing edge was approximately 2.5
mm in width. The pipe was set up in preparation for welding by aligning the two most
appropriate points on the pipe where there was no misalignment of the pipe inside wall. This
was not easy to do because all pipe is slightly elliptical. Once the pipe had been aligned it
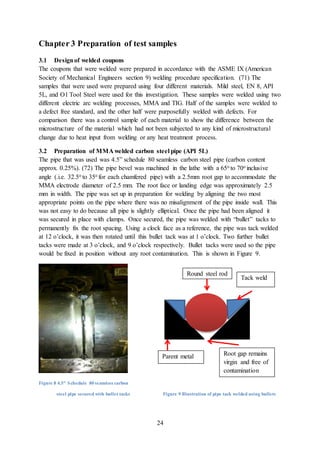
was secured in place with clamps. Once secured, the pipe was welded with “bullet” tacks to
permanently fix the root spacing. Using a clock face as a reference, the pipe was tack welded
at 12 o’clock, it was then rotated until this bullet tack was at 1 o’clock. Two further bullet
tacks were made at 3 o’clock, and 9 o’clock respectively. Bullet tacks were used so the pipe
would be fixed in position without any root contamination. This is shown in Figure 9.
Figure 8 4.5" Schedule 80 seamless carbon
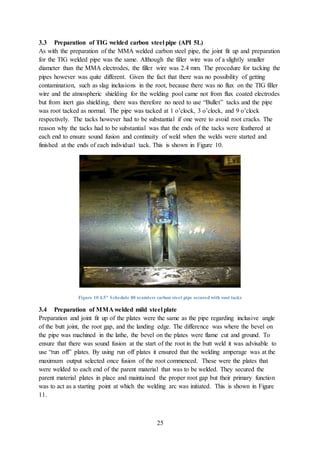
steel pipe secured with bullet tacks Figure 9 Illustration of pipe tack welded using bullets
Parent metal
Round steel rod
Tack weld
Root gap remains
virgin and free of
contamination
25
3.3 Preparation of TIG welded carbon steel pipe (API 5L)
As with the preparation of the MMA welded carbon steel pipe, the joint fit up and preparation
for the TIG welded pipe was the same. Although the filler wire was of a slightly smaller
diameter than the MMA electrodes, the filler wire was 2.4 mm. The procedure for tacking the
pipes however was quite different. Given the fact that there was no possibility of getting
contamination, such as slag inclusions in the root, because there was no flux on the TIG filler
wire and the atmospheric shielding for the welding pool came not from flux coated electrodes
but from inert gas shielding, there was therefore no need to use “Bullet” tacks and the pipe
was root tacked as normal. The pipe was tacked at 1 o’clock, 3 o’clock, and 9 o’clock
respectively. The tacks however had to be substantial if one were to avoid root cracks. The
reason why the tacks had to be substantial was that the ends of the tacks were feathered at
each end to ensure sound fusion and continuity of weld when the welds were started and
finished at the ends of each individual tack. This is shown in Figure 10.
Figure 10 4.5" Schedule 80 seamless carbon steel pipe secured with root tacks
3.4 Preparation of MMA welded mild steel plate
Preparation and joint fit up of the plates were the same as the pipe regarding inclusive angle
of the butt joint, the root gap, and the landing edge. The difference was where the bevel on
the pipe was machined in the lathe, the bevel on the plates were flame cut and ground. To
ensure that there was sound fusion at the start of the root in the butt weld it was advisable to
use “run off” plates. By using run off plates it ensured that the welding amperage was at the
maximum output selected once fusion of the root commenced. These were the plates that
were welded to each end of the parent material that was to be welded. They secured the
parent material plates in place and maintained the proper root gap but their primary function
was to act as a starting point at which the welding arc was initiated. This is shown in Figure
11.
26
Figure 11 10 mm Thick mild steel plate MMA butt joint
3.5 Preparation of TIG welded mild steel plate
The joint preparation and joint fit up of the TIG butt welded mild steel plate was the same as
the MMA butt welded mild steel plate, the only difference was the welding process. This is
shown in Figure 12.
Figure 12 10 mm Thick mild steel plate TIG butt joint
3.6 Preparation of MMA and TIG welded medium carbon steel flat (EN 8)
The EN 8 weld coupons were much smaller in thickness than the pipe and plate samples. The
EN 8 samples were 5 mm in thickness. The butt joint was only 40 mm in width before
sectioning. The samples were bevelled to no more than 35o inclusive angle, because there was
no need to have such a lean angle due the material being half the thickness of the mild steel
plates. Due to the fact that the material was only 5 mm thick there was no need for a wide
root gap, a maximum of 2mm root gap was sufficient for full penetration using both MMA
and TIG welding processes. The EN 8 butt joints for both MMA and TIG were prepared in
exactly the same fashion and were identical other than the fact that they were welded using a
different process. Figure 13 shows the sample prepared for both processes.
27
Figure 13 EN 8 6 mm butt joint for MMA & TIG
3.7 Preparation of MMA and TIG welded high carbon tool steel flat (O1tool steel)
The tool steel specimens were prepared from a piece of ground flat stock of O1 tool steel
which was 70 mm in width by 6 mm in thickness. The material was supplied in the annealed
state. To try and limit, as much as possible, the chance of immediate brittle fracture upon
welding due to the shape of the butt joint (a single V butt), it was decided that the joint
configuration should be simulated. It was preferable to weld the tool steel in this fashion to
avoid the possibility of stress concentrations in the joint. What was meant by simulated is that
it would not be two separate pieces of tool steel joined together but a single piece of tool steel
with a U shaped trough milled through its length with a bull nose cutter. This radial shaped
simulated U shaped butt would limit the chances of immediate failure, although failure upon
cooling was expected anyway because this was a joining operation and not a surfacing
operation where the chances of cracking and ultimate failure could be avoided. The tool steel
sample prior to machining was marked by single red lines where the U shaped trough was
milled. Once the sample was milled it was cut into three individual samples. This is shown in
Figure 14.
Figure 14 Bull Nose milling of U shaped trough (73)
Bull nose
cutters U shaped
milled trough
28
Figure 15 O1 Tool steel prior to milling of U shaped trough
3.8 Welding procedure for test samples
Welding procedure for MMA welding of carbon steel pipe (API 5L) and mild steel
plate
The pipe and plate were preheated to a low preheat temperature just to eradicate any
hydrogen present in the material prior to welding. The welding consumables used for the root
were of a hydrogen controlled specification with <15ml of diffusible hydrogen per 100 grams
of weld metal deposit. They were of AWS specification E7016 (Oerlikon Spezial) which are
a low hydrogen potassium coated manual metal arc electrode. The rods were re-dried at
300oC – 350oc as per manufacturer’s specifications (74) for 2 hours prior to being stored in a
rod heating quiver during the welding operation. The rods used for the hot pass, the fill, and
the cap runs were also of an extremely low hydrogen controlled specification with <5ml of
diffusible hydrogen per 100 grams. The rods used were of AWS specification E7018-1
(Lincoln Electric Conarc 49c) which are a low hydrogen iron powder coated manual metal
arc electrode. These rods were also re-dried at 300o C – 350o C as per manufacturer’s
specifications (75) for 2 hours prior to being stored in a rod heating quiver during the welding
operation. The finished welded pipe and plate are shown in Figures 16 and 17 below.
Figure 16 4.5 Inch Schedule 80 MMA Welded API 5L carbon steel pipe
Welding capping runs
using E7018-1
consumable
4&1/2”
Schedule
80
seamless
carbon
steel pipe
- Grade
API 5L
Pipe fixed in pipe
clamp at HLO
45O
29
Figure 17 10 mm MMA butt welded mild steel plate
Figure 18 BOC Welding Preheat Temperature Chart (76)
Welding procedure for TIG welding of carbon steel pipe (API 5L) and mild steel
plate
As with the previous welding procedure for pipe and plate the specimens were preheated to a
low pre heat temperature as shown Figure 18. This was done to eradicate any hydrogen
present prior to commencing the welding operation. The welding electrodes, or filler wire as
it is referred to when speaking of TIG welding consumables, were of AWS specification ER
70s-2 (BÖhler super steel). The root, fill, and cap runs for both pipe and plate were carried
out using the same filler wire, the gas shielding for the welding operation was argon.
Welding procedure for TIG & MMA welding of medium carbon steel (EN 8)
The welding procedure for welding medium carbon steel (EN 8) involved a preheating
procedure that varies with choice of welding consumable. However if welding sections <18
mm in thickness a rigorous heat treatment process can be avoided. (77) However in this case
it was advisable to preheat the material to eradicate any hydrogen present to prevent
hydrogen infused cracking (HIC). For this procedure a nickel based welding consumable
known as 312 stainless (ESAB OK 68.81) was used. (78)
300 mm long x 100
mm wide x 10 thick -
mild steel plate
Weaved capping run
using E7018-1
welding electrodes
30
The reason for this choice was because the nickel based electrode had a thermal expansion
coefficient that was fairly close to that of the base material which greatly reduced the chances
of cracking if the joint was in any way restrained. (79) The welding procedure for MMA and
TIG welding of EN 8 was the same as regards the choice of welding consumables. 312
stainless electrodes (80) and 312 TIG filler wire (81) was used in both processes, however in
the case of TIG welding, a gas lens was used on the TIG torch to provide adequate gas
shielding and prevent oxidisation of the weldment. (82) This is shown in Figure 19.
Figure 19 Gas diffusion pattern of gas lens Vs standard nozzle (83)
Figure 20 MMA welded EN 8 medium carbon steel
Figure 21 TIG welded EN 8 medium carbon steel
31
Welding procedure for MMA and TIG welding of O1 tool steel
Joining O1 tool steel is not advisable because of the possibility of HIC and brittle fracture
due to the very high carbon content of 0.95 %. O1 tool steel is repaired when there maybe
surface cracks or wear. It is usually “buttered” with a layer of softer material such as a nickel
based 312 stainless filler material before it is “hard faced” with a material that closely
matches the tool steel. In this case a weld was made in a trough that was milled in the
material to a depth of 4 mm, this simulated a U shaped butt joint. Due to the small size of the
samples they only needed to be preheated to 150oC prior to welding. (84) They were then
stress relieved at 650oC for a short time and then allowed to cool naturally in the furnace
overnight. (85) This procedure was only done for one MMA sample and one TIG sample.
The second set of samples were pre-heated to 150oC but after welding they were allowed to
cool in the air. The third set of samples were only slightly warmed up to eradicate any
hydrogen present and the material were only hand warm prior to welding. After welding, the
third set of samples were allowed to cool in the air. In all cases, all welding of O1 tool steel
was carried out using 312 stainless MMA electrodes or 312 stainless filler wire.
3.9 Sectioning of weld samples
Prior to sectioning the samples to the size required for mounting, they were cut using a band
saw. The samples were then further cut down to size using a thin high speed abrasive disc
which was flooded with coolant to prevent the preliminary surface from getting scorched.
This gives the sample its required preliminary surface needed for mounting. This operation
was carried out using the Buehler Abrasimet 2. (86) This machine is shown in Figure 22.
Figure 22 Buehler Abrasimet 2 abrasive disc cutter
3.10 Compression mounting of samples
The compression mounting of the specimens was done by placing the samples face down
inside an enclosed cylindrical chamber which houses a hydraulic ram. On top of the specimen
was poured a measured amount of granulated phenolic polymer. Once the samples had been
placed correctly inside the chamber and the granulated polymer had been poured into the
chamber, the chamber was then locked and closed with the aid of a twist lock clamp. The
cycle was then initiated. The cycle included the pre heating for 1 minute of the polymer, it
was then that the material was fully heated to 300oC and pressurised to 30 bar via the
hydraulic ram for 3 minutes. Once this time had elapsed the sample underwent a cooling
down period of 2 minutes within the enclosed chamber which allowed the polymer to solidify
and cool down, housing the sample securely. The cycle then terminated. This was carried out
using a Buehler Simplemet 3000. (87) This is shown in Figure 23.
32
Figure 23 A Buehler Simplimet 3000 compression mounting sampling machine
3.11 Planar grinding and polishing of samples
Planar grinding of samples
The first stage of the abrasion was carried out using 240 grit silicon carbide abrasive paper,
which was primarily used for stock removal so as to provide a flat surface devoid of any
major scratches or uneven surfaces. The number of cycles of planar grinding varied with
every sample, because some had very good preliminary surfaces which were very flat where
some others were slightly uneven. After using 240 grit until a completely flat even surface
was obtained with all major scratches removed, the next stage of planar grinding commenced.
The next grade of abrasive paper used was 320 grit, which further removed any slightly less
obvious scratches and was used for 2 minutes per cycle. Once 320 grit had been used for a
period of time the next stage of planar grinding commenced. At this stage the abrasive used
was 600 grit SiC paper which is a much finer grade of abrasive. This was used to finely grind
the sample surface and ensure that all the real fine scratches were running in the same
direction, this meant that all other major scratches had been removed. The final stage of
planar grinding was done using an 800 grit SiC paper. This extremely fine abrasive paper was
used to very finely grind the surface of the sample in preparation for polishing. At this stage
the surface scratches had been entirely removed.
Polishing of samples
The first stage of polishing was carried out using a nylon pad in conjunction with a 9μm
diamond water based solution. The solution contained fine diamond in suspension, this
polishing lubricant was sprayed onto the turntable at 15 second intervals. This stage of
polishing consisted of one 4 minute cycle which refined the surface to a really clean finish.
The second stage of polishing was carried out using a much finer nylon cloth pad in
conjunction with a finer water based solution with a diamond particle size of 5μm. This stage
gave a blemish free finish to the sample surface. This stage of polishing consisted of one four
minute cycle and the polishing lubricant was also sprayed onto the turntable in 15 second
intervals. The final stage of polishing was carried out using a fine velvet like pad called a
microcloth in conjunction with an extremely fine alumina slurry which contained 1μm
alumina particles in suspension. This stage of polishing gave a mirror like finish to the
sample and was devoid of any surface defects. The variables of all the grinding and polishing
operation are clearly outlined in Table 3 on page 34.
33
Etching of samples
Etching of the samples was carried out to aid in the preferential corrosion of the
microstructure on the sample surface. This was done by using a 2% nitric acid solution called
“Nital”. The samples were cleaned with ethanol and then dried under an air dryer prior to the
application of the acid solution. Once the etchant was applied to the surface with a cotton bud
it was allowed to settle for five seconds. Once this time had elapsed there was a very clear
definition of the surface grain structure. The samples were then immersed in clean fresh
water to cease the chemical reaction of the acid attacking the surface grain structure. The
samples were then taken out of the water and dried under an air dryer. The samples were then
ready for macroscopic and microscopic examination.
3.12 Table of variables for planar grinding and polishing
Table 3 on page 34 clearly lays out the variables for planar grinding and polishing. This
includes the abrasives used as well as the coolant/lubricant for each stage of surface
preparation. The pressure required to secure the samples to the platen, the platen speed, the
head speed, and the cycle time are all clearly laid out in the table. All planar grinding and
polishing was carried out using the Buehler Phoenix 4000 automatic sample grinding &
polishing machine. (88) This machine is shown in the photo in Figure 24 below.
Figure 24 Buehler Phoenix 4000 sample grinding and polishing machine
34
Table 3 Planar Grinding and Polishing Variables
METHODS OF
ABRASION
TYPE OF
ABRASIVE
PAPER/CLOTH
SIZE/TYPE
OF
ABRASIVE
DIRECTION
PLATEN
SPEED
(RPM)
HEAD SPEED
(RPM)
PRESSURE PER
SAMPLE (Lbs)
CYCLE TIME
(MINUTES)
PLANAR
GRINDING
SiC PAPER P 240 GRIT CONTRA 200 120 5 UNTIL PLANE
PLANAR
GRINDING
SiC PAPER P 300 GRIT CONTRA 200 120 5 2 MINUTES
PLANAR
GRINDING
SiC PAPER P 600 GRIT CONTRA 200 120 5 2 MINUTES
PLANAR
GRINDING
SiC PAPER P 800 GRIT CONTRA 200 120 5 2 MINUTES
STAGE 1
POLISHING
ULTRAPAD
9 μm WATER
BASED
DIAMON
SOLUTION
COMPLIMENTARY 300 120 5 4 MINUTES
STAGE 2
POLISHING
NYLON or
TEXMET
3 μm WATER
BASED
DIAMON
SOLUTION
COMPLIMENTARY 300 120 5 4 MINUTES
FINAL
POLISHING
MICROCLOTH
1 μm WATER
BASED
DIAMON
SOLUTION
CONTRA 80 60 2.5 2 MINUTES
35
Chapter 4 Methods of Evaluation of Project Data
4.1 Macroscopic analysis
The first step in analysing the polished & etched samples was to view and evaluate the
microstructure under a low powered microscope. This allowed the evaluation of the weld
structure, the weld definition and the number of weld passes as well as their orientation.
Macroscopic examination also helped in locating and identifying any possible obvious
surface defects such as porosity, slag inclusions, lack of fusion etc. this facilitated closer
inspection of the samples. It is an accepted procedure to photograph each section of the
specimen at a macro level. The sample was photographed from the parent metal to the parent
metal/HAZ boundary, the HAZ, and the weldment itself. It was also advisable to perform this
procedure right across the sample because of the possibility of variation in the sample. In this
investigation, macroscopic examination was performed using a “Meiji” 7x-45x binocular
zoom microscope.
4.2 Microscopic analysis
Microscopic examination was carried out for many reasons, not least was to view and assess
the grain structure of the material from the photographic images taken. When it comes to
microscopic examination of metals and welded components it is standard practice to closely
examine the grain structure of the material to look for any imperfections or unusual patterns
of grain growth. For example, in some metals, a refined grain structure gives materials
desirable toughness properties. However with a refined grain structure for the same material,
this would reduce the ductility of the material.
4.3 Micro Hardness testing
Micro hardness testing was a procedure that was used in this project to evaluate the variations
in hardness across the specimens from the parent material through to the HAZ and the
weldment. Vickers Micro Hardness testing is an industry standard method for evaluating the
variations in hardness due to the carbon content of the selected materials which affects their
hardenability. When trying to ascertain the hardness variations of small samples using
multiple small indentations travelling from top to bottom and transversely across the sample,
this was the only viable method when trying to obtain more accurate refined figures.
Figure 25 Vickers Micro Hardness Testing Procedure (89)
36
4.4 Representing the micro hardness results graphically using Microsoft Excel
Once a series of figures had been obtained from the micro hardness tests and the distances of
the indentations in the sample relative to a reference point had been recorded, then those
values where plotted on a graph using Microsoft Excel. Once the graph displayed what was to
be expected from the figures then the rest of the hardness tests commenced. When all those
figures had been accurately compiled then they were also plotted on an Excel graph. This is
an example of a typical hardness profile for a material with hardness above 50 HRC. (90)
Graph 1 Example of Micro Hardness Profile of 0.4 % Carbon Steel (91)
4.5 Sample Table of Results for Vickers Micro Hardness Tests
The table below is a sample of the average hardness results obtained while conducting the
Vickers Micro Hardness tests. The complete test data is compiled within the appendices.
Table 4 Average Vickers Micro Hardness Values for the Test Samples
4.6 Determining the Yield Strength of the Weld specimens
The Vickers Hardness results obtained during the course of this investigation were used to
ascertain the yield strength of those weld specimens at different regions throughout the
materials. The yield strength of the weld specimens were calculated for different zones right
across the materials from the parent metal to the HAZ and the weldment itself.
MATERIAL JOINT TYPE WELDING PROCESS HV IN PARENT METAL HV IN HEAT AFFECTED ZONE HV IN WELD
MILDS STEEL BUTT MMA 135.133 165 154.6
MILDS STEEL BUTT TIG 146.1 179.55 182.7
API 5L CARBON PIPE BUTT MMA 176.25 189.1 162.35
API 5L CARBON PIPE BUTT TIG 156.675 193.5 175
EN8 MEDIUM CARBON STEEL BUTT MMA 202.45 145.75 227.433
EN8 MEDIUM CARBON STEEL BUTT TIG 176.85 169.85 481.75
01 TOOL STEEL (ANNEALED) BUTT MMA 184.5 399 230.5
01 TOOL STEEL (ANNEALED) BUTT TIG 184.5 312 207.5
TABLE OF AVERAGE VICKERS MICROHARDNESS VALUES ACROSS TEST SAMPLES
37
To calculate the yield strength of the weld specimens, the Vickers Micro Hardness values
were multiplied by 3. This is only applicable to carbon steel. This gave a valid value for the
yield strength. Yield strength is directly related to hardness, and as one would expect,
therefore as the hardness increases so too does the yield strength. An example of how this
was displayed graphically is shown in Graph 2 below. This is illustrated in greater detail in
the analysis chapter further on in this report. A typical yield strength value for mild steel that
has not been affected by heat energy from welding would be approximately 248 MPa (92).
Typical yield strength for API 5L would be 414 MPa (93). Typical yield strength for EN 8
would be 465 MPa (94). Typical yield strength for O1 tool steel would be 1500 MPa (95).
Graph 2 Yield Strength of MMA Welded Mild Steel
4.7 How was the Arc Energy and Heat Input of the welding processes determined?
The Arc Voltage of the welding processes was calculated using a multi-meter with its probes
connected to the Earth and the Work leads of the welding equipment. This was done for the
MMA and TIG welding processes. Using a piece of material that was marked to a
predetermined length for the start and finish of the weld (50 mm), a test weld was conducted
and the time taken to complete the weld was recorded with a stop watch. This was necessary
to determine the travel speed. Using the AE (Arc Energy) formula, values for both the MMA
and TIG welding processes were determined. Each welding process had an inherent
efficiency rating and this was factored into the calculation to determine the Heat Input. The
AE formula and the exact values obtained for both the MMA and TIG welding processes are
shown in the analysis section of the report.
4.8 Determining the variations in hardness in multi-pass welds from root of weld to
cap of weld
It was observed that the hardness of multi-pass welds change from the root weld into the hot
pass, and throughout the filler welds and into the final cap weld. It was observed that the
hardness increased nearer to the surface of the cap weld and the resulting microstructure was
quite different from the underlying microstructure. This is explained in the analysis section.
38
Chapter 5 Analysis of results
5.1 Analysing and interpreting images of weld specimen microstructure
In this section the resulting microstructure of the different materials and the processes used to
weld them were compared for similarity. Also the specimen microstructure was compared
from the welded samples, the heat treated samples, and the unprocessed control samples.
Mild steel microstructure comparison
Figure 26 Mild Steel Control Sample Microstructure 20 x 10 Magnification
Figure 27 Mild Steel Parent Metal MMA 20 x 10 Magnification
As can be clearly seen from the images above there was little or no difference between the
grain structure of the mild steel control sample in Figure 26 and the parent metal of the MMA
welded mild steel specimen in Figure 27. The proportions and distribution of both ferrite and
pearlite are very similar in both specimens. There was a very small amount of diffusion of
carbon from the ferrite into the cementite. There was a minute difference in average hardness
from 134.18 HV in the control sample to an average of 135.13 HV in the parent metal
sample.
Ferrite is the
white/grey grain
structure in the
image opposite
Pearlite is the
black substance
situated between
the ferrite grains
39
API 5L microstructure comparison
Figure 28 API 5L Control Sample 20 x 10 Magnification
Figure 29 API 5L Parent Metal 20 x 10 Magnification
The API 5L control sample in Figure 28 and the parent metal of the weld sample in Figure 29
appear slightly different. This is due to the fact that the parent metal, although a significant
distance away from the weld fusion zone, has had its temperature elevated to a point where it
minutely changed the material microstructure. The elevated temperature has allowed for the
diffusion of carbon atoms out of the ferrite and into the cementite. This diffusion of carbon
atoms into cementite raised the materials hardness in the parent metal section of the sample to
176.6 HV from the control sample average of 174 HV. The closer to the HAZ the higher the
hardness became. This, however, depended on a number of factors. Primarily it depended on
the carbon content of the material and its hardenability, but it also depended on the size of the
sample. Was there sufficient surrounding parent material for the resulting accumulation of
heat to dissipate into so that the material can retain its hardness or would the material become
in effect annealed due to the specimen becoming saturated with heat?
A darker ferritic
grain structure
due in part to
the higher
carbon content
and the higher
manganese
content which
gives the
ferritic grain
structure a dark
blue/brown tint
White/grey
grain structure
of ferrite more
prominent than
in previous
image.
Black pearlite
grain structure
more prominent
than in previous
image.
40
EN8 Medium carbon steel microstructure comparison
Figure 30 EN8 Medium Carbon Steel Control Sample 20 x 10 Magnification
Figure 31 EN8 Medium Carbon Steel Parent Metal 20 x 10 Magnification
There was a clear visual difference between the EN8 control sample in Figure 30 and the
EN8 parent metal sample in Figure 31. However, unlike the previous API 5L sample, the
hardness of the EN8 control sample exceeded that of the EN8 parent metal. The reason for
this was clear, unlike the previous mild steel plate samples and the API 5L pipe samples
which were of sufficient dimensions that would allow for the dissipation of accumulated heat.
The EN 8 samples were very small (40 mm wide in total) and this, in effect, was the cause of
the material becoming annealed. The average hardness value of the EN 8 control sample was
234.6 HV but surprisingly the EN 8 parent metal sample hardness value was 212.2 HV.
Instead of seeing a gradual increase in hardness across the parent metal and a sharp rise in
hardness when into the HAZ, the opposite occurred and the hardness once into the HAZ
dropped significantly. This happened in spite of the fact that the material contained 0.4 %
carbon that would allow the material in ideal circumstances to attain a maximum hardness of
approximately 58 HRC.
A darker
Martensitic
microstructure
mixed with
white Ferrite
Average Hardness = 234.6 HV
Average Hardness = 212.2 HV
Greater
proportion of
white Ferrite
grains visible
41
O1 Tool steel microstructure comparison
Figure 32 O1 Tool Steel Control Sample 20 x 10 Magnification
Figure 33 O1 Tool Steel Parent Metal 20 x 10 Magnification (Annealed)
The O1 tool steel control sample in Figure 32 showed a stark difference when compared to
the O1 tool steel parent metal sample in Figure 33. One reason for this difference was that the
parent metal belonged to a sample that was annealed post welding. Even after post weld heat
treatment to remove the brittleness from the material the parent metal MMA welded O1 tool
steel sample retained a typical hardness profile. The average hardness value of the O1 tool
steel control sample was 218.933 HV, whereas the parent metal sample hardness value (after
annealing) was 150 HV. But the hardness value steadily increased across the parent metal
sample and a sharp rise was observed in the HAZ and then a drop in hardness across the
weldment as would be typical. The annealed welded sample in Figure 33 displayed a
discoloured microstructure after undergoing heat treatment.
Average Hardness = 218.933 HV
Average Hardness = 150 HV
Annealed O1
Tool Steel
control sample
displays a dark
Martensitic like
structure
interspersed
with small
Ferrite clusters.
Discoloured
welded O1 Tool
Steel which was
annealed post
weld. The
image shows
discoloured
Ferrite.
42
5.2 Comparing the HAZ of the four steels
Figure 34 MMA Welded MildSteel HAZ 20 x 10 Figure 35 MMA Welded API 5L HAZ 20 x 10
Figure 36 MMA Welded EN8 HAZ 20 x 10 Figure 37 MMA Welded O1 Tool Steel HAZ 20 x 10
The HAZ images from Figure’s 34, 35, 36, and 37 display typical HAZ features for the
selected materials mild steel, API 5L, EN8, and O1 tool steel. The mild steel showed a
typically uniform distribution of ferrite and cementite. The API 5L shows a higher proportion
of cementite to ferrite. The EN8 hardness value in the HAZ was NOT what was expected. It
was expected that there would be a sharp rise in the HAZ value from the parent metal value.
This is due to the fact that the EN8 weld specimen was far too small to begin with. If the
weld specimen was of a sufficient size then the accumulated heat would have had adjacent
parent material where it could dissipate too. The resulting drop in hardness within the HAZ of
the EN8 sample was because the HAZ in effect became annealed. The MMA welded O1 tool
steel sample showed a typical HAZ for this particular material.
Average HAZ Hardness = 165 HV Average HAZ Hardness = 189.1 HV
Post Weld Annealed
Average HAZ Hardness = 159.97 HV Average HAZ Hardness = 399 HV
43
5.3 Analysing & interpreting macroscopic images of defective and defect free weld
specimens
Mild steel weld specimens
Figure 38 MMA Welded MildSteel (Defect Free) Figure 39 MMA Welded MildSteel (Defective)
Figure 40 TIG Welded Mild Steel (Defect Free) Figure 41 TIG Welded Mild Steel (Defective)
In Figure 38, the weaved capping run of the MMA welded mild steel specimen had a
distinctly different grain structure than the rest of the sample. Due to a lower heat input from
the MMA this led to a more localised normalising of the grain structure which gave a more
coarse appearance. Also the fact that the cap cooled at a quicker rate because it was exposed
to the atmosphere unlike the previous welds, gave a more coarse appearance to the cap. The
MMA welded mild steel specimen in Figure 39 contained multiple flaws due to inadequate
welding current. These flaws included slag inclusions, undercut, and no root penetration. The
TIG welded mild steel specimen in Figure 40 was defect free and displayed a more refined
grain structure due to a more generalized annealing because of the much higher heat input.
The TIG welded mild steel specimen in Figure 41 had defects that included porosity and lack
of sidewall fusion. These flaws were due to inadequate gas shielding and inadequate welding
current respectively.
Sound
inter pass
fusion,
sidewall
fusion,
and root
fusion.
Weld Root
Defective
weld with
multiple
flaws.
Sound
inter pass
fusion,
sidewall
fusion,
and root
fusion.
Defective
weld with
multiple
flaws.
Corrosion
HAZ
Multi pass
layering of
welds
Dendrites in weld cap
Undercut
on the cap
Slag Inclusion
Inter pass
lack of fusion
No root
penetration
Weld Root
No sidewall fusion
Porosity
Weld
Cap
44
API 5L Weld specimens
Figure 42 MMA Welded API 5L (Defect Free) Figure 43 MMA Welded API 5L (Defective)
Figure 44 TIG Welded API 5L (Defect Free) Figure 45 TIG Welded API 5L (Defective)
In Figure 42, the capping runs of the MMA welded API 5L specimen have a grain structure
that was also quite different than the previous welds. The dendrites are prominent in the
surface layer because upon cooling the capping runs were exposed to the atmosphere. In
Figure 43 the MMA welded API 5L had very obvious defects such as undercut, voids, and
slag inclusions. The undercut was caused by improper rod angle and the other defects were
caused by low welding current. The TIG welded API 5L specimen in Figure 44 shows a
defect free weld specimen. The TIG welded API 5L sample in Figure 45 shows a defective
weld with multiple weld defects such as voids, lack of sidewall fusion, and lack of
penetration. All these defects were caused by the welding current being set too low and using
improper welding technique.
Dendrites in cap
Sound
inter pass
fusion,
sidewall
fusion,
and root
fusion.
Defective
weld with
multiple
flaws.
Defective
weld with
multiple
flaws.
Sound
inter pass
fusion,
sidewall
fusion,
and root
fusion.
Root Weld
Undercut and
devoid of
weldment
Slag inclusion
Root Weld
HAZ
No sidewall
fusion and lack
of penetration
Void and
no sidewall
fusion
HAZ
45
EN8 Weld specimens
Figure 46 MMA Welded EN8 (Defect Free) Figure 47 MMA Welded EN8 (Defective)
Figure 48 TIG Welded EN8 (Defect Free) Figure 49 TIG Welded EN8 (Defective)
As can be seen from Figure 46, the MMA welded EN 8 specimen shows a perfectly defect
free sample. The weldment displays a mirror like finish after etching with a nitric acid
solution because 312 stainless was resistant to granular attack from the nitric acid. In Figure
47 the MMA welded EN 8 specimen displayed serious weld defects. Those defects included
slag inclusions and no sidewall fusion, both were caused by the welding current being set too
low. In Figure 48 the TIG welded EN 8 specimen was welded to a satisfactory standard,
however the cap weld was slightly excessive. In Figure 49 the TIG welded EN 8 specimen
shows serious weld defects such as insufficient sidewall fusion and a complete lack of root
penetration.
HAZ
Welded using 312
SS consumable.
Sound
inter pass
fusion,
sidewall
fusion,
and root
fusion.
Defective
weld with
multiple
flaws.
Slag inclusions and
no sidewall fusion
Sound
inter pass
fusion,
sidewall
fusion,
and root
fusion.
Defective
weld with
multiple
flaws.
Lack of
sidewall
fusion and
lack of root
penetration.
Welded
using 312
SS filler.
wire.
46
O1 Tool steel specimens
Figure 50 MMA Welded O1 Tool Steel (Defect Free) Figure 51 MMA Welded O1 Tool Steel (Defective)
Figure 52 TIG Welded O1 Tool Steel (Defect Free) Figure 53 TIG Welded O1 Tool Steel (Defective)
The MMA welded O1 tool steel specimen in Figure 50 was a defect free specimen. There
was a distinct visible difference in grain structure between the parent material and the HAZ.
The MMA welded O1 tool steel specimen in Figure 51 displayed serious flaws. What was
most evident was the major mid weld crack. There was also an insufficient depth of weld
filler material in the joint chamfer. The TIG welded O1 tool steel specimen in Figure 52 was
a visibly defect free weld specimen. The TIG welded O1 tool steel specimen in Figure 53 was
a defective weld specimen which displayed an identical major crack mid weldment just like
the MMA welded O1 tool steel specimen in Figure 51.
Sound
inter pass
fusion,
sidewall
fusion,
and root
fusion.
Defective
weld with
multiple
flaws.
Sound
inter pass
fusion,
sidewall
fusion,
and root
fusion.
Defective
weld with
multiple
flaws.
Welded using 312 SS
consumable.
HAZ
Major crack
in weldment
Insufficient
depth of
filler
material
HAZ
Welded using 312 SS
consumable.
Major
crack in
weldment
Crack
propagating
into
weldment
from the
parent metal
Annealed
Normalised
Welded at room
Temperature
Welded at
room
Temperature
47
5.4 Sample graphs of Vickers hardness plots
Graph 3 Vickers Micro Hardness plot of Mild Steel MMA Graph 4 Vickers Micro Hardness plot of EN8 MMA
Graph 5 Vickers Micro Hardness plot of API 5L MMA Graph 6 Vickers Hardness plot of 01 Tool SteelMMA
The data plotted in Graphs 3,4,5, and 6 represent the Micro Hardness data plotted of all four project materials, Mild Steel, API 5L, EN 8, and O1
Tool Steel. The data shows the fluctuation in hardness across the three zones of interest from Parent Metal to Heat Affected Zone (HAZ) and the
Weld itself.
48
5.5 The formation and propagation of cracks in welded specimens
Figure 54 MMA Welded O1 Tool Steel Specimen with Hydrogen Infused Crack
In some of the tool steel specimens, which were heat treated pre-weld and post weld, severe
cracks appeared in the parent metal and also the weldment itself. This was due to this
materials’ poor weldability and the possibility of diffusible Hydrogen being contained within
the cooling weldment. Also the conflicting thermal expansion rates of the parent material and
the welding filler material was a source of concern when trying to minimise the potential for
the initiation of cracks and their possible propagation to catastrophic failure. The result of not
following rigorous heat treatment procedures regarding the correct method for welding O1
Tool Steel is clearly illustrated in Figures 51 and 53 on page 46.
Using the carbon equivalent formula (CEIIW) --- 𝑪𝑬 𝑰𝑰𝑾 = 𝑪 +
𝑴𝒏
𝟔
+
𝑪𝒓+𝑴𝒐+𝑽
𝟓
+
𝑵𝒊+𝑪𝒖
𝟏𝟓
The weldability of the material will be determined based on the chemical composition of 01
tool steel. (96)
𝑪𝑬 𝑰𝑰𝑾 = 𝟎. 𝟗𝟓 +
𝟏. 𝟐𝟓
𝟔
+
𝑪𝒓 + 𝑴𝒐 + 𝑽
𝟓
+
𝑵𝒊 + 𝑪𝒖
𝟏𝟓
The carbon equivalent of the O1 tool steel is ≈ 1.158. This far exceeds the accepted limit for
good weldability of 0.4.
Coefficients of thermal expansion for O1 tool steel and 312 stainless steel filler material
Figure 55 COTE For O1 Tool Steel (97) Figure 56 COTE For 312 StainlessSteel (98)
Weld Nugget
Coarse grain structure at the
Initiation point of Hydrogen
infused crack at the toes of
the weld
Refined grain
structure at the
point where the
crack rapidly
propagates
MMA Welded 01 Tool Steel Specimen
49
Chapter 6 Discussion
6.1 Differences in Arc Energy and Heat Input of MMA and TIG
Differences in arc energy and heat input between arc welding processes affect the resulting
material properties due to the amount of heat energy imparted to the material. In this project
there were two arc welding processes used, MMA and TIG. Arc Energy and Heat Input are
both ways of measuring the amount of heat energy imparted to the material, however heat
input takes account of the process efficiency in the calculation. The value is expressed in
Kilojoules per unit length of welded material, in this case it is kJ/mm. The test piece was
welded with a single pass weld over a measured distance of 50 mm for both processes. The
Arc Energy and Heat Input equations are expressed mathematically as follows:
Arc Energy (AE) =
( 𝟔𝟎) 𝒙( 𝑽) 𝒙(𝑰)
( 𝟏𝟎𝟎𝟎) 𝒙(𝒗)
Heat Input (HI) = ηAE
Where V = Arc Voltage (Volts)
I = Welding Current (Amps)
v = Travel Speed (mm/Minute)
η = Process Efficiency
Table 5 Table of Results for Arc Energy and Heat Input
The results for Heat Input left no doubt about the significant variation in Heat Input between
MMA and TIG. TIG imparts a larger quantity of heat energy per unit length into the material.
As shown in Figures 57 and 58 on page 50, there is a significant difference in the
microstructure between the TIG weld specimen and the MMA welded specimen. Strangely
the TIG welded specimen shows an enlarged and coarse grain structure within the HAZ but a
higher HV value. The TIG welded specimen has a large Ferrite grain structure containing fine
pearlite at the grain boundaries. The MMA welded specimen shows a smaller proportion of
Ferrite surrounded by a coarse Pearlite structure, it had a lower HV value. This is reflected in
the Micro Hardness values for both these specimens. The peak Vickers Hardness in the HAZ
for the TIG welded specimen was 159.6 HV, whereas the MMA welded specimen had a
Vickers Hardness of 149.5 HV. The dip in the HAZ Vickers Hardness values for both
specimens was not what was expected. This was due, in part, to the inadequate size of the
samples which were far too small. The specimens effectively became annealed in the HAZ
because of the build-up of heat. With a high heat input value this leads to a much slower
cooling rate which promotes grain growth. Also excessive Ferrite grain growth in the HAZ of
the EN 8 TIG welded sample is due partly to the higher chromium content of the TIG filler
wire as opposed to the MMA welding rods even though both were 312 stainless. TIG filler
chromium content was 32 % (81) and MMA rod content was 29% (80).
PROCESS ARCV(Volts) WELDINGI(Amps) EFFICIENCY(η) WELDTESTL(mm) TIME(Seconds) TRAVELSPEED(mm/min) AE(kJ/mm) HI(kJ/mm) %DIFFERENCE
MMA 19 75 0.8 50 17 176.471 0.4845 0.3876
TIG 75 120 0.6 50 22 136.364 3.96 2.376
TABLEOFRESULTSFORARCENERGYANDHEATINPUT
513.00%
50
Images of EN 8 Medium Carbon Steel welded with MMA and TIG
Figure 57 TIG Welded EN8 HAZ (20x10 Magnification) Figure 58 MMA Welded EN8 HAZ (20x10 Magnification)
6.2 The effect of multiple weld passes on the mechanical properties
The resulting microstructure and mechanical properties that are created due to the effect of
multi-pass welds on a material differ significantly from single pass welds. Because the initial
weld is not exposed to the cooling ambient air for any length of time, as would be the case
with a single pass weld, its final mechanical properties are quite different. The initial heat
energy required, to raise the material to a point where the material becomes molten within the
weld fusion zone, decreases with successive weld passes. Once the initial weld pass has been
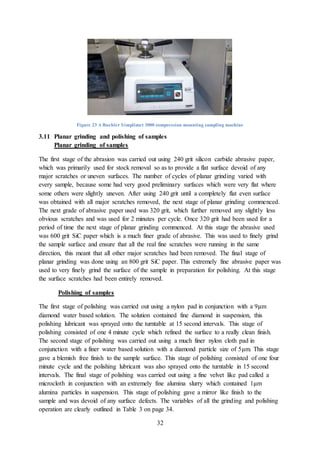
completed then the material temperature has greatly increased. The successive weld passes
can be carried out with a higher travel speed while using the same welding current, this
means that a lower heat input is imparted to the material at the same time ensuring sound
inter-pass fusion. By increasingly lowering the heat input into the material this aids in
limiting grain growth.
The re-heating of the previous weld metal deposit by subsequent weld passes acts to
normalise the previous weld microstructure. This ensures that any residual stresses within the
material are reduced. The nature of multi-pass welds guarantee a level of preheat into the
material and, upon completion of the welding operation, slows the cooling rate down and
greatly reduces the likelihood of the formation of cracks within the welds and the parent
material. When the final weld is completed, whether it is a multi-pass fillet weld or a multi-
pass butt weld, its microstructure differs significantly from the previous welds. This is
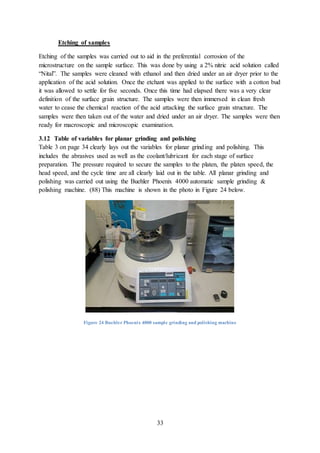
because the final weld is exposed to the cool ambient air, unlike the previous welds. This
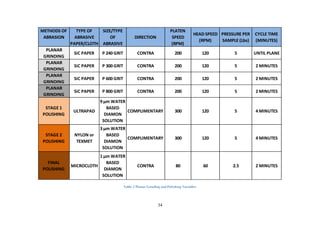
ensures that the final welds have a different cooling rate than the underlying welds.
Graphically the microstructure appears quite different to the underlying microstructure of the
previous welds. What can be clearly seen in multi-pass welds are the lines where the welds
have been layered on top of each other. Also on the final welds, just below the surface, the
dendrites can clearly be seen. In the image shown in Figure 59, the Vickers Hardness is
higher in the surface cap weld than in the root and subsequent welds. This is displayed
graphically in Graph 7. All Vickers Micro Hardness values were taken in the centre of the
weld from root to cap.
Less
Prominent
Ferrite
structure
than
would be
seen in
mild steel
Martensitic
Like
structure
containing
small
amounts of
Ferrite
51
Figure 59 MMA Mild Steel Butt Weld
Graph 7 Graph Displaying Difference in Vickers Micro Hardness from Root to Cap
6.3 Yield strength of weld specimens
The yield strength of a material is closely related to the hardness of the material. With the
increase in hardness comes an increase in yield strength, depending on carbon content. If a
plain carbon steel (0.15% - 0.85%), once quenched, is tempered at a temperature not
exceeding 250o C then it will attain maximum hardness. At a tempering temperature not
exceeding 350o C then it will attain maximum yield strength. (99) The yield strength of a
plain carbon steel is calculated simply by multiplying the Vickers Hardness value by 3.17
(100) (only applicable to carbon steel). The yield strength of the weld specimens used in this
project vary due to the difference in carbon content. The carbon content of the specimens for
this project ranges from 0.15% C - 0.95% C. The variation in yield strength of the different
materials across zones from parent metal into the HAZ and into the weldment, are illustrated
in Graph 8. As can be seen from the graph, the higher carbon containing materials, gave a
much higher yield strength due to carbon content. The variation in yield strength of welded
carbon steels and un-welded carbon steels is an important factor to consider when designing
welded components. It would need to be determined whether or not if the brittle nature of
very hard HAZ’s would mean that higher yield strength in those areas was actually a serious
design fault. The results of such faults are clearly illustrated in Figures 51 and 53 on page 46.
Dendrites
Weld Inter-pass
layers
52
Graph of Yield Strength of Weld Specimens
Graph 8 Graph of Weld Specimen Yield Strengths
6.4 Hardenability
The chemical composition of a material and the alloying elements within that material
determine its ability to from Martensite, this is called “Hardenability”. For different steels
there is a particular relationship between the mechanical properties and the cooling rate of
that material. Hardenability is not hardness. Hardness is the ability of a material to resist
indentation whereas hardenability is a measure of how much that hardness decreases as the
distance away from the quenched surface increases. As the distance away from the quenched
surface increases, the cooling rate is slower and therefore the ability of the material to form
Martensite diminishes. This will give a lower Rockwell Hardness value than the quenched
part.
Figure 60 Time Temperature Cooling Curve for SAE 1040 (EN 8)
53
Images of SAE 1040 (EN 8) After Undergoing Different Heat Treatments
Figure 61 AnnealedEN 8 (0.4 % C) @ 20x10 Mag. Figure 62 NormalisedEN 8 (0.4 % C) @ 20x10 Mag.
Figure 63 QuenchedEN 8 (0.4 % C) @ 20x10 Mag. Figure 64 Tempered EN 8 (0.4 % C) @ 20x10 Mag.
Hardenability of Heat Treated Samples
Using the TTT diagram in Figure 60, it can be seen that SAE 1040 when quenched will attain
up to 57 HRC if cooled within 10 seconds, cooling at a rate of 634o C per second. The HRC
value for the quenched sample was 47 HRC, this was cooled in under 10 seconds so therefore
the material must have had a carbon content less than 0.4 %. The HRB value for the annealed
sample is76.85 HRB, which according to the TTT diagram will cool at a rate of
approximately 1o F/minute. It will take approximately 27.78 hours to cool completely. The
normalized sample gave a hardness value of 83.85 HRB. The tempered sample gave a
Rockwell hardness value of 37 HRC, which would mean that it cooled in approx. 25 seconds.
MATERIAL HEAT TREATMENT VICKERS HARDNESS (HV) ROCKWELL SCALE ROCKWELL HARDNESS (HR)
SAE 1040 (EN 8) ANNEALED 143.4 HRB 76.85
SAE 1040 (EN 8) NORMALISED 164.4 HRB 83.85
SAE 1040 (EN 8) QUENCHED 477.867 HRC 47
SAE 1040 (EN 8) TEMPERED 360.133 HRC 37
TABLE OF VICKERS TO ROCKWELL CONVERSIONS
Enlarged coarse
grain structure
due to
prolonged
cooling time
Less coarse
grain structure
due to faster
cooling in
ambient air
Needle like
shape of
Martensite
Fine Grain
Structure of
Tempered
Martensite
54
6.5 Strengthening by Grain Size Reduction
When a material is held at an elevated temperature, above the recrystallization temperature,
for a period of time beyond the time required for full recrystallization then grain growth
occurs. Diffusion of atoms occur across the grain boundaries more easily because of the
added energy within the system due to the higher temperature experienced by the material.
Larger grains, having less overall grain boundary surface area per unit volume than smaller
grains, diffuse atoms at a lesser rate than the smaller grains. This allows for the grains to
grow larger. Grain size has a significant effect on the strength and toughness properties of a
material. There is a direct correlation between the strength and hardness of carbon steel and
the grain size within the microstructure. Boundaries between grains inhibit the movement of
dislocations and any slip that may possibly occur. Grains are positioned at different
orientations relative to each other and because slip planes are not trans-granular, meaning slip
planes cannot travel across grains, the smaller the grain size then the smaller distance that the
atoms can move along that slip plane. The smaller grains then greatly improve the yield
strength of the material. The size of the finished grain structure is dependent upon carbon
content and the rate at which the material is cooled from the liquid phase.
Figure 65 AnnealedSAE 1040 (EN 8) @ 20X10 Mag. Figure 66 QuenchedSAE1040 (EN 8) @ 20x10 Mag.
Figure 67 O1 Tool SteelParent Metal @ 20x10 Mag. Figure 68 O1 Tool SteelHAZ @ 20x10 Mag.
143.40 HV 477.867 HV
188.5 HV 543 HV
Larger Grain
Structure
Refined Needle Like
Grain Structure
Larger Grain
Structure
Refined Smaller
Grain Structure
430.2 MPa 1433.601 MPa
565.5 MPa 1629 MPa
55
6.6 Phase Transformations in Weld Specimens
Figure 69 Iron Carbon Phase Diagram (101)
Figure 70 MMA Welded MildSteel Microstructure (10x Mag.)
Solidified Weld
Solid – Liquid Transition Zone
RecrystallizedZone
PartiallyTransformedZone
Unaffected
Parent Metal
TemperedZone
Grain Growth Zone
56
Mechanical Properties of Weld Specimens during and after Phase Transformation
The mechanical properties of a welded joint are related to its microstructure and the number
of welding cycles that it has undergone. The number of welding cycles i.e. the number of
weld passes performed to fill out a butt weld or a fillet weld, have a direct impact on the final
mechanical properties of the weldment and the surrounding HAZ and parent material.
However there are many other factors that determine what kind of microstructure and
mechanical properties will be attained on completion of the welding operation. The welding
parameters such as arc voltage, welding current, travel speed, and welding process all
influence the final microstructure and mechanical properties of the finished welded joint.
Upon initiation of the welding arc and once the weld pool is moving, the semi solid cooling
weldment left in its wake forms a cast type microstructure which starts at the edges of the
weld pool. Grains start to form and grow from the weld pool edges towards the centre of the
weld. The size of the grains formed in the weld depend on the rate of cooling of the weld
metal and its surrounding parent material. The HAZ, the zone between the fusion zone and
the parent material forms a different kind of microstructure. The width of the HAZ is
determined by the temperature during the welding operation. Once the temperature exceeds
550o C (102), which it will during welding, the microstructure of the HAZ will change. As
shown in Figure 69, only tempering of the HAZ happens below the Eutectoid temperature of
723o C. Above the Eutectoid point there is partial phase transformation to austenite. Above
the recrystallization temperature of 912o C within the fully austenite region, there is no
significant grain growth until all carbides present have been dissolved. At the other side of
the HAZ where it interfaces with the weld fusion zone the carbides have been fully dissolved,
this allows the grain structure to grow and have a more coarse appearance and therefore is
softer relative to the HAZ. Moving outwards from the weldment and the HAZ towards the
zone of the parent metal a point is reached where the grain structure of the material is no
longer affected.
6.7 Heat Treatment of Carbon Steels
Heat treatment of carbon steels is a way of changing the microstructure to attain the desirable
mechanical properties required. Depending on what application the material will be used for
and what service conditions it will experience will dictate what heat treatment, if any, will be
necessary for the material. When carbon steels are heat treated they undergo phase
transformations which alter the grain structure. If a material needs to machined or welded
then it would be advisable to “Anneal” the material first. If a material needs increased
toughness after being work hardened by rolling or folding then it should be “Normalized”. If
a material needs increased hardness then the material should be quenched in an appropriate
medium. If a material has been quenched and if it is to be used in service then it must be
tempered to relieve the stress and embrittlement and by virtue increasing its strength. The
various heat treatments carried out on the specimens relating to this project are as follows:
 Annealing
 Normalizing
 Quenching
 Tempering
57
Images of Heat Treated Samples SAE 1040 (EN 8)
Figure 71 AnnealedSAE 1040 (50 x 10 Mag.) Figure 72 NormalizedSAE1040 (50 x 10 Mag.)
Figure 73 QuenchedSAE1040 (50 x 10 Mag.) Figure 74 Tempered SAE 1040 (50 x 10 Mag.)
As is clearly shown in Figures 71, 72, 73, and 74, the different heat treatment processes have
a significant effect on the microstructure of the medium carbon steel. When a material is
annealed it allows the material to cool at a very slow rate which promotes grain growth which
is clearly shown in Figure 71. In Figure 72 there is a slightly smaller grain structure which is
brought about because the material is cooled at a much quicker rate in the ambient air, thus
increasing toughness and strength by normalizing. In Figure 73 there is significantly visible
reduction in grain size because the material has been quenched and thus locking the carbon in
solution because of the rapid rate of cooling. This forms Martensite and the structure is
extremely hard, but brittle. In Figure 74 the grain structure is slightly less “needle like”
because it has been tempered. This heat treatment procedure will relive the material of
internal stress at the expense of a proportion of its hardness but in return its strength has been
greatly increased.
Very Large Grain Structure Slightly Smaller
Grain Structure
Sharp Needle Like Grain
Structure
More Refined Tempered
Grain Structure
58
6.8 Conclusions
Upon reflection there are areas of concerns and they should be addressed so that if similar
work was to be carried out in the future, these areas of concern could be avoided.
Weld Specimen Materials
The materials used in this project were those near to hand and the best that was available.
After attempts at sourcing medium carbon steel (EN 8) in the size that was needed had failed,
a compromise was made to include the use of this material in the project. EN 8 of a
dimension that was far from ideal was used, and because of its inadequate size the Vickers
Hardness values that were recorded were the reverse of what was expected. This is purely
because the material was far too small and the material properties reflected this fact. If
carrying out a similar project in the future it would be advantageous to use materials of equal
dimensions (width. length, thickness) for all four steel used, so as to help limit any factors
that have the possibility to produce unexpected results.
Welding Consumables
The welding consumables used were not all new consumables but were prepared, as much as
was possible, according to the ASME IX code of practice. The consumables, (low hydrogen)
need to be stored and preheated in accordance with the above code prior to any welding being
carried out. But due to the cost of these consumables, older consumables (although sealed)
were used to reduce cost. This may have introduced diffusible Hydrogen into the molten weld
pool which can cause Hydrogen infused cracking. Also there is a possibility that this may
have had an adverse effect on the x-ray quality of those welds. But since there is no
possibility of submitting the welds to an x-ray, there is no way of being sure either way.
Planar Grinding and Polishing Procedure
After extensive planar grinding and polishing of more than two dozen samples, doubts have
been raised as to the validity of the procedure that was followed. The procedure concerned all
the variables of this operation. For some of the samples, the mild steel, the API 5L, and the
medium carbon EN 8 there were no significant concerns but the O1 tool steel samples did not
yield the planar surface that was expected when the advised Buehler procedure was followed.
It took an unusually long time for stock removal to remove all scratches and when it was
suspected that the surface of the O1 tool steel was ready to move to a finer grade of abrasive,
when commenced it had the adverse effect and introduced new scratches to the specimens.
59
Yield Strength of welded carbon steel Vs yield strength un-welded carbon steel
The yield strength of the lower carbon steels (mild steel, API 5L) after welding have a HAZ
hardness that does not represent a problem that would lead to brittle fracture. There is no
significant fluctuation in hardness from the parent metal to the HAZ and the weldment. The
exceptionally high carbon O1 tool steel, however, shows significant variations between
hardness in the parent metal into the HAZ and the weld. There is a significant rise in hardness
in the HAZ of O1 tool steel and this has led to brittle fracture in some O1 specimens which
displayed high yield strength figures as shown in Figures 51 & 53 on page 46. All O1 tool
steel specimens, except the annealed specimens exceeded the typical un-welded yield
strength of O1 tool steel and ultimately failed by cracking. The typical yield strength for EN8
was exceeded, and in the case of the TIG welded specimen, it was exceeded by more than 3
times the yield strength in the HAZ for the un-welded EN 8. However none of the EN 8
specimens failed. None of the mild steel specimens or the API 5L specimens failed and they
were all within acceptable design limits. The complete table of Vickers hardness values and
yield strength values are in the Table 6 on page 79.
Multi Pass Weld Test Pieces Vs Single Weld Test Pieces
When the microscopic examination of the weld specimens was commenced it was noticed
that there was a layered type of microstructure which sometimes made it difficult to clearly
define zone interfaces. When the Vickers Micro Hardness testing commenced it was
presenting a very confusing looking microstructure that made it difficult to clearly locate
regions of interest for hardness testing. It became very difficult to accurately pinpoint a
suitable location for the diamond indenter. Upon reflection it would be advisable to use single
pass butt welds on thinner plates or single pass fillet welds, using a wider variety of materials
and processes. This would allow for a broader comparison of not just materials but of
welding processes also.
Arc Energy and Heat Input of MMA Vs TIG
It was concluded that the TIG welding process imparted a far greater amount of heat energy
into the material during the welding process than the MMA process does. This high energy
input meant that there was a much slower cooling rate for the samples welded with the TIG
welding process. This resulted in excessive grain growth in some samples, namely Figure 57
on page 50.
The need for using the Carbon Equivalent Formula
The carbon equivalent formula is an extremely important source of critical information which
was used to determine the weldability of the project materials. It was demonstrated that
without proper adherence to recommended heat treatment procedures, any carbon steels with
a carbon equivalent above 0.4 would produce undesirable mechanical properties when
welded.
60
The anomaly of varied hardness values in the EN 8 weld specimens
The anomaly of obtaining an unexpected decrease in hardness in the HAZ of both the TIG
welded and the MMA welded specimens, coupled with unexpected corresponding
microstructure for the same zones of both specimens was difficult to explain. It would have
been expected that as the hardness increased, the corresponding grain structure for the TIG
welded EN 8 specimen would have been more refined rather than the coarse grain structure
that was obtained. The finer grain structure that was obtained from the MMA welded EN 8
specimen was what was expected but the corresponding hardness value was lower than that
for the coarser grain structure of the TIG welded EN 8 specimen. The only conclusion that
can be drawn from the relatively coarse Ferrite microstructure of the TIG welded EN 8, as
opposed to the finer microstructure of the MMA welded EN 8, is the fact that the TIG filler
wire (312 stainless) contains 32% Chromium which at higher temperatures promotes the
growth of Ferrite. The ESAB MMA welding rods however, although also 312 stainless, but
only containing 29% Chromium could be a factor for the disparity in hardness value and
microstructure grain size.
EN 8 Microstructure for MMA & TIG with corresponding graphs
Figure 75 HAZ of EN 8 (20 x 10 Magnification) Graph 8 Hardness Profile across EN 8 Weld Specimen
Figure 76 HAZ of EN 8 (20 x 10 Magnification) Graph 9 Hardness Profile across EN 8 Weld Specimens
HAZ Hardness = 159.6 HV
TIG Coarse Grain Structure
MMA Finer Grain Structure
HAZ Hardness = 149.5 HV
61
Chapter 7 APPENDICES
Graph 10 Vickers Micro Hardness For Mild Steel (MMA)
Graph 11 Vickers Micro Hardness For Mild Steel (TIG)
Graph 12 Vickers Micro Hardness For EN 8 (MMA)
62
Graph 13 Vickers Micro Hardness For EN 8 (TIG)
Graph 14 Vickers Micro Hardness For API 5L (MMA)
Graph 15 Vickers Micro Hardness For API 5L (TIG)
63
Graph 16 Vickers Micro Hardness For O1 Tool Steel ANNEALED (MMA)
Graph 17 Vickers Micro Hardness For O1 Tool Steel ANNEALED (TIG)
Graph 18 Vickers Micro Hardness For O1 Tool Steel NORMALISED (MMA)
64
Graph 19 Vickers Micro Hardness For O1 Tool Steel NORMALISED (TIG)
Graph 20 Vickers Micro Hardness For O1 Tool Steel ROOM TEMPERATURE (MMA)
Graph 21 Vickers Micro Hardness For O1 Tool Steel ROOM TEMPERATURE (TIG)
65
7.1 Graph of Difference in Vickers Micro Hardness From Root To Cap
Graph 22 Difference in Vickers Micro Hardness From Root To Cap
7.2 Graph of Differences in Yield Strength of All Weld Specimens
Graph 23 Graph of Yield Strengths of All Weld Specimens
66
7.3 Table of Vickers Hardness values and Yield Strengths
Table 6 Table of Vickers Hardness Values and Corresponding Yield Strengths
MATERIAL CARBONCONTENT(%) WELDPROCESS AVERAGEHV(PM) AVERAGEHV(HAZ) AVERAGEHV(WELD) AVERAGEYIELDMPa(PM) AVERAGEYIELDMPa(HAZ) AVERAGEYIELDMPa(WELD)
MILDSTEEL 0.15 MMA 135.133 165 154.6 428.37161 523.05 490.082
MILDSTEEL 0.15 TIG 146.1 179.55 182.7 463.137 569.1735 579.159
API5L 0.25 MMA 177.867 193.1 162.35 563.83839 612.127 514.6495
API5L 0.25 TIG 152.4 179.8 192.8 483.108 569.966 611.176
EN8 0.4 MMA 207.133 159.967 227.433 656.61161 507.09539 720.96261
EN8 0.4 TIG 176.85 169.85 481.75 560.6145 538.4245 1527.1475
O1TOOLSTEEL 0.9MMANORMALISED MMA 188.5 543 236.5 597.545 1721.31 749.705
O1TOOLSTEEL 0.9TIGNORMALISED TIG 465.5 602 218 1475.635 1908.34 691.06
O1TOOLSTEEL 0.9MMAANNEALED MMA 184.5 399 230.5 584.865 1264.83 730.685
O1TOOLSTEEL 0.9TIGANNEALED TIG 312 423 207.5 989.04 1340.91 657.775
O1TOOLSTEEL 0.9MMAROOMTEMP. MMA 220 594 226.5 697.4 1882.98 718.005
O1TOOLSTEEL 0.9TIGROOMTEMP. TIG 513 538 227.5 1626.21 1705.46 721.175
TABLEOFCONVERSIONSFROMVICKERSHARDNESSTOYIELDSTRENGTH
67
Bibliography
1. http://www.twi-global.com/contact/find-us/twi-cambridge/. http://www.twi-global.com/.
[Online] 4th October 2015.
2. http://www.aws.org/. http://www.aws.org/. [Online] 4th October 2015.
3. http://www.jflf.org/. http://www.jflf.org/. [Online] 4th October 2015.
4. https://www.asme.org/. https://www.asme.org/. [Online] 4th October 2015.
5. http://www.asminternational.org/home. http://www.asminternational.org/home. [Online]
4th October 2015.
6. Bolton, W. Newnes Engineering Materials Pocket Book (Third Edition). Oxford : Newnes,
2000. 0750649747.
7. http://www.kvsteel.co.uk/index.html. www.kvsteel.co.uk. [Online] KV Steel . [Cited: 10th
April 2016.]
8. ASM Handbook - Arlan O. Benscoter, Lehigh University - Bruce L. Bramfitt
International Steel Group. Metallography amd Microstructures of Low-Carbon and Coated
Steels. Ohio : ASM International, 2004. 0-87170-706-3.
9. Introduction to Steels and Cast Irons. Ohio : ASM International, 2002.
10. Shah, KP. The Hnadbook of Mechanical Maintenance.
11. Callister, William D. Materials Science and Engineering, An Introduction - Sixth Edition
- Page 279. New York : John Wiley & Sons Inc., 2003. 0-471-22471-5.
12. http://www.eaglesteel.com/download/techdocs/Carbon_Steel_Grades.pdf.
www.eaglesteel.com. [Online] Eagle Steel, 22nd 0ctober 2015. [Cited: 22nd October 2015.]
13. http://www.pearson-studium.de/books/3827370597/cd01/Gallery/Images/OM.htm.
http://www.pearson-studium.de. [Online] [Cited: 4th November 2015.]
14. Callister, William D. Material Science and Engineering - An Introduction - Sixth Edition
- Page 281. Ohio : John Wiley & Sons Inc., 2003. 0-471-22471-5.
15. Shah, KP. The Hnadbook of Mechanical Maintenance.
16. Callister, William D. Materials Science and Engineering - An Introduction - Sixth
Edition - Page 277. Ohio : John Wiley & Sons Inc., 2003. 0-471-22471-5.
17. Free, Miles. http://pmpaspeakingofprecision.com/2009/11/24/5-ways-fine-austenitic-
grain-size-affects-your-machine-shop/. http://pmpaspeakingofprecision.com/. [Online]
Precision Machined Products Association. [Cited: 29th January 2016.]
68
18. http://steel.keytometals.com/Articles/Art127.htm. keytometals.com. [Online] 1999-2010.
[Cited: 22nd October 2015.]
19. Shah, KP. The Handbook of Mecahanical Maintenance.
20. Gas Tungsten Arc Welding. Cleveland, Ohio : The James F. Lincoln Arc Welding
Foundation, 2004. 0-937390-00-3.
21. The Procedure Handbook of Arc Welding. Clevelaand Ohio : The Lincoln Electric
Company, 1995.
22. http://www.twitraining.com/home/course-schedule/welder-training-and-qualification.
http://www.twitraining.com/. [Online] TWI. [Cited: 4th November 2015.]
23. http://www.lr.org/en/_images/213-35590_Inspection_-_Welding_Certification_Service_-
_Weld_Certificate_UK.pdf. http://www.lr.org/en/. [Online] Lloyds Register of Shipping.
[Cited: 4th November 2015.]
24. http://www.aws.org/certification/detail/certified-welder-program. http://www.aws.org.
[Online] American Welding Society. [Cited: 4th November 2015.]
25. https://www.asme.org/products/courses/overview-welding-under-section-ix.
https://www.asme.org. [Online] American Society of Mechanical Enigneers. [Cited: 4th
November 2015.]
26. http://www.weldersuniverse.com/welding_beads.html. http://www.weldersuniverse.com.
[Online] Welders Universe, 2012-2015. [Cited: 4th November 2015.]
27. http://www.weldingdata.com/stringerorweave.htm. http://www.weldingdata.com.
[Online] Welding Data . [Cited: 4th November 2015.]
28. http://www.twi-global.com/technical-knowledge/job-knowledge/the-manual-metal-arc-
process-mma-welding-002/. http://www.twi-global.com/. [Online] The Welding Institute.
[Cited: 4th November 2015.]
29. http://www.twi-global.com/technical-knowledge/job-knowledge/tungsten-inert-gas-tig-
or-gta-welding-006/. http://www.twi-global.com/. [Online] The Welding Institute . [Cited: 4th
November 2015.]
30. AISI Austenitic Stainless Steel Grades. [book auth.] The Lincoln Electric Company. The
Procedure Handbook of Arc Welding. Cleveland Ohio : The Lincoln Electric Company,
1995.
31. http://www.engineersedge.com/tool_steel.htm. http://www.engineersedge.com. [Online]
2000 - 2015. [Cited: 5th November 2015.]
32. Dieter, George E. Mechanical Metallurgy, Chapter 6, Subsection 15, Page 233. New
York London Tokyo : McGraw-Hill, 1986. ISBN 0-07-016893-8.
69
33. http://www.metlabheattreat.com/metal-hardening-metal-quenching-metal-tempering.html.
http://www.metlabheattreat.com/. [Online] MetLab. [Cited: 6th November 2015.]
34. http://www.twi-global.com/technical-knowledge/job-knowledge/welding-procedure-039/.
http://www.twi-global.com/. [Online] The Welding Institute. [Cited: 6th November 2015.]
35. Davies, A.C. The Science and Practice of Welding Volume 2. Cambridge London New
York : Cambridge University Press, 1986. ISBN 0 521 27840 6.
36. McAllister, E.W. Pipline Rules of Thumb Handbook. New York Oxford Paris : Elsevier,
2005. ISBN 0750678526.
37. Buehler Handbook For Buehler Simplimet 3000 Automatic Mounting Press. Illinois :
Buehler, 2000.
38. http://www.engineershandbook.com/Materials/phenolics.htm.
http://www.engineershandbook.com. [Online] 2004 - 2006. [Cited: 6th November 2015.]
39. Application Guide For Compressive Mounting. Lake Bluff Illinois : Buehler, 2013.
40. http://www.mitar.sk/prospekty/phoenix4000.pdf. http://www.mitar.sk. [Online] 2000.
[Cited: 6th November 2015.]
41. http://www.labtesting.com/services/materials-testing/metallurgical-testing/sample-
preparation/. http://www.labtesting.com/. [Online] Lab Testing. [Cited: 6th November 2015.]
42. Callister, William D. Materials Science And Engineering - An Introduction -
Microscopic Examination - Page 81. Utah : John Wiley & Sons, Inc., 2003. ISBN 0-471-
22471-5.
43. Dissemination of IT for the Promotion of Materials Science (DoITPoMS). Cambridge :
University of Cambridge, 2004 - 2015.
44. Callister, William D. Materials Science and Engineering - An Introduction - Page 138 -
Knoop and Vickers Micro Hardness Tests. Utah : John Wiley & Sons Inc., 2003. ISBN 0-
471-22471-5.
45. H.W. Hayden, W.G. Moffatt, J. Wulff. The Structure And Properties Of Materials,
Volume 3 - Mechanical Behaviour. New York : John Wiley & Sons Inc., 1965.
46. Callister, William D. Materials Science And Engineering - An Introduction - Heat
Treatment of Steels - Page 361. Utah : John Wiley & Sons, Inc., 2003. ISBN 0-471-22471-5.
47. Influence of Welding Method on Microstructural Creation of Welded Joints. Čičo P.,
Kalincová D., Kotus M.,. Special Issue - S50-S56, Zvolen - Slovakia : Czech Agriculture
Journals, 2011, Vol. 57.
70
48. http://www.vuz.sk/public/files/english/production/Covered_Electrodes.pdf.
http://www.vuz.sk. [Online] VUZ Welding Consumable Manufacturers. [Cited: 7th November
2015.]
49. http://www.lincolnelectric.com/en-
us/consumables/Pages/product.aspx?product=Products_Consumable_StickElectrodes-
MildandLowAlloySteels-Excalibur-Excalibur7018MR(LincolnElectric).
http://www.lincolnelectric.com/. [Online] Lincoln Electric Arc Welding Company. [Cited:
7th November 2015.]
50.
http://www.esab.it/it/en/products/index.cfm?fuseaction=home.product&productCode=41033
7. http://www.esab.it/. [Online] ESAB. [Cited: 7th November 2015.]
51. Defects - Hydrogen Cracks in Steels - Identification. Bill Lucas, Gene Mathers, David
Abson. Cambridge : Connect (Orignal) - Amended version by The Welding Institute, 2000.
52. Hydrogen cracking - its causes, costs and future occurrence. HART, P H M.
Wollongong, Australia : Welding Technology Institute of Australia (WTIA), March 1999.
53. http://www.lincolnelectric.com/en-
us/consumables/Pages/product.aspx?product=Products_Consumable_StickElectrodes-
MildandLowAlloySteels-Excalibur-Excalibur7018-1MR(LincolnElectric).
http://www.lincolnelectric.com/. [Online] Lincoln Electric Arc Welding Company. [Cited:
8th November 2015.]
54. http://www.twi-global.com/technical-knowledge/faqs/material-faqs/faq-what-is-the-
difference-between-the-various-carbon-equivalent-formulae-used-in-relation-to-hydrogen-
cracking/. http://www.twi-global.com/. [Online] The Welding Institute. [Cited: 8th November
2015.]
55. Defects - Hydrogen Cracks in Steels - Identification. Bill Lucas, Gene Mathers, David
Abson. Cambridge : Connect (Original) - The Welding Institute (Amended), 2000.
56. Residual Stresses In Welded Structures. Leggatt, R.H. 144 - 151, Cambridge :
Internaional Journal of Pressure Vessels and Piping, 2008, Vol. 85.
57. Mathers, Gene. http://www.twi-global.com/technical-knowledge/job-knowledge/design-
part-1-090/. http://www.twi-global.com. [Online] [Cited: 14th November 2015.]
58. The Procedure Handbook of Arc Welding - Section 2.2-1 - The Design of Welded Joints.
Cleveland, Ohio : The Lincoln Electric Arc Welding Company, 1995.
59. http://www.twi-global.com/technical-knowledge/job-knowledge/distortion-prevention-
by-pre-setting-pre-bending-or-use-of-restraint-035/. http://www.twi-global.com. [Online] The
Welding Institute. [Cited: 14th November 2015.]
71
60. http://www.residualstress/stress measurements/.org. http://www.residualstress.org/.
[Online] [Cited: 14th November 2015.]
61. Residual stresses in welded structures. Leggatt, R.H. 144 - 151, Cambridge :
International Journal of Pressure Vessels and Piping, 2008, Vol. 85.
62. The International Journal of Pressure Vessels and Piping. Leggatt, RH. 144 - 151,
Cambridge : International Journal of Pressure Vessels and Piping, 2008, Vol. 85.
63. Residual Stresses In Welded Structures. Leggatt, RH. 144 -151, Cambridge :
International Journal of Pressure Vessels and Piping, 2008, Vol. 85.
64. Donald C. Zipperian, Ph.D. http://www.metallographic.com/Technical/Basics.pdf.
http://www.metallographic.com. [Online] Pace Technologies. [Cited: 22nd November 2015.]
65. Petzow, G. Metallographic Etching, 2nd Edition. [book auth.] ASM International.
Metallography. New York : ASM International, 1999.
66. http://www.metallographic.com/Brochures/SiCpaper.pdf.
http://www.metallographic.com. [Online] Pace Technologies. [Cited: 24th November 2015.]
67. http://www.struers.ie/default.asp?top_id=3&main_id=10&sub_id=16&doc_id=198.
http://www.struers.ie/. [Online] Struers . [Cited: 24th November 2015.]
68. http://www.buehler.co.uk/products/consumables/polishing-cloths.html.
http://www.buehler.co.uk. [Online] Buehler. [Cited: 24th November 2015.]
69. http://www.metallographic.com/Etchants/Etchants.htm. http://www.metallographic.com.
[Online] Pace Technoligies, 2006 - 2015. [Cited: 24th November 2015.]
70. Dieter, George E. Mechanical Metallurgy Page 331. New York : McGraw Hill, 1986.
ISBN 0-07-016893-8.
71. https://www.wpsamerica.com/ASME-WPS-DEMO.pdf. https://www.wpsamerica.com.
[Online] Weld Procedure Specifications America. [Cited: 27th November 2015.]
72. http://www.engineeringtoolbox.com/ansi-steel-pipes-d_306.html.
http://www.engineeringtoolbox.com. [Online] [Cited: 27th November 2015.]
73. http://www.efunda.com/processes/machining/mill_cutters.cfm. www.efunda.com.
[Online] efunda. [Cited: 30th January 2016.]
74. http://www.oerlikonline.hu/files/047.pdf. http://www.oerlikonline.hu. [Online] [Cited:
28th November 2015.]
75. http://www.lincolnelectric.com/en-
gb/consumables/Pages/product.aspx?product=Products_ConsumableEU_StickElectrodes-
Conarc-Conarc49(LincolnElectric_EU_Base). http://www.lincolnelectric.com. [Online] The
Lincoln Electric Arc Welding Company. [Cited: 28th November 2015.]
72
76. http://www.bocworldofwelding.com.au/media/pdf/file/library/WOWLibrary-
Preheating%20of%20materials-Consumables.pdf. http://www.bocworldofwelding.com.au/.
[Online] BOC Industrial Gases. [Cited: 31st January 2016.]
77. http://saajsteel.com/?page_id=1777. http://saajsteel.com. [Online] Saaj Steel. [Cited: 28th
November 2015.]
78.
http://www.esab.co.uk/gb/en/products/index.cfm?fuseaction=home.product&productCode=4
10059. http://www.esab.co.uk/. [Online] ESAB Industries. [Cited: 28th November 2015.]
79. http://www.twi-global.com/technical-knowledge/faqs/material-faqs/faq-what-is-the-
procedure-for-welding-en8-subsequently-known-as-080m40-and-11186-c40e-a-04-carbon-
steel-under-high-restraint-/. http://www.twi-global.com/. [Online] [Cited: 28th November
2015.]
80. http://www.gasweld.ie/product/esab-68-81-vac-pac-312l/. www.gasweld.ie. [Online]
[Cited: 15th April 2016.]
81. http://www.rapidwelding.com/files/T31224.pdf. www.rapidwelding.com. [Online] Rapid
Welding. [Cited: 15th April 2016.]
82.
http://www.rapidwelding.com/dynamic/Category.aspx?c=CK3SCLDPTS&o=0&zl=3&sq=14
. http://www.rapidwelding.com. [Online] Rapid Welding . [Cited: 28th November 2015.]
83. http://www.eastwood.com/tig-gas-lens-components-and-kits.html. www.eastwood.com.
[Online] Eastwood Welding. [Cited: 31st January 2016.]
84. http://www.bucanada.ca/media/BOHLER-UTP_Welding_in_tool_making.pdf - Page 10.
http://www.bucanada.ca. [Online] [Cited: 28th November 2015.]
85. http://www.interlloy.com.au/our-products/tool-steel/o1-tool-steel-100mncrw4/.
http://www.interlloy.com.au. [Online] Interlloy. [Cited: 28th November 2015.]
86. http://www.fhmachinery.com/grinders/5651.htm - Buehler Abrasimet 2 abrasive sample
cutter. http://www.fhmachinery.com. [Online] [Cited: 28th November 2015.]
87.
http://www.buehler.com/UK/Brochures/English/Mounting/SimpliMet%203000%20Brochure
.pdf. http://www.buehler.com. [Online] Buehler. [Cited: 28th November 2015.]
88. http://www.mitar.sk/prospekty/phoenix4000.pdf - Owners manual for Buehler Phoenix
4000 sample grinding & polishing machine. http://www.mitar.sk. [Online] 2000. [Cited: 29th
November 2015.]
89. http://www.substech.com/dokuwiki/doku.php?id=hardness_test_methods.
www.substech.com. [Online] Substances and Technologies. [Cited: 10th April 2016.]
73
90. http://www.met-tech.com/weld_engineering.html. www.met-tech.com. [Online]
Metallurgical Technologies, 2016. [Cited: 9th March 2016.]
91. http://www.met-tech.com/weld_engineering.html. www.met-tech.com. [Online]
Metallurgical Technologies Inc. [Cited: 10th April 2016.]
92. http://www.engineersedge.com/material_science/yield_strength.htm.
www.engineersedge.com. [Online] [Cited: 14th April 2016.]
93. http://www.prosaicsteel.com/api_5l_gr_b_carbon_steel_seamless_pipes.html.
www.prosaicsteel.com. [Online] Prosaic Steel. [Cited: 15th April 2016.]
94. http://www.highpeaksteels.com/en8-steel-properties/. www.highpeaksteels.com. [Online]
High Peak Steels. [Cited: 15th April 2016.]
95.
http://www.matweb.com/search/datasheet.aspx?matguid=42da7db7f74041a98f3ee0239b4c6a
c6&ckck=1. www.matweb.com. [Online] Mat Web. [Cited: 15th April 2016.]
96. http://www.westyorkssteel.com/tool-steel/o1/. www.westyorkssteel.com. [Online] West
Yorkshire Steel. [Cited: 24th February 2016.]
97. http://fordtoolsteels.com/wp-content/themes/twentytwelve/pdf/LSS_O1.pdf.
www.fordtoolsteels.com. [Online] Ford Tool Steels. [Cited: 25th February 2016.]
98.
http://www.aksteel.com/pdf/markets_products/stainless/austenitic/316_316l_data_sheet.pdf.
http://www.aksteel.com. [Online] AKS Steel. [Cited: 25th February 2016.]
99. Effect of Tempering Behavior on Heat Treated Medium Carbon (C 35 Mn 75) Steel.
V.K.Murugan, Dr.P.Koshy Mathews. 4, Coimbatore, India : International Journal of
Innovative Research in Science, Engineering and Technology, 2013, Vol. 2. ISSN: 2319-
8753.
100. http://www.engineershandbook.com/Tables/hardness.htm.
www.engineershandbook.com. [Online] [Cited: 14th April 2016.]
101. http://www.chegg.com/homework-help/questions-and-answers/microstructure-iron-
carbon-alloy-consists-proeutectoid-cementite-pearlite-mass-fractions-m-
q3821221?adobe_reloaded=true. http://www.chegg.com/. [Online] Chegg. [Cited: 24th March
2016.]
102. David Brandon, Wayne D. Kaplan. Joining Processes - An Introduction - Page 216.
New York : John Wiley & Sons, 1997. ISBN 0-471-96488-3.
103. Dieter, George E. Mechanical Metallurgy Page 334. New York : McGraw Hill, 1986.
ISBN 0-07-016893-8.
74
104. Kopeliovich, Dr. Dmitri.
http://www.substech.com/dokuwiki/doku.php?id=hardness_test_methods.
http://www.substech.com. [Online] [Cited: 27th November 2015.]
105. —. http://www.substech.com/dokuwiki/doku.php?id=hardness_test_methods.
http://www.substech.com. [Online] [Cited: 27th November 2015.]
106. England, Gordon. http://www.gordonengland.co.uk/hardness/rockwell.htm.
http://www.gordonengland.co.uk. [Online] [Cited: 27th November 2015.]