1 
STUDENT NAME -ANKIT KUMAR BHATT
INTRODUCTION 
2 
 Flame-retardant finishes provide textiles with an important 
performance characteristic that is it stopped the propagation of 
fiber when it comes in contact with fire. 
 NEEDS OF FLAME RETARDANTS 
 Protection of consumers from unsafe apparel 
 Firefighters and emergency personnel require protection 
 Floor coverings, upholstery and drapery protection 
 The military 
 the airline industry
Types of F.R. Fabric In Industry 
3 
Fabric which has to be padded with F.R. 
chemical 
Fabric which is made flame retardant at the 
time of manufacturing of yarn
HISTORY 
4 
About 450 BC EGYPTIANS used ALUM to reduce 
flammability of wood 
In 1638 clay & gypsum used for theater curtains. 
1821 GAY-LUSSAC mixture of borax & ammonium salt of 
phosphoric acid for linen 
1913 Perkin gives FR treatment for cotton by using so. 
Stannite & ammo. Sulphate.
Mechanisms of flame retardancy 
5 
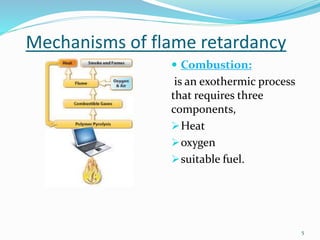
 Combustion: 
is an exothermic process 
that requires three 
components, 
Heat 
oxygen 
suitable fuel.
Mechanisms of flame retardancy 
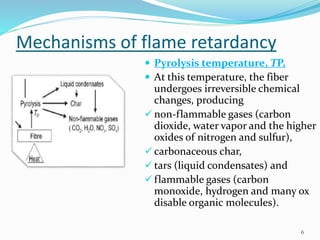
 Pyrolysis temperature, TP, 
 At this temperature, the fiber 
undergoes irreversible chemical 
changes, producing 
 non-flammable gases (carbon 
dioxide, water vapor and the higher 
oxides of nitrogen and sulfur), 
 carbonaceous char, 
 tars (liquid condensates) and 
 flammable gases (carbon 
monoxide, hydrogen and many ox 
disable organic molecules). 
6
Mechanisms of flame retardancy 
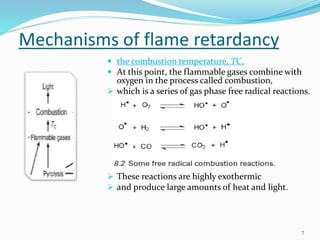
 the combustion temperature, TC, 
 At this point, the flammable gases combine with 
7 
oxygen in the process called combustion, 
 which is a series of gas phase free radical reactions. 
 These reactions are highly exothermic 
 and produce large amounts of heat and light.
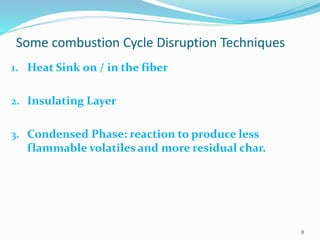
Some combustion Cycle Disruption Techniques 
8 
1. Heat Sink on / in the fiber 
2. Insulating Layer 
3. Condensed Phase: reaction to produce less 
flammable volatiles and more residual char.
Combustion Cycle Disruption Techniques 
9 
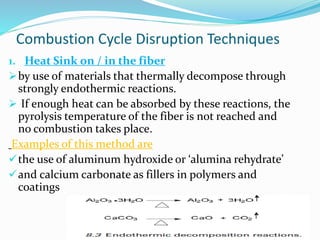
1. Heat Sink on / in the fiber 
by use of materials that thermally decompose through 
strongly endothermic reactions. 
 If enough heat can be absorbed by these reactions, the 
pyrolysis temperature of the fiber is not reached and 
no combustion takes place. 
Examples of this method are 
the use of aluminum hydroxide or ‘alumina rehydrate’ 
and calcium carbonate as fillers in polymers and 
coatings
Combustion Cycle Disruption Techniques 
10 
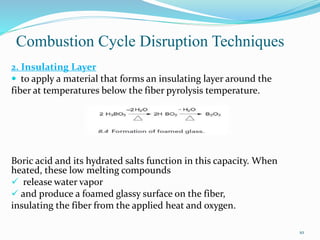
2. Insulating Layer 
 to apply a material that forms an insulating layer around the 
fiber at temperatures below the fiber pyrolysis temperature. 
Boric acid and its hydrated salts function in this capacity. When 
heated, these low melting compounds 
 release water vapor 
 and produce a foamed glassy surface on the fiber, 
insulating the fiber from the applied heat and oxygen.
Combustion Cycle Disruption Techniques 
11 
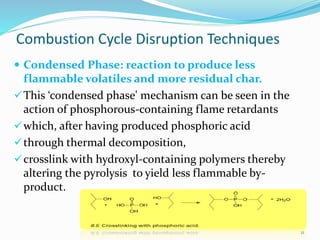
 Condensed Phase: reaction to produce less 
flammable volatiles and more residual char. 
This ‘condensed phase' mechanism can be seen in the 
action of phosphorous-containing flame retardants 
which, after having produced phosphoric acid 
through thermal decomposition, 
crosslink with hydroxyl-containing polymers thereby 
altering the pyrolysis to yield less flammable by-product.
Combustion Cycle Disruption Techniques 
12 
 The ‘condensed phase’ strategy includes 
the described mechanism 
of removal of heat and the enhancement 
of the decomposition temperature as in 
heat resistant fibers.
Testing of flame retardants 
The visual timing test- vertically 
The 45 degree test – 5 inch distance at such 
angle 
Hoop test- semi circular frame 
13
LOI 
 LIMITED OXYGEN INDEX is give us some 
information about flame retardancy 
 It is the minimum % of oxygen in oxy- nitro 
atmosphere require to sustain combustion 
L.O.I. = (O2)/(O2+N2)* 100 
HIGHER THE LOI MEANS MORE THE FLAME 
RETARDENT 
14
Factor affecting the f. resistance 
Fiber content 
Fabric structure 
weight 
15
Problems with flame retardant 
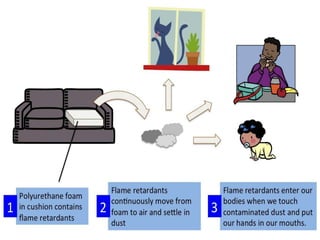
Toxicity 
Irritated towards skin 
Durability 
Flexibility 
16
17
18
Protective clothing for fire 
fighter (APPLICATION) 
NATIONAL FIRE PROTECTION ASSOSIATION has set 
a fundamental requirement that it’s TPP value must 
be 35 minimum. 
According to NFPA each far. cloth ,, contain three 
component – 
Outer shell 
Moisture barrier 
Thermal barrier 
19
Protective clothing for fire 
fighter 
 As an example LOS ANGELOUS fire department 
used- 
 outer shell –nomex/kevlar in a rip stop weave 
Thermal insulator 
Moisture barrier 
20
21
22
23