Abrasives & AbrasiveWheels
Their Nature, Manufacture and Use
A COMPLETE TREATISE ON
THE MANUFACTURE AND PRACTICAL USE OF
ABRASIVES, ABRASIVE WHEELS AND GRINDING OPERATIONS
INCLUDING
NATURAL AND ARTIFICIAL ABRASIVES, PRODUCTION AND PREP-
ARATION OF ABRASIVES, GRITS, GRADES AND BONDS, SHARPEN-
ING AND GRINDING STONES AND WHEELS, TESTING WHEELS
FOR EFFICIENCY, TRUING, REBUSHING AND INSTALLING
WHEELS, SAFETY DEVICES, AND DUST-COLLECTING SYSTEMS,
COMPLETE EXPOSITION ON SURFACE, EXTERNAL AND INTERNAL
GRINDING AND COMPREHENSIVE DATA COVERING THE PHYS-
ICAL AND CHEMICAL NATURE OF ABRASIVES IN GENERAL
BY
FRED B. JACOBS
A PRACTICAL HANDBOOK FOR ENGINEERS, FACTORY SUPERINTEN-
DENTS, FOUNDRYMEN, SHOP FOREMEN AND MECHANICS IN GENERAL
FULLY ILLUSTRATED
New York
The Norman W. Henley Publishing Company
2 West 45th Street
1919
8.
Copyrighted, 1919, by
TheNorman W. Henley Publishing Company
Printed in U. S. A.
Printing Presswork and Binding by
Harper & Brothers, New York
9.
PREFACE
THE art offinishing metals by abrasion is one of the
oldest mechanical practices in existence, dating from
the time prehistoric man discovered that he could fashion
his wood and bone implements by rubbing them on rocks of a
gritty nature.
The grindstone is, without doubt, the oldest form of
grinding wheel known. With the early development of
the mechanical arts, it was discovered that a sandstone cut
in circular shape and mounted upon a revolving shaft,
showed higher efficiency than the side of a rock for sharpen-
ing and shaping various implements. It is definitely known
that grindstones, rotated by power, were used in the manu-
facture of armor as early as the year 1570. It is also
known that the emery deposits of the Grecian Archipelago
were known to the ancients and the value of this abrasive
recognized, as many writers of early days referred to emery
under various names. In considering some of the mechan-
ical achievements of the handicraftsmen who worked with
metals centuries before the Christian era, it is hard to
conceive how they attained so high a degree of perfection
without the use of an alumina abrasive for tool-sharpening
purposes.
While the practice of fashioning tools and implements by
abrasion is in all probability as old as civilization itself,
modern grinding, as we accept this term, is a compara-
tively recent development. About half a century ago,
the individual workman made his own grinding wheels of
glue and emery.
The first attempt at precision grinding consisted of finish-
ing the chilled iron calender rolls used in the paper-making
5
10.
PREFACE
industry. Owing tothe hard nature of the material in
question, it was a long and tedious process to turn these
rolls accurately.
The development of the sewing-machine industry in the
New England States gave impetus to the development of
the grinding-wheel business. As a matter of fact, the first
attempts at cylindrical grinding, aside from roll grinding,
consisted of finishing parts of the Wilcox & Gibbs sewing
machine. The work was done by the Brown & Sharpe
Mfg. Co.
With the advent of the automobile industry, over twenty
years ago, the grinding-wheel business received a fresh
impetus as a rapid means was in demand for the accurate
finishing of parts.
Today, the modern grinding wheel is among the most
useful of modern shop accessories. Without it, it would be
impossible to maintain the present-day standard of rapid
production. In practically every line of metal working,
the grinding wheel plays an important part, its usefulness
ranging all the way from the rough grinding of castings and
forgings to the finishing of accurate surfaces, both plane and
cylindrical.
In presenting this work, the writer has taken great
precaution to make sure that every statement is authentic.
Aside from knowledge gained through many years as a
journeyman machinist, later supplemented with several
years' experience as a grinding-wheel salesman, many months
were spent in collecting data, verifying statements and
consulting reliable authorities, both in this country and
abroad.
The writer is indebted to the following manufacturers
and individuals who cheerfully answered numerous letters
and supplied valuable data and photographs:
Abrasive Co. The Carborundum Co.
American Emery Wheel Works Chicago Wheel & Mfg. Co.
The Blanchard Machine Co. The Cincinnati Milling Machine
Brown & Sharpe Mfg. Co. Co.
6
11.
PREFACE
The Cleveland StoneCo.
Cortland Grinding Wheel Corp.
Detroit Grinding Wheel Co.
Diamond Machine Co.
Parrel Foundry & Machine Co.
Metal & Thermit Corp.
H. G. Hammett.
Hampden Corundum Wheel Co.
The Heald Machine Co.
Frederick S. Jacobs, data on axe-
grinding.
'
Landis Tool Co.
Manufacturers Corundum Co., Ltd.
Minnesota Mining & Mfg. Co.
Newton Machine Tool Works.
Norton Co.
Norton Grinding Co.
Penton Publishing Co.
Pittsburgh Crushed Steel Co.
Pratt & Whitney Co.
Fred E. Rogers, editor emeritus of
Machinery.
Safety Emery Wheel Works.
Springfield Grinding Co.
Springfield Mfg. Co.
Sterling Grinding Wheel Co.
B. F. Sturtevant Co.
Superior Corundum Wheel Co.
United States Geological Survey.
Vitrified Wheel Co.
Waltham Grinding Wheel Co.
Wardwell Mfg. Co.
Permission to reprint material by the writer which had
been previously published, was granted by the following
publishers :
Penton Publishing Co., Marine Review.
McGraw Hill Co., American Machinist.
S. S. Smith Co., The Woodworker.
W. R. C Smith Publishing Co., Iron Tradesman.
Iron Age Co., The Iron Age.
The MacLean Publishing Co., Ltd., Canadian Machinery.
The Mines Publishing Co., Ltd., publishers of The Canadian Mining
Journal, gave permission to reprint material concerning corundum.
FRED B. JACOBS.
June, 1919.
13.
CONTENTS
CHAP. PAGE
PREFACE ix
I.NATURAL ABRASIVE SUBSTANCES Pages 13 to 36
Nature of natural abrasives Where found History of natural
abrasives Commercial application Sandstone Emery Corun-
dum Garnet Diamond Bort diamond Flint Quartz Nat-
ural sharpening stones Arkansas Washita Hindustan Tripoli
Pumice.
II. ARTIFICIAL ABRASIVES Pages 37 to 64
Various artificial abrasives Their physical and chemical properties
Their Commercial application Methods and processes employed
in the production of artificial abrasives Carborundum Alundum
Aloxite Boro- Carbone Oxalumina Adamite Crystolon, etc.
Relative hardness and abrasive efficiency of various materials
Artificial production of precious stones Their abrasive properties
Other artificial abrasives and their production Experimental
work Electro-thermic processes Production of rouge and crocus
Diamonds and crushed steel Angular grit.
III. THE MANUFACTURE OF GRINDING WHEELS .... Pages 65 to 82
Composition of grinding wheels Desirable and undesirable proper-
ties Bonds Shellac Rubber Fusible clays Silicate of soda
Vitrified wheels Method of oroducing vitrified wheels Puddled
process Pressed process Silicate wheels Shellac wheels Rubber
wheels Clay bond used in vitrified wheels Choice of bonding ma-
terial Wheel-turning Kiln used Heating of kiln and work
Cooling of kiln Dressing wheels Bushing wheels Speed tests for
wheels Elastic process Rubber process.
IV. ARTIFICIAL SHARPENING STONES Pages 83 to 87
Properties of artificial stones Carborundum stones Method of
manufacture Bond Grit Grade Finishing Combination
stones Carborundum rubs.
V. GRITS AND GRADES . . . ; Pages 88 to 96
Designation of grits and grades Mixed grits Grits of abrasive s
papers Standard grades Wheels Relation of speed to grade and
grit Wheel speeds for various operations.
9
14.
CONTENTS
CHAP.
VI. TESTING WHEELSFOR EFFICIENCY Pages 97 to 114
Selection of wheels Improper methods of testing Practical testing
methods Items to be noted in a wheel test How to figure result
Formula for finding volume of abrasive material in a wheel General
considerations Wheel tests.
VII. LABORATORY TESTS Pages 115 to 122
Apparatus and appliances used Limitations of laboratory tests
Factors to be considered Laboratory testing machine Data for
test Work used in testing.
VIII. GRINDING WHEEL vs. GRINDSTONES Pages 123 to 128
Advantages of natural and artificial abrasive used in wheels Early
use of grindstones Special work where grindstones are still em-
ployed Action of grinding wheel.
IX. THE ECONOMIC ADVANTAGE OF USING LARGE WHEELS .
Pages 129 to 132
Factors to be considered in choosing a wheel Comparative price of
wheels of various sizes Advantage of large wheels in certain work
Why large wheels are more efficient.
X. TRUING DEVICES FOR GRINDING WHEELS Pages 133 to 138
Abrasive action Tools used in truing wheels Use of bort and
carbonado diamonds in tools Getting stones in tool Procedure in
truing wheels.
XI. RE-BUSHING GRINDING WHEELS Pages 139 to 141
Methods used in bushing wheels Tools employed Metals used.
XII. SUGGESTIONS TO FOLLOW IN ORDERING GRINDING WHEELS
Pages 142 to 144
Information to be given with grinding-wheel order Factor govern-
ing selection of wheels How to determine what kind of a wheel
should be used Ordering special wheels.
XIII. DESIGN OF DUST-COLLECTING SYSTEMS .... Pages 145 to 150
State law requirments Design of wheel hood General design
Size of exhaust pipe for different size wheels Elbows Collars
Method of erection Clean-out Fan Dust-collector Exhaust
systems.
XIV. SAFEGUARDING GRINDING WHEELS Pages 151 to 165
Why wheels break Cause of accidents How wheels are packed
and tested before leaving factory Wheel speeds Mounting wheels
properly What causes wheels to burst Safety flanges Work rest
Wheel guards Grinding on small wheels Precautions for the
workman.
10
15.
CONTENTS
CHAP.
XV. ABRASIVE PAPERSAND CLOTHS Pages 166 to 175
Abrasive substances used in making abrasive paper History of
abrasive paper How abrasive paper and cloth is manufactured
Grades of abrasive paper and cloth Finding percentage of iron in
garnet Testing garnet paper Paper and cloth abrasive discs--
Testing discs for efficiency.
XVI. SURFACE GRINDING Pages 176 to 215
Finishing work by surface
grinding Development of the surface
grinding machine Finishing locomotive guide bars Rotary
grinding fixture Wheel speeds Cuts Die grinding How dies
are held Grinding punches Care of wheels Magnetic chucks
Demagnetizes Proper wheel selection for surface grinding Types
of surface-grinding machines Standard wheel list.
XVII. CYLINDRICAL GRINDING Pages 216 to 242
Cylindrical grinders Operation of grinders Driving devices for
work Proper wheel speeds for various metals and work Traverse
feed Depth of cut Roughing and finishing cuts Sparking
Backrest and steadyrests Lubrication of work Lubricating com
pounds and mixtures Dressing and truing wheels while on the
grinder Chatter marks and their remedy Selection of proper
wheels for use on cylindrical grinders Universal grinders Grinding
tapers Various operations on universal grinder.
XVIII. INTERNAL GRINDING Pages 243 to 262
Internal grinding machines Internal grinding on universal grinder
Setting up universal grinder for internal work Grinding double
tapers Automatic grinders Grinding holes in spur and bevel gears
Chucks Wet and dry grinding Proper speeds Selection of
wheels Operating of cylinder grinders Cylinder grinding.
XIX. SPECIAL GRINDING OPERATIONS Pages 263 to 289
Grinding calender rolls Special grinding machines Roll grinders
and roll grinding Corrugating flour-mill rolls Grinding crank-
shafts Grinding cam shafts Locomotive valve gears.
XX. CUTTER SHARPENING Pages 290 to 307
Machines employed for cutter grinding Adjustments and attach-
ments on cutter grinders Grinding spiral cutters General opera-
tion of cutter grinders Selection of wheels Speeds Depth of cut.
XXI. SAW SHARPENING Pages 308 to 321
Band saws and circular saws Operation of band-saw sharpening
machine Sharpening band saws Grinding in new teeth Care of
machine Selection of wheels for saw gumming Machines for
sharpening cold saws Sharpening hack-saw blades.
ii
17.
CHAPTER ONE
NATURAL ABRASIVESUBSTANCES
Nature of natural abrasives Where found History of natural abrasives
Commercial application Sandstone Emery Corundum Garnet
Diamond Bort diamond Flint Quartz Natural sharpening stones
Arkansas Washita Hindustan Tripoli Pumice.
NATURAL
abrasives are being found in many parts of
the world. In a broad sense, the list includes all
minerals capable of abrasive action, but from a commercial
point of view, the principal natural abrasives are sandstone,
emery, corundum and garnet. The diamond is, of course,
a natural abrasive; indeed it is the hardest of all, but it is
needless to state that its rarity excludes it from the list of
commercial abrasive materials.
SANDSTONE
The first abrasive to be used in the form of a wheel was
in all probability sandstone. The use of a revolving stone
for sharpening purposes is so old that the beginning is
lost in antiquity. It seems reasonable to believe, however,
that the artificers of early civilization borrowed the idea
of a revolving sharpening stone from the crude mills used
many centuries ago for the grinding of grain.
Sandstone is a very curious mineral, indeed, as it consists
of uniform grains of sand (generally quartz with a small
percentage of feldspar and mica) firmly cemented together
with silica. Some varieties of sandstone, the Craigleith
stones used in the cut-glass industry for instance, are prac-
tically pure silica, this material often running as high as
98 per cent. Sandstone is found in many parts of the
13
18.
ABRASIVES AND ABRASIVEWHEELS
world and in this country the most extensive deposits that
are worked for the production of grindstones are in Ohio
and Michigan. The Gray Canyon quarry at Amherst,
Ohio, is classed as the largest quarry in the world. Sand-
stones are of various colors, these being derived from
impurities that penetrated the mass during the formative
stage. Pure siliceous stones are white, or pale yellow in
cases where small quantities of iron oxide are present. A
red tinge is generally due to hematite, yellow to limonite,
green to glauconite, gray to clay and shale, and black, as
observed in black Graileith stones for example, to manganese
dioxide.
The average layman is of the opinion that all grindstones
are alike, but this supposition is erroneous for, in forming
the sandstone of which the grindstones of commerce are
made, it would appear that Nature anticipated the wants
of man by providing not only several grits to choose from,
but several grades as well. To insure an ample supply
of grits and grades, grindstone manufacturers generally
control holdings in various localities.
Before the advent of the grinding wheel, sandstone was
the only abrasive to be used in the form of a wheel. Its
use was, of course, limited, as practically the only grinding
done in the early manufacturing days consisted of tool
sharpening. Grindstones are used at present in large quan-
tities for sharpening edge tools, cutlery, etc., often in
preference to modern abrasive wheels. Many reasons for
this practice are explained later, under the heading, Grind-
stones Vs. Grinding Wheels.
EMERY
Emery, which in reality is an impure form of corundum,
has been known as an abrasive from very remote times. Its
value as an abrasive was known to the ancient Greeks/
Dioscorides referred to it as a stone used in gem engraving.
Emery was also known to the Romans, Pliny and other
19.
EMERY
writers referring toit as naxium. There is also seme
authority for the statement that in the "adamant" of
the Old Testament, translated from the Hebrew, shamir
referred to emery ore. ^The principal emery deposits that
furnish the emery of commerce are located in Asia Minor,
in the basins of the Sarabat and Mender rivers. In the
Grecian Archipelago, the best known of these deposits are
located on the Island of Naxos, and in this country near
Chester, Mass., and Peekskill, N. Y.
Emery looks like iron ore, being of a dense, granular con-
struction. Its luster is metallic, while its color runs from
blue-black to black. It can truly be called a unique mineral,
as it is a mixture of alumina oxide and iron as magnetite
and hematite. At one time, all of the world's supply of
emery came from the Grecian Isles, principally Naxos, but
during the year 1847 Dr. J. Lawrence Smith located im-
portant emery deposits in Asia Minor. Dr. Smith's dis-
coveries proved to be of great benefit to the emery-consum-
ing trade owing to the fact that the price of emery was
materially reduced. Asia Minor or Turkish emery, as the
new material was called, at once became popular, as it
proved to be an efficient abrasive for many purposes.
Turkish emery always occurs in limestone or marble,
the deposits resting on gneiss, schist and mica slates, while
Naxos emery is generally found in limestone beds, being
associated with crystalline schists. One noticeable dif-
ference between the emery of the Grecian Archipelago and
that of Asia Minor is that in the former are numerous small
particles of mica which are seldom observed in the latter *-
The mining of both Turkish and Naxos emery is generally
carried on in a very primitive manner. Being near the sur-
face, the ore is easily removed as it is often present in loose
boulders. Masses that are too large for transportation to
the sea coast, are generally broken into fragments through
the process of heating them for a number of hours followed
by a sudden cooling with water. This causes the ore to
fracture in many places, and, by means of hammer blows, ^
15
20.
ABRASIVES AND ABRASIVEWHEELS
it is an easy matter to reduce the ore to pieces suitable for
transportation. The low cost of mining, together with
moderate transportation costs, accounts for the fact that
Turkish emery finds a ready sale in this country in competi-
tion with American emery. For the purpose of grinding-
wheel manufacture, however, *&axos emery is considered
superior to all other kinds as it is the hardest, toughest
and most uniform. The foregoing sounds like a broad
statement, to be sure, but it is the consensus of opinion
expressed by leading grinding-wheel manufacturers who
make wheels of emery.
L
The discovery of emery in this country dates back to
about the year 1830, at which time a railroad was being
built from Boston to the Hudson River. In making a cut
near Chester, Mass., a deposit of emery ore was uncovered,
which, at the time, was taken for iron ore. As previously
stated, emery and iron ore resemble each other closely.
Blast furnaces were erected and provision made for working
the ore on a moderately large scale. At the first attempt
to smelt the ore, however, great difficulties were encountered
in separating the iron from the alumina and the deposits
were ultimately condemned as too refractory for practical
purposes.
The mine remained idle and almost forgotten for a num-
ber of years. In 1864 or thereabout, Dr. H. S. Lucas,
realizing the possibilities of working the deposits as a source
of abrasive supply to compete with the foreign product,
bought the property and began to successfully operate it
as an emery mine. Operations have been continued in
this district until the present day. The emery in question
is associated with amphibolite and serpentine, and, as the
veins of ore reach several hundred feet underground, it is
necessary to work them by extensive tunneling.
Mention should also be made of the emery deposits in
New York state in the vicinity of Peekskill. rhis emery,
which is called a spinel emery, does not occur in a continu-
ous vein, but in segregated masses, being associated with
16
21.
EMERY
morite rocks. Inthis ore spinel, which is magnesium
aluminate, MgAl2o4 ,
furnishes the abrasive agent, since
spinel has a relative hardness of 8, as against 9, the hardness
of alumina, it is seen that spinel emery is somewhat softer
than other varieties of true emery. The value of spinel
emery should not be overlooked, however, as it furnishes
an efficient polishing material in cases where a very hard
and tough abrasive is not desired.
The specific gravity of emery varies in different speci-
mens from 3.7 to 4.3 and the percentage of alumina oxide
from 30 to 70. The abrasive power, sometimes called the
effective hardness, is not proportional to the amount of
alumina contained, being influenced to a great extent by
the proportions of other component parts in the form of
impurities such as silica, lime magnesia, etc., and the
structure of the grain itself. For the purpose of grinding-
wheel manufacture, the value of emery as an abrasive agent
is determined by the amount of alumina oxide present and
the toughness of the grain itself.
~^
In common with other natural products, emery ore
varies in' a number of characteristics. This is true not
only of specimens from different mines, but of the product
of one mine as well. To market a high-grade emery, it is
necessary to pay especial attention to the selection and
grading of the crude ore, to which end the use of the micro-
scope cannot be recommended too strongly, as by this
means more can be learned of the quality of the emery
than by resorting to any other method, aside from the
actual working test of the finished product.
As emery may have a high percentage of alumina and
at the same time the ore may be so constituted that, after
crushing, the grains will seem to possess no cutting points.
Such an emery does not make a very efficient grinding
wheel.
Some specimens of emery crush up into the proper kind
of grains, as far as cutting points are concerned, but at the
same time nothing but fine grains are produced. Again
22.
ABRASIVES AND ABRASIVEWHEELS
it is sometimes noticed that small flakes of mica are
scattered through the ore, which is sure to cause trouble
in the vitrifying process if the emery is used in the
manufacture of vitrified grinding wheels. It is readily
seen that an efficient abrasive cannot be made of an
emery ore selected at random. It is of the utmost im-
portance to know the nature of the grain to adapt the
same for a given abrasive purpose.
At one time, all grinding wheels were made of emery.
Of late years, however, corundum and the different artificial
abrasives are used. At the same time, notwithstanding
the efficiency of modern abrasives, the more ancient emery
wheel still has its field of usefulness, and, strange as it may
seem, on some classes of grinding, steel castings and heavy
malleables, for instance, emery wheels continue to show
the highest efficiency. This statement is not made thought-
lessly, but is the result of several years of observation spent
in representing grinding-wheel manufacturers.
From a theoretical point of view, it would seem that
abrasives containing a higher percentage of alumina than
is present in emery, would prove more efficient, regardless
of the nature of the work. Actual tests, however, have
proven beyond a doubt that for certain purposes the emery
wheel is still in a position to successfully compete with
artificial abrasives. This is explained in a subsequent
chapter.
Again, emery wheels are comparatively low in price, and
they find a ready market among consumers whose grinding-
wheel wants are few. A manufacturer who uses grinding
wheels intermittently, a few minutes at a time, is not con-
cerned whether or not the wheel shows the highest efficiency.
As long as it gives satisfaction, within certain limits, no
good reason is see'n why a higher price should be paid for
a more improved abrasive.
Another factor, that should be mentioned while consid-
ering the emery wheel, is that owing to the high percentage
of oxide of iron contained, this abrasive, grit for grit, leaves
18
23.
EMERY
a finer finishthan any other abrasive material used in
grinding-wheel manufacture. Even on precision work, such
as gauge grinding and other similar operations, the emery
wheel still plays an important part and it is often the choice
of many engineers who know abrasives for their actual
worth.
Emery wheels, or emery stones, as they are termed in this
case, are also largely used for hulling oats and rice, taking
the place of the bed and runner natural stones as used in the
ordinary buhr mill. To whom the credit belongs for intro-
ducing the above stones, is not known for a certainty, but
experience has proven that the emery stone compares
favorably with the natural stones heretofore used for this
purpose.
Coarse emery is used in the form of bricks for rubbing
stone and various metals while the finer grades of emery
are made into sharpening stones, scythe stones, etc. Of
late years, however, artificial sharpening stones made of
electro-thermic abrasives (Carborundum, for example) have
largely replaced those made of emery. For a few specific
purposes, emery stones are still in use owing to the high
finish they produce.
v
ln the form of grains and powders, emery is used for a
number of purposes such as finishing bevels on plate glass,
lapping hardened steel, polishing precious stones, etc., or,
in fact, for any purpose where a tough, durable abrasive in
grain form is desired.
Emery grain is also used to a great extent on polishing,
or set-up wheels, as they are termed, for finishing an end-
less variety of metal parts such as edge tools, cutlery, parts
of firearms, etc. Various kinds of emery act differently
on a polishing wheel and suitable grades for specific pur-
poses are generally chosen after careful experiment. One
reason why emery gives such good results on polishing
wheels is that its comparatively rough fracture presents
a good holding surface for the glue, which factor is not
true of many of the manufactured abrasives. Carborun-
19
24.
ABRASIVES AND ABRASIVEWHEELS
dum, on account of its smooth, glassy surface, does not
form a very efficient abrasive to use on a polishing wheel.
Emery paper and cloth are used to a large extent in the
mechanical arts for smoothing and polishing small, intricate
parts of small machinery and instruments.
In the study of the occurrence of emery, we are con-
fronted with two very curious facts. First, emery is a
mixture of iron oxides and alumina and, second, this com-
position occurs in but few places in the world pin points
on the earth's surface, as it were. In American emery, Prof.
J. H. Pratt regards the alumina and iron oxides as basic
segregations from an igneous magma. This, of course, is
within reason since it is an accepted fact that the earth
was at one time a molten mass of elements, and as this
mass slowly cooled, the various elements combined and
sometimes segregated. What force of nature caused the
elements of iron and alumina to segregate together, in
practically the same manner, is beyond the knowledge of
the writer.
CORUNDUM
V
The name corundum was originally applied to the ruby
and sapphire of India, the word being derived from the
Sanskrit (kurminda) and literally means ruby. The variety
of corundum we are dealing with is called, by the older
mineralogists, impure corundum and comprises the numerous
varieties that are not transparent or perfect enough to be
used as gem stones.
Some thirty years ago, corundum was regarded as a
comparatively rare mineral, but at the present time it is
known to occur abundantly in several localities in this
country and in Ontario, Canada. In this country, it occurs
in igneous rocks, principally syenites, and in several gneisses
and schists. It also occurs in alluvium deposits in sands and
gravels. Canadian corundum occurs in nepheline syenite
associated with Laurentian gneiss.
Of the origin of corundum but little is known for a cer-
25.
CORUNDUM
tainty, as astudy of his mineral calls for exhaustive research
work on the part of the geologist, who is sometimes reticent
when it conies to establishing hard and fast rules. Prof.
J. H. Pratt, who has made a deep study of the occurrence
of corundum, in this country and elsewhere, considers that
the corundum of North Carolina segregated from a molten
magma, the separation taking place at an early period of
consolidation. ^
Canadian corundum has of recent years been regarded
as an essential rock constituent. Regarding the corundum
of Ontario, H. E. T. Haultain states that the corundum-
bearing rocks are not dykes, that they are not eruptive,
and that there is no sign of separation from magma.
The principal Canadian deposit of corundum occurs at
Craig Mountain, which is situated in Raglan Township,
Renfrew County, Ontario. In this country, corundum is
found in the following states: Maine, Massachusetts,
Connecticut, New York, Pennsylvania, Delaware, Virginia,
North Carolina, South Carolina, Tennessee, Georgia, Col-
orado, Montana, California and Idaho.
'"'
Corundum is found in three different ways; block corun-
dum, crystal corundum and sand corundum. Under the
heading of block corundum, is included corundum found in
masses whether large or small.
(
This is the most difficult
form of corundum to mine. Owing to its extreme hardness,
it is impossible to drill it for the purpose of blasting. Thus
it is not easily broken up. When block corundum is mixed
with foreign substances, such as feldspar, hornblende, etc.,
it is often difficult to clean, whereas a block corundum
free from superfluous foreign matter makes an ideal ore,
provided the parting planes are -not too well developed.
The disadvantage of numerous parting planes is explained
later.
Corundum crystallizes in the rhombohedral division of
the hexagonal system and under the head of crystal corun-
dum is included all the crystal varieties of corundum
which occur in block corundum or% in sand or gravel.
21
26.
ABRASIVES AND ABRASIVEWHEELS
Some of these crystals take the form of a hexagon with a
prism at each end, in which case the crystal is termed
"barrel corundum." Many of these crystals are of no defi-
nite form, being enclosed in compact masses of surrounding
material.
Very small crystals and small grains are termed sand
corundum and often occur between a corundum-bearing
peridotite rock and the surrounding gneiss or schist.
Corundum possesses no true cleavage, but parting planes
are usually present along which the crystal fractures. How-
ever, if these planes are so numerous as to be present in
the small grains of abrasive material that constitute a
grinding wheel, a low abrasive efficiency will be the result
because the grains will readily fracture, thus breaking away
before becoming dull and useless.
An ideal corundum for an abrasive wheel is one wherein
the grains are free from parting lines, thus they will, on
becoming dull, break with the irregular to conchoidal frac-
ture, which is a characteristic of corundum. As a matter
of fact, all varieties of corundum have comparatively the
same degree of hardness, that is, from 8.8 to 9., but some
varieties are much higher in abrasive efficiency than others.
This is due to the fact that the parting planes are sometimes
too numerous as previously stated. This accounts for the
fact that some makes of corundum wheels are superior to
others. The only practical test for the abrasive efficiency
of a doubtful corundum is to make some sample wheels of
it and have them tested on actual work under every-day
working conditions.
From a theoretical point of view, corundum contains
but two elements, alumina and oxygen, its chemical formula
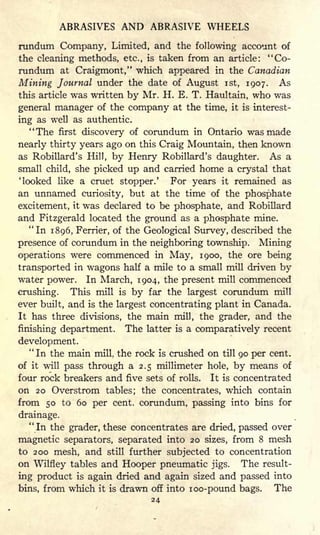
being A12O3 . Commercial corundum, as well as the gem
varieties, generally contains a trace of silica, ferric oxide
and combined water. The following table, which is taken
from Bulletin No. 269 of the United States Geological
Survey, gives the chemical analyses of several well-known
corundums.
27.
CORUNDUM
ANALYSES OF CORUNDUM
Sincecorundum occurs more abundantly than emery, the
consumer of grinding wheels often asks why corundum
wheels command a higher price than wheels made of emery.
It is true that corundum deposits are numerous, but not
all of these corundums are of the correct structure for
grinding-wheel use, as above explained, and, again, co-
rundum goes through a comparatively expensive process
before it is fit for the grinding-wheel manufacturers.
It must be borne in mind that corundum, as it comes from
the mine, is not in a pure state, being mixed with other
minerals, such as feldspar, hornblende, margartite, mus-
covite, etc. Corundum is sometimes found in huge masses
weighing many tons and in cases of this kind, the elimi-
nation of the foreign matter is often a difficult problem.
Again, a corundum that is to be used in the manufacture
of vitrified wheels should be free from such substances as
mica, garnet and feldspar. Otherwise difficulties are sure
to be encountered in the vitrifying process.
In describing the methods used in mining and cleaning
corundum for the market, it may be well to first consider
the mines at Craigmont, Canada, as the methods and facili-
ties used there are generally acknowledged to be the most
up-to-date and practicable.
The above mine is worked by the Manufacturers Co-
23
28.
ABRASIVES AND ABRASIVEWHEELS
rundum Company, Limited, and the following account of
the cleaning methods, etc., is taken from an article: "Co-
rundum at Craigmont," which appeared in the Canadian
Mining Journal under the date of August ist, 1907. As
this article was written by Mr. H. E. T. Haultain, who was
general manager of the company at the time, it is interest-
ing as well as authentic.
"The first discovery of corundum in Ontario was made
nearly thirty years ago on this Craig Mountain, then known
as Robillard's Hill, by Henry Robillard's daughter. As a
small child, she picked up and carried home a crystal that
'looked like a cruet stopper.' For years it remained as
an unnamed curiosity, but at the time of the phosphate
excitement, it was declared to be phosphate, and Robillard
and Fitzgerald located the ground as a phosphate mine.
"In 1896, Ferrier, of the Geological Survey, described the
presence of corundum in the neighboring township. Mining
operations were commenced in May, 1900, the ore being
transported in wagons half a mile to a small mill driven by
water power. In March, 1904, the present mill commenced
crushing. This mill is by far the largest corundum mill
ever built, and is the largest concentrating plant in Canada.
It has three divisions, the main mill, the grader, and the
finishing department. The latter is a comparatively recent
development.
"
In the main mill, the rock is crushed on till 90 per cent.
of it will pass through a 2.5 millimeter hole, by means of
four rock breakers and five sets of rolls. It is concentrated
on 20 Overstrom tables; the concentrates, which contain
from 50 to 60 per cent, corundum, passing into bins for
drainage.
"In the grader, these concentrates are dried, passed over
magnetic separators, separated into 20 sizes, from 8 mesh
to 200 mesh, and still further subjected to concentration
on Wilfley tables and Hooper pneumatic jigs. The result-
ing product is again dried and again sized and passed into
bins, from which it is drawn off into zoo-pound bags. The
24
29.
CORUNDUM
run of bagseach day is sampled by hand, every size by
itself, and these samples are carefully assayed, and accord-
ing to the assay results, the bags are stocked in the finishing
department.
"The finishing department performs three functions. It
thoroughly mixes the product so as to give a uniform ma-
terial complying closely with fixed standards. It re-screens
each size so as to eliminate the results of carelessness in
the grader. It automatically samples every lot of thirty
bags.
"The finishing foreman, knowing the assays of the con-
tents of his bags, mixes thirty hundredweight at a time
in a hopper. From this hopper, the corundum passes in a
thin, flat stream past a draft of air, which blows away the
mica. It then passes over a set of shaking screens, which
screen out both undersize and oversize particles and from
this it passes to a bin whence it is drawn off past an auto-
matic sampler direct into canvas bags, which are filled to
contain 100 pounds of corundum.
"The bags are then sewn up by machinery and marked
for size and lot number. The samples are tested by hand
screens for accuracy of sizing, by the eye for pyrites and
hornblende contents, by the magnet for magnetite contents,
and in the assay office for both corundum and iron content.
"On receipt of the assay results, the bags are marked G
or Gi, G grade being for silicate wheels and the polishing
trade, and Gi for the vitrified wheel trade. A sample
weighing about half a pound, representing each lot of
thirty bags, is stored for reference."
As before stated, corundum is found in many parts of
this country; one of the well-known mines is called the
Corundum Hill Mine. It is located in Macon County,
North Carolina. Corundum was discovered here in 1870
and mining operations were commenced a year later. This
corundum is found in a peridotite rock. The above mine
yields block, crystal and sand corundum having a high
abrasive efficiency in both silicate and vitrified wheels.
25
30.
ABRASIVES AND ABRASIVEWHEELS
The corundum of this mine enjoys a wide reputation, in-
deed, one well-known manufacturer of grinding wheels ad-
vertises the fact that this brand of corundum is used.
Another famous mine, the Laurel Creek mine, is located
in Rabun County, Georgia. This corundum is also found in
peridotite and often in massive blocks, many of them weigh-
ing several hundred pounds. One mass of corundum taken
from this mine is reported to have weighed over 5,000
pounds. It is said that this mine has furnished the largest
masses of corundum ever mined in any locality.
An excellent grade of corundum is also found in Gallatin
County, Montana, where it occurs in a syenite rock. The
crystals are of all sizes up to eight inches long and some
have been found that weighed two pounds. Montana
corundum is being worked by modern methods. The
mills are equipped with up-to-date machinery. Several
grinding-wheel manufacturers have used this corundum,
reporting it as making an excellent grinding-wheel grade.
The above corundum deposits are mentioned because
they are well known to the corundum-consuming trade.
It must not be inferred from this, however, that excellent
grades of corundum are not found elsewhere in this country.
As a matter of fact, there are over 160 corundum deposits
that have been listed by geologists, many of them yielding
an excellent grade of material.
Abrasive engineers admit that corundum of the right kind
makes a very efficient grinding wheel for all purposes, with
the exception of materials of low tensile strength such as
cast iron, etc., and since corundum occurs so plentifully,
the question is often asked: why is it not used more ex-
tensively? This is at best a difficult question to answer,
but we may throw some light on the subject by considering
some facts that exist concerning the corundum industry.
To begin with, the older methods of preparing the abrasive
for the market were unsatisfactory; this resulting in an
imperfectly cleaned grain not wholly free from impurities,
for it is only within the. last few years, comparatively speak-
26
31.
CORUNDUM
ing, that modernappliances, such as used at the Canadian
mines, have been installed in this country.
In the old process of cleaning, the ore was crushed in rock
crushers and then re-crushed by passing it between a series
of rolls. The resulting grain was then washed in running
water, the corundum, being the heaviest, settled while the
lighter impurities were carried away. This, of course,
applied only to such substances as were not attached to
the grains of corundum themselves. The material was then
"scoured" by passing it through a machine not unlike a
screw conveyor and afterward re-washed. The grain then
received a further cleaning in a wet pan muller, which
consists of a revolving pan having a shaft over it carrying
two wooden rollers. The action of the muller caused the
grains to rub against each other, thus gradually wearing
away the impurities which were carried away by a stream
of running water. The material was then thoroughly dried
and sieved to the various commercial sizes.
The old process was expensive and uncertain as to re-
sults. Again, severe competition with artificial abrasives
began to creep in. The Carborundum Company was spend-
ing large sums of money int'oducing their product to the
manufacturing world and the Norton Company was not
far behind in extolling the merits of their artificial corundum
called Alundum. That it pays to advertise is an old and
true saying and artificial abrasives certainly have had the
advantage of wide publicity. Again, the artificial abrasives
were uniform, whereas corundum, when taken as a whole,
was not, since it was the product of many deposits, which
naturally varied to some extent.
It is the writer's opinion, given for what it is worth, that
corundum as an abrasive has been handled wrong from the
start. It has always been sold as a raw material, in com-
petition with emery at first and later in competition with
the artificial abrasives. The miners of corundum, even of
the very best qualities, were more than willing to sell their
product to all who wished to purchase, regardless of the
27
32.
ABRASIVES AND ABRASIVEWHEELS
fact that not all manufacturers, a few years ago, knew how
to make the best quality of grinding wheels.
The writer fully realizes that it is a simple matter to say,
"I told you so," but, nevertheless he ventures the opinion
that if, upon the discovery of an exceedingly good quality
of corundum, the mine owners had gone into the wheel-
making business, absolutely controlling the sale of their
product and keeping the same up to a high standard, the
story of corundum could have been written differently at
the present time.
As a means of verifying the above statement, let us con-
sider The Carborundum Company for a moment. Suppose
they had been willing to sell their product to all wheel
manufacturers who cared to purchase. Would the carbo-
rundum grinding wheel hold the high position that it does
at the present day? Decidedly not. Carborundum wheels
of all kinds, good and bad, would have been on the market
and the result would have been that carborundum would
have lost favor in a great many cases.
Now it is a far easier matter to make a poor grinding
wheel than it is to produce a good one and here we have
the answer regarding corundum, an abrasive occurring
abundantly and possessing the highest abrasive qualities,
which now occupies an inferior position simply because
"too many cooks spoiled the broth." Everybody had
corundum wheels for sale wheels made of pure corundum
certainly. At the same time, however, some of this
"pure" corundum was unfit for wheel manufacture, while
in other cases corundum of the highest grade was given a
bad name because the actual value of the abrasive was
hidden in a poorly made grinding wheel.
How, then, should corundum have been handled? some
one is sure to ask. The answer is simple. As before stated,
the owners of a good corundum deposit should have en-
gaged in the wheel-making end of the business, given their
brand of corundum a good name, spent a hundred thousand
dollars in equipment, and several hundred thousand more
28
33.
DIAMOND
in advertising theirproduct, and the business would have
developed itself. The sole ownership of a widely advertised
product is a gold mine in itself provided, of course, the
business is properly handled, and this is one factor that
has made manufactured abrasives rth distinctive names
so universally used.
Corundum is used for a number of purposes, and, in
comparing it with emery, it is a faster cutting abrasive
owing to its pure state. Corundum wheels are used prin-
cipally for steel grinding on both 'rough and precision work,
while corundum in grain and powder form is used for vari-
ous grinding and polishing operations. Sharpening stones
made of corundum are very efficient, while corundum-
coated paper and cloth are also put to a number of uses,
principally in the form of discs used on the disc-type of
grinder for finishing steel parts, both hard and soft. Taken
as a whole, corundum covers a wide field and by many it
is considered to be the best all-round abrasive known.
DIAMOND
Diamonds are divided into three groups, the transparent
and practically flawless varieties used as gem stones and im-
perfect stones called bort diamonds. There is also a black
diamond often called carbonado. The diamond has a specific
gravity of 3.50 and is the hardest substance known, being
placed at 10 on the mineralogist's scale. The diamond
crystallizes in the cubic system, generally taking the form
of an octahedron.
The fracture of the diamond is conchoidal and the crystals
invariably cleave along planes parallel to the octahedral
faces. Diamond cutters avail themselves of this character-
istic when reducing the stone to the best shape for cutting.
Of late years, however, a sawing process has been developed
which is said to be superior to the older method of cleaving
by means of a sharp blow.
The diamond is found in India, South America, South
29
34.
ABRASIVES AND ABRASIVEWHEELS
Africa, New South Wales, Borneo, and British Guiana.
At the present time, most of the diamond industry centers
in South Africa, the mines in this locality having been
worked since 1870. Previous to this time, diamonds were
found in alluvial deposits and in conglomerates, but in
the South African mines, the most famous of which are
the Kimberley and the De Beers mines, the diamonds are
found imbedded in a kind of blue clay in what are termed
"pipes." These are supposed to be filled-up craters of
long-extinct volcanoes.
Of the origin of the diamond but little is known, although
many eminent geologists have advanced well-grounded
theories concerning its formation, but, as the original con-
dition of the carbon, of which the diamond is composed,
remains a question, the genesis of the diamond is still un-
solved.
The De Beers Company mine many hundred thousand
dollars' worth of diamonds weekly and it is needless to state
that operations are conducted on a large scale, under the
supervision of the most able mining engineers available.
To get at the diamond-bearing blue clay, a shaft is sunk
several hundred feet into the earth just outside the pipe,
tunnels from this shaft running into the diamond-bearing
deposits. This material is hoisted to the ground above,
where it is spread out in large fields to allow the sun and
rain to crumble it to the extent of being easily washed.
This weathering process is materially aided by going over
the deposits occasionally with steam-plows.
The disintegrated soil is next washed in shallow cylin-
drical troughs wherein the diamonds are swept to the rim
by means of revolving toothed arms, the lighter material
escaping at the center. The findings are now concentrated
to separate the diamonds from hard foreign substances
and then a further separation is effected by passing the
concentrates over a greased surface. For some unaccount-
able reason, the greased surface holds the diamonds while
the other worthless materials escape.
30
35.
DIAMOND
It takes, onan average, four tons of blue ground to yield
one carat weight of diamond, and as the De Beers mines
often yield from three to four pounds of diamonds a day, it
is seen that an immense amount of blue ground has to be
worked.
The next step, and a very interesting one, is to sort out
the diamonds both for color and purity. The color runs
from clear white to black, a pale yellow being the most
common color. The only difference between a gem stone
and a bort diamond is that the former is practically flaw-
less and of good color, while the latter contains black specks
and other flaws, has no brilliancy and possesses an irregular
fracture.
It is needless to state that the diamond sorters are expert
at their work and they never let a gem stone pass for a bort.
As a matter of fact, dealers in bort stones look in vain for
a gem stone that might have missed the eye of the inspector,
but there is no record of their efforts being rewarded.
Aside from truing grinding wheels, bort diamonds are
used for many other purposes. In powdered form, they
are used for diamond cutting, this process being introduced
by L. von Berquen in the year 1476, for cutting and drilling
very hard substances, for certain kinds of delicate lapping
and grinding in watch factories and occasionally for very
minute turning operations in the watch or jeweler's lathe.
The process of converting bort diamonds into diamond
powder is simple, being carried out as follows: Several
bort stones are first crushed in a little mortar made especially
for this purpose and the material thus obtained is placed
in a quantity of the very best olive oil. The mixture is
thoroughly stirred and allowed to stand for five minutes.
The oil is then poured off and the diamond powder that
remains in the vessel is called No. o. The oil is now allowed
to stand for ten minutes and again poured off, the remain-
ing powder being known as No. i. To get the various
grades, the time limits used are shown in the accompanying
table.
36.
ABRASIVES AND ABRASIVEWHEELS
Five minutes ...................... No. o
Ten minutes ....................... No. i
Thirty minutes .................... No, 2
One hour .......................... No. 3
Two hours ..... ................... No. 4
Ten hours ......................... No. 5
The oil is now allowed to stand until it shows clear, the
particles settling at the bottom being known as No. 6.
Carbonado, often called black diamond, is a form of
diamond found in Brazil, South America. It is of irregular
form and of a black, gray or brown color. It possesses no
cleavage and breaks with a granular fracture. Its specific
gravity is less than that of the true diamond. It is found
almost exclusively in the state of Bahia in what is called
cascalho, or diamond-bearing gravel. It is generally found
in small pieces, although occasionally a large piece is dis-
covered, the largest on record having a weight of 3,150
carats.
For truing grinding wheels, carbonado is superior to bort
diamond owing to the fact that absence of cleavage makes
the stone less liable to fracture. Thus carbonado is the
ideal form of diamond to use in rock drills and diamond
saws where the stone must withstand the impact of re-
peated shocks that would speedily ruin a bort stone.
GARNET
The name garnet is applied to a group of very closely
related minerals, some of which, in the pure varieties, are
used as gem stones. There are six kinds of garnet known
as follows:
Lime alumina garnet
Lime iron garnet
Lime chrome garnet ...................... Ca3 Cr2Si3Oi2
Magnesia alumina garnet
Iron alumina garnet
Manganese alumina garnet
Garnet crystallizes in the cubic system, generally in
rhombic dodecahedra. It possesses an imperfect cleavage,
32
37.
GARNET
the parting linesrunning parallel to the dodecahedron.
Its hardness varies from 6.5 to 7.5 while its specific gravity
also varies to quite an extent, in different specimens running
from 3.4 to 4.3.
Garnet has been found in crystalline schists, gneiss, gran-
ite, metamorphic limestone, serpentine and volcanic rocks.
In this country, deposits are located in New York, New
Hampshire, Connecticut, Pennsylvania and North Caro-
lina. Large quantities of garnet are mined in New York
state, the deposits being located in the vicinity of the
Adirondack Mountains. This garnet, which occurs in
limestone and gneiss, is of the iron-alumina variety. It is
often called Almandine. The garnet of New Hampshire is
also of the above variety while North Carolina garnet occurs
in two forms, the iron-alumina and a subdivision called
rhodolite, which consists of two parts magnesia alumina and
one of iron-alumina garnet.
An excellent garnet, known to the trade as Spanish
mineral, is mined in Spain. This material is extensively
used in this country; in fact, one large manufacturer of
garnet paper uses it exclusively. There are no analyses on
record to establish the composition of this material, although
The United States Geological Survey informed the writer
that it is probably an iron-alumina garnet, or almandine.
Garnet is prepared for abrasive uses by crushing, concen-
trating and magnetic separation to remove the superfluous
iron oxide, after which it is graded into various commercial
sizes. As an abrasive for smoothing wood, garnet paper
and cloth enjoys great popularity, showing high efficiency
over ordinary sandpaper, especially on comparatively hard
woods, such as oak, cherry, maple, etc. It is not a suitable
abrasive for grinding-wheel manufacture, owing to its soft
nature, although it is sometimes mixed with corundum
in the manufacture of silicate wheels for such operations as
knife grinding.
The pure varieties of garnet are often cut as gem stones of
which there are many colors from deep red to light rose.
33
38.
ABRASIVES AND ABRASIVEWHEELS
Some of the finest garnet gem stones are found in loose
gravel in Macon County, N. C.
QUARTZ
Quartz is one of the most common of minerals and has
a wide distribution throughout the world. It is composed
of silicon dioxide, or silica SiO2 . Aside from being an
essential constituent of some igneous rocks, as granite, it
occurs as sand and in crystals. Its specific gravity is
2.65 while its hardness is placed at 7 on Moh's scale. It
crystallizes in the trapezohedral-hemihedral class of the
rhombohedral division of the hexagonal system. In its pure
state, it forms many semi-precious stones such as the
amethyst, bloodstone, sardonyx and others. It has no
true cleavage and breaks with a conchoidal fracture.
As an abrasive, quartz has many uses. In grain form,
large quantities of it are used for plate-glass grinding and
in other forms of glass work. Glued on belts, it is used
for sanding implement and tool handles. Owing to its
hardness and sharpness, it is often used for sand blasting.
For sawing stone of the softer varieties, such as marble and
limestone, quartz forms a cheap and efficient medium. It
is not adapted to grinding-wheel manufacture although
it is sometimes mixed with other abrasives in making knife-
grinding wheels.
FLINT
Flint is a very hard, brown-colored stone being composed
principally of silica and having a specific gravity of 2.6.
Its fracture is conchoidal. It is one of the oldest known
minerals, being used by prehistoric man in the manufacture
of implements and weapons. It was once widely used for
striking fire and until the invention of the percussion cap
the flint-lock musket was used the world over. Thus it is
seen that this now little used material once played an
important part in shaping the destinies of nations. A
34
39.
NATURAL SHARPENING STONES
formof flint called flint-quartz is used in making the flint
paper of commerce which is more commonly spoken of as
sand-paper. In this country, the material in question is
mined in several places, the more important deposits being
in Maine, Maryland and Wisconsin.
NATURAL SHARPENING STONES
Under this heading are included all the natural stones
used, as hand stones, hones, etc., for various sharpening
operations. Sharpening stones are of very ancient origin,
specimens having been unearthed in Egypt dating back to
1500 B. c. Pliny, ^writing early in the Christian era, tells
of a stone from Crete used with oil and one from Naxos
used with water. The latter, in all probability, was noth-
ing more or less than a fragment of emery ore. The oldest
natural stone of modern civilization is the Turkey stone
mined in Asia Minor. This stone became popular over
one hundred years -ago and to some extent is used at the
present day. Other famous sharpening stones of a century
ago were the Belgian razor hone, which owes its abrasive
qualities to minute particles of garnet, and the German
water hone. Both of these stones are sold at the present
time.
The well-known Arkansas and Ouachita (Washita) stones
were discovered in Arkansas in the year 1815. These are
found in the foot-hills of the Ozark Mountains. There are
two varieties of Arkansas stones; hard Arkansas and soft
Arkansas. The former consists of 99^ per cent, pure
silica, being composed of very small particles of hexagonal-
shaped crystals to which it owes its cutting qualities.
This stone is widely used by watchmakers, engravers, tool-
makers, etc., for putting a very fine edge on cutting tools.
Soft Arkansas stones, although not as hard as the former
variety, are freer cutting, therefore they are the choice of
the carpenter, cabinet maker and pattern maker for putting
the correct cutting edge on chisels, plane irons, etc.
35
40.
ABRASIVES AND ABRASIVEWHEELS
Another famous natural stone is the Indian Pond scythe
stone, discovered in New Hampshire in the year 1821.
Upon this discovery was founded the well-known business
of the Pike Manufacturing Company, whose goods are
known to mechanics throughout the world. Several grades
of fine sandstone are used in making sharpening stones
for various purposes, scythe stones, axe stones, etc., large
deposits being located in Ohio. As a matter of fact, this
state furnishes many varieties of natural sharpening stones
such as the Hindustan, Queer Creek arid Chagrin Falls
brands. These are all excellent stones and find a ready
market for purposes to which they are adapted.
TRIPOLI
Tripoli is a trade name given to a yellowish abrasive
material which results from the leaching of calcareous
material from limestones and cherts. This material is also
often called rotten stone. It is found principally in Illinois
and Missouri. For abrasive purposes, it is used principally
for "cutting down" before polishing soft metals. It is put
on the market in the form of cakes, being mixed with tallow
and compressed.
PUMICE
Pumice is of volcanic origin, being an igneous rock which
was cooled so quickly that it did not have time to crystallize.
It sometimes contains impurities, such as feldspar and
hornblende, which diminish the general value of the
material as an abrasive, as the impurities leave deep scratches
owing to their hard nature. Natural pumice is found in
California, Kansas, Nebraska, Idaho, South Dakota and
Utah in this country while much of the imported article
conies from various islands in the Mediterranean Sea.
As an abrasive, pumice is used principally for very fine
varnish rubbing and in the manufacture of metal polishes.
36
41.
CHAPTER TWO
ARTIFICIAL ABRASIVES
Variousartificial abrasives Their physical and chemical properties Their
commercial application Methods and processes employed in the pro-
duction of artificial abrasives Carborundum Alundum Aloxite Boro-
Carbone Oxalumina Adamite Crystolon, etc. Relative hardness and
abrasive efficiency of various materials Artificial production of precious
stones Their abrasive properties Other artificial abrasives and their
production Experimental work Electro-thermic processes Production
of rouge and crocus Diamonds and crushed steel Angular grit.
UNDER
this heading can be included all grinding and
polishing materials produced by the arts of man; the
most commonly used being divided into two classes, carbide
of silicon abrasives, the original of which is Carborundum,
and artificial corundum, which material, in the form of
precious stones, has been made for more than seventy years.
In reality, the artificial corundum of today, sold under va-
rious trade names, such as Aloxite, Alundum, Boro-Carbone,
Oxalumina, etc., is an indirect outgrowth of the experiments
of other days, wherein scientific investigators had to con-
tent themselves with making artificial rubies and sapphires,
while vainly striving to produce the artificial diamond.
To class rouge and crocus as abrasives may seem rather
far fetched on first thought, but it must be borne in mind
that while these materials are used for polishing purposes
only, their mission is accomplished through abrasion, since
the finest mechanically finished surface possible to produce,
when viewed under a powerful microscope, is seen to consist
of a multitude of fine scratches.
Crushed steel and chilled iron are abrasives in the true
sense of the word. The former is used for grinding and the
37
42.
ABRASIVES AND ABRASIVEWHEELS
latter for sand blasting, which is a process of removing
superfluous material by abrasive action.
Carborundum is undeniably the best known and, for
many purposes, the most useful of all the artificial abrasives;
indeed, it is often called the father of them all, since its
introduction into the mechanical world gave electro-
chemical engineers an impetus to produce competitive
material.
For the sake of clearness, the various well-known artificial
abrasives will be considered in chronological order, Car-
borundum being at the head of the list as it was the first
artificial abrasive to be recognized commercially.
CARBORUNDUM
Carborundum is a trade name given to carbide of silicon,
a substance discovered during the year 1891 by Edward G.
Acheson. It can truly be called the most unique of all
abrasives as it has never been found in nature, therefore
it is not an imitation of nature's work, but a distinct creation
in a class by itself. It is a chemical combination of the
two elements carbon and silicon, its chemical formula
being SiC.
The raw materials entering into the manufacture of
Carborundum are coke, sand, salt and sawdust. Coke
supplies the element carbon, while the element silicon is
derived from the sand. The object of the sawdust is simply
to make the mass porous, thereby permitting the gases
generated during the burning operation a free passage to
the open air. The object of the salt is to eliminate im-
purities such as iron, etc. As the salt volatilizes; it im-
pregnates the whole mass, taking up impurities in the form
of chlorides.
The Carborundum furnaces used at the present time are
fifty feet long, ten feet wide, and five feet high. The
original furnaces, however, were somewhat smaller. Both
types are of open construction, the sides and ends being
43.
CARBORUNDUM
built of brick.The end walls are approximately two feet
thick, through which run the terminals for the electric cur-
rent. These terminals are made of carbon rods three feet
long and three inches in diameter, arranged parallel in
bundles of sixty, the spaces between the rods being packed
tightly with graphite. At the outer ends of the rods,
copper terminals are let in, which, in turn, are connected
to a large copper cap. Current is supplied by means of
cables from overhead bus bars.
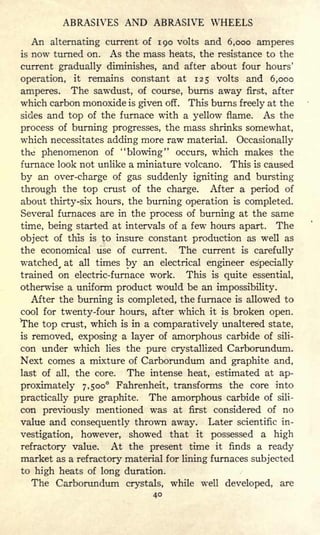
In charging the Carborundum furnaces preparatory to
burning, a mixture of thirty-four parts coke, fifty-four
Fig. i. Carborundum furnace charged with raw material, ready for burning.
parts sand, ten parts sawdust and two parts salt is used.
The materials are thoroughly mixed and brought to the
furnaces by means of mechanical conveyors. Enough of
this mixture is placed in the furnace to bring the upper
layer level with the ends of the electrodes. A trench is now
made between the terminals, wherein a core of granulated
coke is laid. The object of the coke is to allow a free pas-
sage for the electric current. More of the material is now
introduced and built up in the form of a mound as shown
in Fig i.
39
44.
ABRASIVES AND ABRASIVEWHEELS
An alternating current of 190 volts and 6,000 amperes
is now turned on. As the mass heats, the resistance to the
current gradually diminishes, and after about four hours'
operation, it remains constant at 125 volts and 6,000
amperes. The sawdust, of course, burns away first, after
which carbon monoxide is given off. This burns freely at the
sides and top of the furnace with a yellow flame. As the
process of burning progresses, the mass shrinks somewhat,
which necessitates adding more raw material. Occasionally
the phenomenon of "blowing" occurs, which makes the
furnace look not unlike a miniature volcano. This is caused
by an over-charge of gas suddenly igniting and bursting
through the top crust of the charge. After a period of
about thirty-six hours, the burning operation is completed.
Several furnaces are in the process of burning at the same
time, being started at intervals of a few hours apart. The
object of this is to insure constant production as well as
the economical use of current. The current is carefully
watched, at all times by an electrical engineer especially
trained on electric-furnace work. This is quite essential,
otherwise a uniform product would be an impossibility.
After the burning is completed, the furnace is allowed to
cool for twenty-four hours, after which it is broken open,
^he top crust, which is in a comparatively unaltered state,
is removed, exposing a layer of amorphous carbide of sili-
con under which lies the pure crystallized Carborundum.
Next comes a mixture of Carborundum and graphite and,
last of all, the core. The intense heat, estimated at ap-
proximately 7,500 Fahrenheit, transforms the core into
practically pure graphite. The amorphous carbide of sili-
con previously mentioned was at first considered of no
value and consequently thrown away. Later scientific in-
vestigation, however, showed that it possessed a high
refractory value. At the present time it finds a ready
market as a refractory material for lining furnaces subjected
to high heats of long duration.
The Carborundum crystals, while well developed, are
40
45.
CARBORUNDUM
not regular inappearance, some being hexagonal and others
rhombohedral. The crystals have no lines of cleavage,
breaking with a distinct crystalline fracture, invariably
leaving sharp cutting edges.
Carborundum crystals are of various colors, being truly
beautiful from an artistic point of view; coal black, deep
brown, light green, pale blue, deep blue a'nd purple are all
intermingled in a gorgeous riot of colors seldom equaled in
nature. In the early days of the industry, green Carbo-
rundum predominated and at present many are of the opin-
ion that green Carborundum is superior in cutting qualities
to specimens of other colors. Actual tests, however, con-
ducted by abrasive engineers, have proven beyond all reason-
able doubt that the above theory is absolutely groundless,
the color being the result of oxidation.
On Moh's scale of hardness, Carborundum is placed be-
tween nine and ten. It is probably nearer ten than nine
as Carborundum has been known to scratch rubies, sapphires,
and diamonds. Compared with other abrasives, Carbo-
rundum is comparatively light, its specific gravity being
approximately 3.18. This factor should not be under-
estimated since the centrifugal force of a revolving body
is proportional to the square of the velocity. Thus, wheels
running at the high speeds recommended in present-day
grinding practice are under a severe centrifugal strain,
and it is apparent that the lightest abrasive makes the safest
wheel.
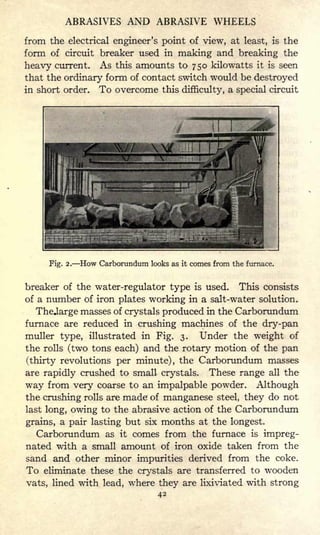
Fig. 2 gives a good idea of the appearance of Carborundum
as it comes from the furnace, the photograph being taken
after the outer layers and core had been removed. As this
material looks like the products of the mine and quarry, the
question is sometimes asked, "Why is carbide of silicon not
found in nature?" The only reasonable answer the writer
can give is that the degree of heat at which both carbide of
silicon and graphite are formed is so near the same temper-
ature that nature seemed content to produce graphite alone.
An interesting feature of the production of Carborundum,
41
46.
ABRASIVES AND ABRASIVEWHEELS
from the electrical engineer's point of view, at least, is the
form of circuit breaker used in making and breaking the
heavy current. As this amounts to 750 kilowatts it is seen
that the ordinary form of contact switch would be destroyed
in short order. To overcome this difficulty, a special circuit
Fig. 2. How Carborundum looks as it comes from the furnace.
breaker of the water-regulator type is used. This consists
of a number of iron plates working in a salt-water solution.
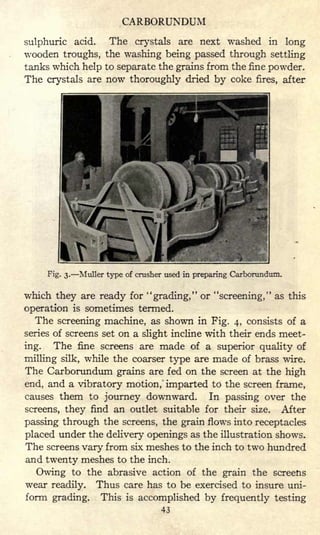
Thejarge masses of crystals produced in the Carborundum
furnace are reduced in crushing machines of the dry-pan
muller type, illustrated in Fig. 3. Under the weight of
the rolls (two tons each) and the rotary motion of the pan
(thirty revolutions per minute), the Carborundum masses
are rapidly crushed to small crystals. These range all the
way from very coarse to an impalpable powder. Although
the crushing rolls are made of manganese steel, they do not
last long, owing to the abrasive action of the Carborundum
grains, a pair lasting but six months at the longest.
Carborundum as it comes from the furnace is impreg-
nated with a small amount of iron oxide taken from the
sand and other minor impurities derived from the coke.
To eliminate these the crystals are transferred to wooden
vats, lined with lead, where they are lixiviated with strong
42
47.
CARBORUNDUM
sulphuric acid. Thecrystals are next washed in long
wooden troughs, the washing being passed through settling
tanks which help to separate the grains from the fine powder.
The crystals are now thoroughly dried by coke fires, after
Fig. 3. Muller type of crusher used in preparing Carborundum.
which they are ready for "grading," or "screening," as this
operation is sometimes termed.
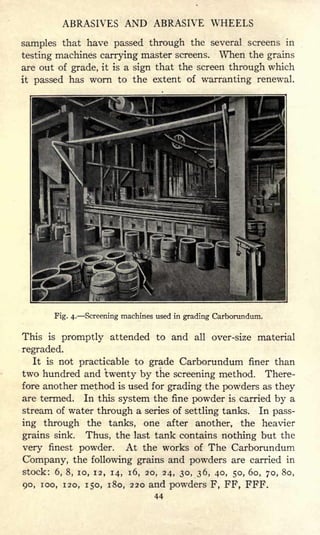
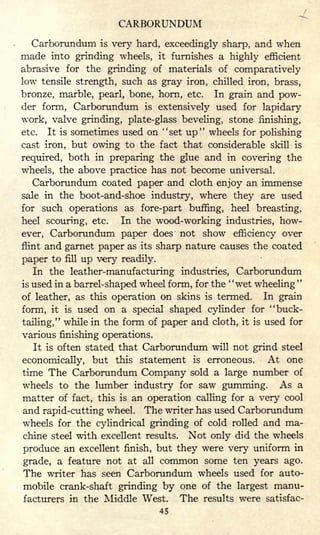
The screening machine, as shown in Fig. 4, consists of a
series of screens set on a slight incline with their ends meet-
ing. The fine screens are made of a superior quality of
milling silk, while the coarser type are made of brass wire.
The Carborundum grains are fed on the screen at the high
end, and a vibratory motion, imparted to the screen frame,
causes them to journey downward. In passing over the
screens, they find an outlet suitable for their size. After
passing through the screens, the grain flows into receptacles
placed under the delivery openings as the illustration shows.
The screens vary from six meshes to the inch to two hundred
and twenty meshes to the inch.
Owing to the abrasive action of the grain the screens
wear readily. Thus care has to be exercised to insure uni-
form grading. This is accomplished by frequently testing
43
48.
ABRASIVES AND ABRASIVEWHEELS
samples that have passed through the several screens in
testing machines carrying master screens. When the grains
are out of grade, it is a sign that the screen through which
it passed has worn to the extent of warranting renewal.
Fig. 4. Screening machines used in grading Carborundum.
This is promptly attended to and all over-size material
regraded.
It is not practicable to grade Carborundum finer than
two hundred and twenty by the screening method. There-
fore another method is used for grading the powders as they
are termed. In this system the fine powder is carried by a
stream of water through a series of settling tanks. In pass-
ing through the tanks, one after another, the heavier
grains sink. Thus, the last tank contains nothing but the
very finest powder. At the works of The Carborundum
Company, the following grains and powders are carried in
stock: 6, 8, 10, 12, 14, 16, 20, 24, 30, 36, 40, 50, 60, 70, 80,
90, 100, 120, 150, 180, 220 and powders F, FF, FFF.
44
49.
CARBORUNDUM
Carborundum is veryhard, exceedingly sharp, and when
made into grinding wheels, it furnishes a highly efficient
abrasive for the grinding of materials of comparatively
low tensile strength, such as gray iron, chilled iron, brass,
bronze, marble, pearl, bone, horn, etc. In grain and pow-
der form, Carborundum is extensively used for lapidary
work, valve grinding, plate-glass beveling, stone finishing,
etc. It is sometimes used on "set up" wheels for polishing
cast iron, but owing to the fact that considerable skill is
required, both in preparing the glue and in covering the
wheels, the above practice has not become universal.
Carborundum coated paper and cloth enjoy an immense
sale in the boot-and-shoe industry, where they are used
for such operations as fore-part buffing, heel breasting,
heel scouring, etc. In the wood-working industries, how-
ever, Carborundum paper does not show efficiency over
flint and garnet paper as its sharp nature causes the coated
paper to fill up very readily.
In the leather-manufacturing industries, Carborundum
is used in a barrel-shaped wheel form, for the "wet wheeling
"
of leather, as this operation on skins is termed. In grain
form, it is used on a special shaped cylinder for "buck-
tailing," while in the form of paper and cloth, it is used for
various finishing operations.
It is often stated that Carborundum will not grind steel
economically, but this statement is erroneous. At one
time The Carborundum Company sold a large number of
wheels to the lumber industry for saw gumming. As a
matter of fact, this is an operation calling for a very cool
and rapid-cutting wheel. The writer has used Carborundum
wheels for the cylindrical grinding of cold rolled and ma-
chine steel with excellent results. Not only did the wheels
produce an excellent finish, but they were very uniform in
grade, a feature not at all common some ten years ago.
The writer has seen Carborundum wheels used for auto-
mobile crank-shaft grinding by one of the largest manu-
facturers in the Middle West. The results were satisfac-
45
50.
ABRASIVES AND ABRASIVEWHEELS
tory, Carborundum being preferred to all other makes of
wheels.
It must be considered that the above instances happened
some years ago, before the high development and accurate
grading of manufactured alumina abrasives, which at the
present time show higher efficiency on steel grinding than
is possible to attain with Carborundum. The above state-
ments are made simply to show that at one time in the his-
tory of grinding, Carborundum held its own on steel.
Why, then, does not Carborundum, which is acknowledged
to be the hardest and sharpest of all abrasives, both natural
and artificial, show high efficiency on steel grinding? This
is, at best, a hard question to answer and one upon which
opinions are at great variance. The writer's opinion, based
upon many years of observation, close study, and prac-
tical application, is that if Carborundum was not quite so
hard, and broke with a conchoidal instead of a crystalline
fracture, it would eventually drive the alumina abrasives
out of the market.
The above opinion can be called pure speculation without
a suitable hypothesis, therefore it is open to question.
However this may be, it is set down for what it is worth,
for opinions, no matter how theoretical they may appear,
possess some merit, at least until they have been dis-
proved by actual demonstration, and as it is an impossi-
bility to produce the type of Carborundum described, the
above theory may be as rational as any other.
The name Carborundum is registered as a trade mark,
thus it is the sole property of The Carborundum Company.
It, however, grinding wheels are made of Carborundum,
no matter by whom, they can lawfully be sold as genuine
Carborundum wheels.
OTHER CARBIDE OF SILICON ABRASIVES
A carbide of silicon abrasive called
"
Carbosolite
"
is made
in Germany. It has been sold in this country to a limited
46
51.
ARTIFICIAL CORUNDUM
extent, chieflyin the granite-finishing business. It is
mostly of a dark-gray color and it is not considered as pure
as Carborundum. Aside from the granite trade, a limited
amount of this material is made into grinding whe^s.
Crystolon is a trade name given to a carbide of silicon
abrasive made by Norton Company at their electric-
furnace plant in Chippawa, Canada. It is made by practi-
cally the same method used in producing Carborundum;
the same raw material forming the ingredients. It was
first puu on the market about seven years ago, and at
the present time it enjoys a large sale, both in the form of
wheels and grain.
The Abrasive Company of Philadelphia market grinding
wheels made of carbide of silicon, calling the same "Elec-
trolon." This material is an electric-furnace product, being
made of selected materials, the grain being specially treated
before being incorporated into grinding wheels/ This ma-
terial was first put on the market during the year 1914
and it is considered by many large consumers of grinding
wheels to be a very efficient abrasive.
ARTIFICIAL CORUNDUM
As stated at the beginning of this chapter, artificial
corundum has been produced for more than seventy years
and in considering the subject in the abstract, a little light
thrown on the experimentalists of other days may not be
out of place at the present time.
It is a well-known fact among those conversant with the
values of precious stones that a true Oriental ruby, of fine
color and flawless, is worth more, carat for carat, than
the finest diamonds of Brazil or South Africa. The term
ruby is often misconstrued to embrace the spinel or balas
ruby. Indeed, the famous "ruby" set in the Maltese cross
in front of- the imperial state crown of England is in reality
a spinel. It is, of course, possible for experts to readily
distinguish the difference between true and spinel rubies, but
47
52.
ABRASIVES AND ABRASIVEWHEELS
since the ruby is nothing more or less than pure crystallized
alumina, colored with a small quantity of chromium, it is
evident that a laboratory product of the above materials
is a true synthesis of the ruby. It is as much entitled to the
name as the choicest specimens of nature from the Mandalay
district of Upper Burma, where the finest rubies have been
found.
In the year 1837, M. A. A. Gaudin successfully made
true rubies by fusing alum in a carbon crucible at a very
high temperature, a little chromium being added to impart
the desired color. The rubies, while of a very small size,
hardly visible to the naked eye, proved that it was within
the means of science to produce corundum artificially.
J. J. Ebelmen's experiments during the year 1847 resulted
in the artificial production of the white sapphire and rose-
colored spinel. The process consisted of fusing the desired
constituents at high temperature in boracic acid. He also
produced the ruby by using borax as a solvent.
Not until the year 1877, however, was it proved possible
to produce crystallized artificial alumina of a size suitable for
cutting into small stones, the process being the result of
experiments on the part of E. Fremy and C. Feil. The
process used was as follows :
By the fusion of lead oxide and
alumina in a fire-clay crucible, lead aluminate was formed.
Silica enters into the composition of fire clay, and under
the influence of high temperature, the silica of the crucible
gradually decomposes the lead aluminate, forming lead
silicate, which remains in a liquid state while the alumina
crystallizes as white sapphire. By mixing in a small amount
of chromium, rubies were formed. The experiments of
Sainte-Claire Deville, Caron, Eisner, Debray, and De
Senarmont, too lengthy to be described fully here, did
much toward reducing the art of producing artificial corun-
dum to an exact science.
So much for the experimentalists of other days. They
did not attempt to produce artificial corundum for abrasive
purposes, to be sure, such a possibility being undreamed of
48
53.
ARTIFICIAL CORUNDUM
in theirday. The fact remains, however, that their investi-
gations were of value as by their means it was shown con-
clusively that it was possible to produce artificial corundum.
One of the first inventors to achieve success in the manu-
facture of an artificial abrasive of the alumina type was
Franz Hasslacher of Frankfurt-on-Main, Germany. As
stated elsewhere, emery contains a high percentage of iron
oxide, which possesses no abrasive value, and aside from this
fact most specimens of emery are hydrous, often containing
as high as 5 per cent, of combined water, which causes trouble
in the kilns where wheels, in which this emery is incor-
porated, are made by the vitrified process. The above-
named inventor was granted a patent for changing natural
emery into iron-and-water-free corundum (German patent
No. 85,021, issued Nov. 20, 1894), the method of procedure
being as follows:
Crushed emery ore and charcoal or coke are first mixed
together, the percentage of the latter being equal to the
proportion of iron oxide contained in the emery ore. This
mixture is then placed in an electric furnace, an illustration
of which is shown in Fig. 5. The furnace consists of fire-
brick walls (A) , supported by the uprights (H) ,
the electric
current being transmitted by the carbons (C) .
In charging the furnace the opening at the bottom (D)
is closed by means of a glass plate (P) and the furnace filled
with the emery-and-coke mixture until the top of the mass
is level with the center of the carbons. The carbons are
placed about i-> inches apart, the space between them
being packed with a few lumps of coke. The furnace is
now completely filled and heaped up as shown at (S).
An alternating current of 300 amperes at a pressure of
no volts is now turned on, under the influence of which
the pieces of coke between the carbons are brought up to
incandescence, which causes the surrounding emery to
assume a molten state. The pieces of coke are soon ab-
sorbed and an electric arc established between the terminals,
the presence of which is proven by a loud buzzing sound.
49
54.
ABRASIVES AND ABRASIVEWHEELS
Carbon monoxide gas escapes through the mass, burning
with a blue flame. The presence of this gas indicates that
the iron oxides are in the process of reduction. A large
mass of molten emery soon forms about the electrodes,
Fig. 5. Hasslecher's furnace for making artificial corundum.
the furnace walls being protected by the surrounding, un-
melted material as the illustration shows. When a suf-
ficient amount of emery has been melted, the glass plate
fuses, causing the emery to run through to the floor in a
dazzling, white-hot stream.
At this point, the top crust is broken in, whereat the
descending crust of emery cools the molten emery around
the opening, causing the same to close. The furnace is
then charged again and the process continued. In about
fifteen minutes, the molten emery again breaks through.
Thus the process can be continued as long as convenient.
The resulting product is fairly well crystallized alumina,
running from white to blue in color, possessing a luster
not unlike that of quartz. This material, being free from
iron, possesses a higher abrasive efficiency than emery
and for some purposes it gives excellent results. It has been
5
55.
ARTIFICIAL CORUNDUM
used inthis country to quite an extent, but at the present
time, and in fact for the last fifteen years, it has not been able
to successfully compete with American-made products.
Another process for making artificial alumina was patented
by Dr. G. Dollner of Rixdorf, Germany (German patent
No. 97,408, issued Feb. 28th, 1897). The method is quite
simple and easily carried out, consisting of mixing crushed
aluminum with oxides, peroxides and other metallic com-
pounds with oxygen. This mixture, when ignited, owing to
the high combustion temperature of aluminum, reacts in an
endothermic manner causing the formation of oxide of alumina.
This phenomenon is accompanied by the separation of the
metals, the oxides and peroxides of which were used.
In the reaction, the oxide of alumina is brought to a
state of fusion, and, on cooling, it is characterized by extreme
hardness. In his patent specifications, the inventor claims
that this material is of a degree of sufficient hardness to
replace diamonds for technical purposes, and further states
that it is superior to other artificial abrasives as by this
process grinding wheels can be prepared in solid blocks
that is a grinding wheel produced without a bonding
material. Whether or not this has been carried out suc-
cessfully the -writer cannot state. Even if it were possible,
however, such a wheel would be of one grade only, thus
its field of usefulness would be limited.
It may be well at this time to consider an abrasive called
Corubin, which is a by-product resulting from the manu-
facture of chromium by the Goldschmidt Thermit alumino-
thermic process. The above process is one for making
metallic chromium through endothermic action, the slag or
by-product of which forms an excellent abrasive material
as the following analysis shows.
Chromium 13 . 2 per cent.
SiO2 3.08
"
A12 O3 71-65
"
Fe 2.00
"
CaO Trace
MgO 1.35
"
56.
ABRASIVES AND ABRASIVEWHEELS
From the above, it is seen that this material is composed
chiefly of alumina and chromium, the percentage of alu-
mina being high enough to form an efficient abrasive, while
the amount of chromium contained renders the abrasive
very hard and tough.
In the manufacture of other metals by the Goldschmidt
Thermit process, other slags are obtained being only slightly
inferior in abrasive efficiency to Corubin. The writer is
informed on good authority that these abrasives are giving
satisfaction, owing to the fact that several thousand tons
of them are sold annually to responsible abrasive-wheel
manufacturers in this country. Large quantities of Corubin
are used abroad in the manufacture of lenses, wherein the
abrasive is used to grind the glass, and in other abrasive
work.
That the experimentalists made great strides in perfect-
ing methods for the manufacture of artificial abrasives
(after Acheson and The Carborundum Company proved to
the world that there was a ready market for an artificial
abrasive) no one will deny. The artificial corundum made
previous to the year 1900, however, was incomplete in
that it lacked what we term at the present day abrasive
temper. We all know that high-carbon steel, or tool steel
as it is called, possesses a valuable characteristic inasmuch
as it can be made exceedingly hard by heating it red hot
and suddenly cooling it by immersion in water, or a brine
solution. Further, by tempering it, or drawing the color
as the smith says, we get various degrees of temper for in-
numerable purposes; a very hard steel for razors, a some-
what softer material for machine reamers, softer still for
lathe, tools, and yet softer for cold chisels and axes.
A piece of tool steel that has been hardened but not drawn,
is very brittle, thus its field is limited. For an illustration,
a lathe tool, a pair of scissors, or an axe thus treated would
be useless the lathe tool would crumble away as soon as
it was brought in contact with the piece of work to be turned,
the scissors would break the first time they were dropped
52
57.
BAUXITE
on the floor,while the axe would fly to pieces at the first
stroke of the woodsman. Thus, it is seen, that the character-
istic of temper is what gives tool steel its immense value
in the arts and sciences.
To complete the parallel we will now consider artificial
corundum, which, as originally made, was very hard and
useful in a limited field only. It is evident that if means
could be found whereby the temper of the material in
question could be controlled, its usefulness would be in-
creased a thousandfold.
This has been successfully accomplished and the credit
is due to an American, Charles B. Jacobs (no relation to
the writer), who in the year 1900 obtained a process
patent for manufacturing an abrasive from bauxite and
tempering the same to a degree of hardness suitable for
abrasive purposes. Briefly stated, Mr. Jacobs' process con-
sists of fusing bauxite in an electric furnace of the arc type
and cooling the resultant alumina oxide in a manner to
impart the desired degree of temper.
Before considering Mr. Jacobs' process, it will be of ad-
vantage at this point to touch briefly on the material bauxite
as we will have occasion to refer to it several times later.
BAUXITE
Bauxite is a clay-like mineral, or rather a combination of
minerals, containing among other constituents alumina
oxide, iron oxide, silica and titanic acid. It is taken to be
a decomposition product of igneous rock. It was first dis-
covered in France as long ago as the year 1821 by P.
Berthier, who called it alumina hydratee de Beaux. The
present name of bauxite was given to the material in ques-
tion by E. H. Sainte-Claire Deville in 1861. The name
was derived from the village of Les Beaux in Southern
France where the material was first observed.
Bauxite is never found in a crystallized state, but always
as a clay-like earth. Its color varies from light yellow to
53
58.
ABRASIVES AND ABRASIVEWHEELS
deep red. The material, while always impure, contains a
high percentage of alumina oxide. Hence its value as a
raw material for the manufacture of an alumina abrasive
claimed the attention of abrasive manufacturers some
years ago, when a substitute for natural alumina abrasives,
that is to say emery and corundum, was seriously given
consideration.
In this country, bauxite is found in Georgia, Alabama
and Arkansas. In these localities, the material in question
is generally associated. with limestone and its origin is at-
tributed to the action of solutions of aluminum sulphate
on limestone.
CHARLES B. JACOBS' PROCESS
Mr. Jacobs' electric furnace for carrying out his process of
converting bauxite into artificial corundum is shown in
Fig. 6. It consists of a rectangular casing (i) with a slop-
ing top, at the apex of which is an opening (2) which serves
the double purpose of charging the furnace and carrying
off the volatile matter of the charge. The furnace casing
is constructed with a sheet-iron shell (3) which is lined with
fire brick (4), which serves as a non-conducting material
in regard to electricity as well as heat. Next to this, are
laid carbon bricks (5).
The hearth of the furnace consists of a cast-iron plate
(6) lined first with ground lime (7) and then carbon bricks
(8) laid in the lime. The hearth is mounted on a screw
(9) by means of which it can be lowered or raised at will.
By lowering the hearth during the furnace run, in a gradual
manner, a thick body of the fused material is obtained.
Over the earth are mounted four pairs of carbon electrodes
(10) between which the electric arc is produced. The fur-
nace is supported by cast-iron legs (n). These are of suffi-
cient height to allow the hearth to be lowered clear of the
bottom of the furnace. It is seen that the two outside pairs
of electrodes are away from the furnace walls; the object
being to keep the walls clear of fused material. The hearth
54
59.
CHARLES B. JACOBS'PROCESS
Fig. 6. Jacobs' artificial corundum furnace.
55
60.
ABRASIVES AND ABRASIVEWHEELS
is left free to move up and down in the furnace. An
opening is made in one side of the furnace to permit
of inspection should occasion require and also to provide
means of introducing a stirring rod. The opening is closed
by the plug (12).
Mr. Jacobs' process of converting bauxite into artificial
corundum is as follows: The first step is to calcine the raw
material, the object of which is to drive away as much
moisture as possible. This saves undue expenditure of cur-
rent and wear on the electrodes. The hearth is now raised
until it occupies a position one inch below the electrodes,
each pair of which is placed in contact, and the furnace
filled with the calcined bauxite.' Current is now turned on
and the electrodes pulled apart, causing electric arcs to be
set up between them. The bauxite fuses under the intense
heat and the alumina contained therein runs down on the
hearth, which is lowered about two inches per hour. This
results in a quiet pool of melted alumina oxide which cools
and solidifies in crystalline form while the furnace hearth
descends. During the process of fusion, the impurities in
the raw material are volatilized, in which condition they
escape through the opening at the top of the furnace.
Regarding the temper of the material, Mr. Jacobs has
the following to say: "The nature of the product may be
varied by the slow or rapid cooling of the fused mass, so
as to obtain a product of the same degree of absolute
hardness, but of varying toughness, and consequently
varying abrasive power, by the slow or rapid lowering of
the hearth. The more slowly the product cools, the better
defined will be its crystallization and the greater its tough-
ness and abrasive power. The nature of the product may
also be varied by agitating the mass while cooling, as by a
poker or stirring rod inserted through the hole normally
closed by plug 12, and thus disturbing its natural tendency
of crystallization, producing thereby a finer grain of crys-
talline structure than when the material cools without
disturbance."
56
61.
ALUNDUM
ALUNDUM
Alundum is atrade name originated by Norton
Company and is applied to an alumina abrasive manufac-
tured under the above-described patent. However, the
process has been modified somewhat as shown by the fol-
lowing account of the same by Richard G. Williams, Me-
chanical Engineer and Special Investigator of Norton
Company, in a paper presented at the thirty-first general
meeting of the American Electrochemical Society held in
Detroit, Mich., May 2 5, 1917.
"The raw material must necessarily be a substance high
in aluminum oxide. The most satisfactory material is a
high-grade bauxite, although satisfactory abrasives are
being made from other materials, such as low-grade bauxite
and emery. Aluminous abrasives are made in the arc type
of furnace. These furnaces often consist of a wrought-iron
shell, or some form of pot, lined with carbon. The electrodes
are suspended in the pot and then lowered to the bottom
of the furnace, a train of graphite or fine coke placed be-
tween the electrodes, the current turned on and an arc
suitable for fusing is available as soon as the train of graphite
or coke has volatilized.
"Before fusion in the electric furnace, the bauxite receives
a calcining treatment to drive off 30 per cent, of combined
water. Suitable chemicals are mixed with the calcined ore
in order to facilitate the removal of such materials as iron
and silicon. Furnaces of three-ton capacity consume between
650 and 700 horse power and it takes approximately 24 hours
for a furnace run. After the run is completed, the shell
is stripped off or the furnace sides removed and the pigs
allowed to cool. When the pigs have cooled to a sufficient
temperature, they are broken up by sledge hammers into
pieces convenient for putting through a large jaw crusher.
This operation reduces the material to pieces about the
size of a man's fist, and in this condition the abrasive is
sent to the grinding-wheel factory for further treatment."
57
62.
ABRASIVES AND ABRASIVEWHEELS
Alundum, as put on the market, consists of two kinds;
ordinary Alundum and white Alundum. White Alundum
makes an almost white wheel when bonded by the silicate
process and a deep red-colored wheel when the vitrified
process is employed. White Alundum is designated by
the prefix 38. A 60 grit wheel made of white Alundum
is marked 3860. Ordinary Alundum is used for general
steel grinding on both rough and precision work, while
white Alundum is used principally for grinding such ma-
terials as high-alloy steels and general precision tool-room
grinding.
ALOXITE
Aloxite is the trade name of an alumina abrasive manu-
factured by The Carborundum Company. It is made from
bauxite in an electric furnace of the arc type. The Car-
borundum Company's Aloxite plant is located at Sarran-
colin, a small town in the province of Hautes Pyrenees in
Southern France, so as to be near an adequate supply of
the raw material. As a precautionary measure, however,
several furnaces are operated at the Niagara Falls plant.
An Aloxite furnace is quite a simple affair, consisting of
an outer shell resting on a base, and two electrodes for sup-
plying the current. The outer shell is water-cooled, but does
not have a refractory lining as the charge forms this itself.
It is placed on wheels to facilitate moving it from under
the electrodes when the burning operation is completed.
In charging the furnace, the bottom is first lined with a
mixture of carbon and tar. Next a layer of bauxite is in-
troduced and the electrodes lowered until they rest on the
bauxite. A path of graphite is now laid between the elec-
trodes, the object being to form a free passage for the cur-
rent. As soon as the charge is in a molten state, however,
it forms a good conductor in itself. The current is now
turned on and the bauxite brought to a molten state. An
alternating current of 6,000 amperes at a pressure of 100
volts is used.
58
63.
ALOXITE
As soon asthe first layer of bauxite is in a molten state,
another layer is introduced, the electrodes raised, and this
layer melted. This process is continued until the furnace
is full, which requires about thirty-six hours. During the
melting process, the oxide of iron and silicon in the raw
material unite in the form of ferro silicon, thus practically
freeing the alumina from all impurities. As a matter of
fact, Aloxite runs about 97 per cent, pure alumina. The
ferro silicon, being heavier than the alumina, sinks to the
bottom of the furnace where it is easily disposed of. Several
furnaces are operated at the same time, the object being
twofold; that is, to produce a large supply of material and
to keep the current consumption as uniform as possible.
After the furnace has cooled sufficiently, the outer shell
is removed, exposing the Aloxite ingot. Two of these are
shown in Fig. 7. The ingots are first broken into pieces
Fig. 7. Aloxite ingots as they come from the furnace.
of about fifty pounds weight by means of a heavy breaker
of the skull-cracker type. The pieces thus obtained are
next crushed in an ore crusher of the type illustrated in
Fig. 8. Two crushers are employed, the first one being set
to produce lumps about as large as a man's fist while the
second crusher breaks them still smaller. The Aloxite lumps
are now passed through a magnetic separator which re-
59
64.
ABRASIVES AND ABRASIVEWHEELS
moves any lumps of silicon which may have clung to the
ingot. A roller-type crusher is next used which completes
the crushing operation. Aloxite is screened in the same
manner as Carborundum and the numbers of the grades
and powers are identical.
Aloxite is very tough and possesses what might be termed
a well-regulated temper. The grains are hard enough to
I II
Fig. 8. Ore crushers used in preparing Aloxite.
cut rapidly, yet not so tough that they will not fracture
when dull. The temper of the grain is under control, thus
a uniform abrasive is the result. In color, Aloxite is of a
purplish blue and its formation is distinctly crystalline,
as Fig. 9 shows.
Aloxite is adapted for all kinds of steel grinding, especially
on precision work such as surface grinding, cylindrical
grinding, cutter and reamer sharpening, special grinding
operations such as crank-shaft grinding, wherein it is ab-
solutely essential that the corner of the wheel hold a well-
defined radius for some time, and for the general , grinding
of high-speed and alloy steels. As a substitute for emery
cloth, Aloxite-coated cloth has found favor with many
manufacturers of motor-cars and other products. Aloxite
60
65.
WERLEIN'S ARTIFICIAL ABRASIVE
grainis also being used for many grinding and polishing
operations heretofore done with emery grain. In the cut-
glass industry, Aloxite wheels are used for finishing the
beautiful and intricate cuts seen on the best ware, having
Fig- 9- Aloxite as it is formed in the furnace.
to a great extent taken the place of the black Craigleith
natural stones which were used for this purpose for many
years. Aloxite has been on the market since 1909.
WERLEIN'S ARTIFICIAL ABRASIVE
A comparatively recent patent (French patent No.
430,932, issued Aug. 28th, 1911) for the manufacture of an
artificial abrasive has been granted to Ivan Werlein of
Seine, France. It is an electric-furnace product composed
of alumina and silicon. In his patent specifications, the
inventor states: "This alumina and silicon compound
produced at high temperature may be obtained in various
ways. For instance, a mixture of 80 to 95 parts of alumina
and 5 to 20 parts of silicon is melted in an electric furnace.
61
66.
ABRASIVES AND ABRASIVEWHEELS
When the mass has reached about 2,888 to 3,000 C. it is
kept at that temperature for about 20 minutes and then
cooled."
The writer has never seen this abrasive, therefore he
is not in a position to comment on its merits. From its
composition, however, it would appear to have some of
the characteristics of Carborundum combined with those
of the various alumina abrasives. Just what such an abrasive
would accomplish, judging from an American efficiency
standpoint, is a question of conjecture and to the best of
the writer's knowledge, this abrasive has not as yet claimed
the attention of American abrasive engineers.
BORO-CARBONE
Boro-Carbone is an artificial alumina abrasive made in
an electric furnace of the arc type by a process somewhat
similar to that used in the manufacture of Aloxite and
Alundum. It contains a high percentage of alumina oxide
with a small amount of impurities. In color, this abrasive
varies from a milky white to a light blue and its crystal-
lization is very pronounced.
Boro-Carbone is made in France, the raw material being
bauxite, and in one respect it enjoys a unique reputation
in that it is the only foreign abrasive that has been success-
fully able to compete with American-made products. To
be sure, Aloxite might be called a foreign abrasive, but in
the strictest sense of the word, this is a fallacy, as it is a
product of American engineering talent, originating at
The Carborundum Company's Niagara Falls plant.
The sale of Boro-Carbone is controlled in this country
by the Abrasive Company of Philadelphia, Pa., to whom
is really due the credit of perfecting this abrasive to a point,
where it could compete with American-made products. It
was put on the market in 1912 and at the present time en-
joys a large sale, being adapted for all kinds of steel grinding.
The Abrasive Company state that the temper of Boro-
62
67.
OXALUMINA
Carbone can bevaried according to the kind of grinding it
is to do.
OXALUMINA
Oxalumina is a name given to a manufactured abrasive
of the artificial alumina type by. the Cortland Grinding
Wheel Corporation. Physically, it is composed of micro-
scopic crystals of alumina; chemically, it contains about
98 per cent, of aluminum oxide. It is prepared by fusing
and refining various alumina-bearing clays and ores in
carefully regulated furnaces. The resulting mass is properly
cooled, then crushed and graded for use as an abrasive.
This abrasive is widely advertised and sold in competition
with other American artificial abrasives principally for pre-
cision grinding operations.
ADAMITE
This material is an electric-furnace product made in
Austria. It contains approximately 80 per cent, alumina
oxide. It is dark blue to black in color, being of a compact,
well crystallized nature. It is a very tough abrasive and
by some American grinding-wheel manufacturers it is used
to a limited extent in the manufacture of very durable wheels.
ROUGE AND CROCUS
Both of these materials are made by the same process,
which consists of calcining sulphate of iron in crystal form.
The sulphate of iron crystals are subjected to high tempera-
ture in crucibles and the powder that forms at the bottom
is crocus, while that at the top is rouge. These materials
differ in color, rouge being red while crocus is purple.
These materials are used in buffing and polishing operations.
DIAMOND CRUSHED STEEL
This material is manufactured by the Pittsburgh Crushed
Steel Company of Pittsburgh, Pa. It is made of crucible
63
68.
ABRASIVES AND ABRASIVEWHEELS
steel, subjected to a special treatment, after which it is
crushed and graded into the following sizes: 4, 6, 8, 10,
12, 14, 16, 18, 20, 30, 36, 40, 50, 60, 70, 90, 120, 150, 170, 190,
200. The sizes from 60 to 200 inclusive are known to the
trade as Diamond Steel Emery.
The material in question is a new departure in abrasives;
a scientifically prepared material designed to replace emery
for grinding operations on granite, onyx, marble, brick,
glass, etc., or in fact for any purpose wherein an abrasive
is used in grain form. As this material has three important
characteristics; hardness, sharpness and toughness, it should
prove a very durable grinding agent in cases where a rolling
and crushing action is present.
Crushed steel is not an ideal abrasive to employ in grind-
ing-wheel manufacture inasmuch as its tough nature tends
to prevent the grains from fracturing upon becoming dull.
ANGULAR GRIT
This is another abrasive material made by the above
concern, being used in the place of sand for sand-blasting
operations. It is a crushed chilled-iron product marketed
in the following sizes :
10, 12, 20, 30, 40, 60, 90. This ma-
terial is, without doubt, an excellent medium to use for
sand blasting as the individual grains have a number of
cutting points and the material does not break away, or
pulverize, as quickly as sand, thus reducing the objection-
able factor of dust to a minimum.
69.
CHAPTER THREE
THE MANUFACTUREOF GRINDING WHEELS
Composition of grinding wheels Desirable and undesirable properties
Bonds Shellac Rubber Fusible clays Silicate of soda Vitrified
wheels Method of producing vitrified wheels Puddled process Pressed
process Silicate wheels Shellac wheels Rubber wheels Clay bond
used in vitrified wheels Choice of bonding material Wheel-turning
Kiln used Heating of kiln and work Cooling of kiln Dressing wheels
Bushing wheels Speed tests for wheels Elastic process Rubber
process.
A GRINDING wheel consists of two parts the abrasive
'f material that does the cutting and a suitable bonding
material to hold the countless grains of which the wheel is
composed in a solid mass. Grinding wheels for some pur-
poses, such as the rough grinding of heavy gray-iron cast-
ings, should be hard and compact, to resist undue wear.
A cylinder wheel designed for a vertical spindle surface
grinding machine, such as the Pratt & Whitney Company
manufacture, must be open and porous to insure free cutting.
Thus it is seen that the dressing action which a particular
work has on the wheel in any given operation must be given
consideration in the manufacturing process.
The two kinds of wheels above mentioned are at extremes,
but in the making of wheels for various other purposes,
equally important factors must not be overlooked. As an
illustration, wheels for various tool and cutter sharpening
operations must be very cool cutting, while wheels for such
special grinding operations as crankshaft finishing are re-
quired to hold their peripheral shape for a reasonable length
of time; otherwise more time would be consumed in keep-
ing them in proper condition than would be spent in actual
production.
65
70.
AB^SIVES JtfrD ABRASIVEWHEELS
Some years ago, when grinding wheels were used only
for a few simple operations such as tool sharpening and
general grinding, simple "rule of thumb" manufacturing
methods answered very well. At the present day, however,
owing to keen competition and the high standard required
by modern efficiency engineers, grinding-wheel manufac-
ture is fast becoming an exact science, as it were, wherein
the manufacturer studies the requirements of his customers
and perfects his production methods to a point where only
the highest quality of goods receive the final inspector's
approval.
When we speak of the bond of a grinding wheel, we refer
to the material used to hold the grains in the wheel together.
In the vitrified bond, the binding medium is a high grade of
kaolin, or other refractory or fusible clays, the process of
vitrification taking place in a kiln patterned after a pottery
kiln. In the elastic bond, a good grade of shellac is em-
ployed, while in the rubber bond, the particles of abrasive
material are held together by vulcanized rubber. In an-
other process, silicate of soda, sometimes called waterglass,
is used. All these bonds possess merit for specific purposes,
but as a matter of fact the majority of grinding wheels in
use at the present time are made by the vitrified process.
This bond is used so much more extensively than the others
that it is possible to obtain with it a greater range of grade
than is possible with other wheels. Again, years of ex-
perience, to say nothing of costly laboratory experimenta-
tion, have proven that the bond of a grinding wheel is
always a detriment to fast cutting, but as a bond of some
kind is, of course, a necessity the one that will produce
the least friction and at the same time produce the desired
grade is always preferable. Thus, the vitrified bond has
been found by practice to be the best adapted for the ma-
jority of purposes.
For the sake of clearness, all the above methods of wheel
manufacture will be considered separately. The selection
of correct bonding materials and the perfection of the various
66
71.
THE VITRIFIED PROCESS
processesinvolved is the result of many years of research
work and close study on the part of ceramic engineers and
experts on abrasives.
THE VITRIFIED PROCESS
As before stated, in the vitrified process, the binding
material is a good grade of kaolin, or other refractory or
fusible clay, which comes to the grinding-wheel manufac-
turer in carload lots, just as it is taken from the earth.
By means of standardized formulas, the chemist tests this
material to make sure that it comes up to a predetermined
standard. Otherwise several thousand finished wheels might
prove to be absolutely worthless. Further to test the value
of the bonding material, several small wheels and briquets
are made up and run through the kilns to make sure that
the material in question stands a satisfactory heat and
resistance test.
The foregoing may seem to the layman like an elaborate
procedure for the testing of a carload of clay, but eternal
vigilance is the watchword of the grinding-wheel manufac-
turer who desires to get new trade and successfully hold it
against competition. After it has been assured that the
bonding material is up to the correct standard, it is care-
fully ground and thoroughly dried and sifted.
The hardness, or resistance to wear, in a grinding wheel
is determined by the percentage of bond used with a cer-
tain amount of abrasive material. A hard wheel has a
heavy bond, while in a soft wheel, the percentage of bond-
ing material is less. To adapt an abrasive to many different
kinds of work calls for a variety of bonds, the most common
being the close tough and close brittle, open tough and open
brittle. It must also be borne in mind that bonds are em-
ployed to produce texture between these extremes. The
standardization of grinding-wheel bonds is the result of many
years of research work and actual experimentation. It is
needless to state that bond mixtures are kept as close secrets.
67
72.
ABRASIVES AND ABRASIVEWHEELS
In the manufacture of vitrified grinding wheels, there are
three methods used in mixing the abrasive material with
the bond; dry mixing, wet mixing and a combination of
both these methods. A dry mixed wheel is made by what
is known as the pressed process while a wet mixed wheel is
made by the puddled method. In a puddled and pressed
wheel, a combination of both mixing methods is employed.
In making wheels by the pressed process, the first step
is to determine the correct proportions of grain and bonding
material by weight, after which the mixture is dampened
a little and tumbled about in a tumbling barrel for a few
hours. The object of this procedure is twofold; to mix
the materials thoroughly and to surround each individual
grain of abrasive material with a matrix of bonding mixture,
to hold it in place in the finished wheel.
The mixed material now goes to the press room to be
formed into wheels. In this department are a number of
hydraulic presses, some of them capable of exerting a pres-
sure of 5,000 pounds per square inch. The process of
pressing a wheel is quite simple and easily carried out. An
operator carefully weighs out the correct amount of mixture
and places it in a steel mold of the desired size. After
leveling the mixture carefully, a cover that fits the bore of
the mold is placed on the wheel mixture and the mold placed
in position over the ram of the press. With his eye on the
pressure gauge, the operator opens the water inlet and as
the ram rises under the water pressure, and as the hand
of the pressure gauge mounts upward a crunching sound
is heard as the enormous pressure exerted by the water is
transmitted to the wheel in process of formation. When
just the exact pressure required is recorded by the gauge,
the operator opens the release, the ram descends and the
mold is removed. The pressed wheel is now taken from
the mold, ready for the vitrifing kiln.
Wheels made by the pressed process are very compact
but not necessarily hard. As an illustration, a Carborun-
dum wheel in O grade, G2 bond is a pressed wheel, al-
68
73.
-
THE VITRIFIED PROCESS
thoughit is six grades softer than an I grade wheel in B6
bond, which is a puddled wheel. On the other hand, a
Carborundum wheel in BI6 bond, which is made by the
puddled process, is very hard but not as compact as an I
grade wheel in G6 bond which is a pressed wheel, and
although six grades softer, it is more compact: It is seen
that the object of making wheels by the pressed process is
to make them compact, which characteristic is to be de-
sired in wheels for a variety of grinding purposes.
In making wheels by the puddled process, the correct
proportions of grain and bonding material are agitated for
several hours in mechanical mixers as shown in Fig. 10.
Fig. 10. Mixing the materials to form puddled wheels.
The mixture is then poured into a sheet-iron mold and
thoroughly dried by steam heat. After drying sufficiently,
which consumes several weeks for very large wheels, the
embryo wheel is placed on what is termed a shaving machine,
an illustration of which is shown in Fig. n. This machine
is constructed on the principle of a potter's wheel, consisting
of a revolving circular table upon which the wheel is placed,
and a cross-slide over which travels the head carrying the
tools used in shaping the wheel.
69
74.
ABRASIVES AND ABRASIVEWHEELS
The process of turning the wheel to the correct size and
shape, and boring the hole for the lead bushing, is com-
paratively simple although considerable skill is required in
turning wheels of irregular shape, such as certain wheels
for special tool grinders, cup wheels, large cylinder wheels,
Fig. II. Shaving grinding wheels preparatory to vitrifying.
recessed wheels for cylindrical grinding, etc. The wheel-
shaving operator is a skilled artisan in his particular line
of work, prosecuting his work by means of a blue print, or
other drawing, and obtaining the necessary dimensions by
means of scales and calipers such as are used by the machinist.
The next step consists of vitrifying the wheels. The
vitrifying kilns used by grinding-wheel manufacturers are
patterned after those used in the pottery industry for
vitrifying china and earthenware. They are approxi-
mately sixty -feet high and sixteen feet in diameter, being
constructed on what is called the down-draft principle.
A secondary interior wall is built inside the kiln, coming to a
70
75.
THE VITRIFIED PROCESS
crownabout twenty feet from the kiln floor. The heat is
so distributed that it circulates freely in all parts of the
kiln interior, finding an outlet at the bottom.
The wheels, as they come from the press and puddling
rooms, are placed in earthenware receptacles technically
termed sagers, a few of which are shown at the left-side
foreground of Fig. 12. As the wheels are in what is termed
Fig. 12. Loading a grinding-wheel kiln.
a "green" state, care is necessary in handling them. To
insure even bedding in the sagers, the wheels are placed on
a layer of sand. Several small wheels are loaded in one
sager but with medium-sized wheels, say 12x2, one to a
sager is considered sufficient. Wheels 14 inches in diameter
and over are piled one over the other in sectional sagers,
each wheel being bedded in sand.
An interior view of a grinding-wheel kiln is shown in
Fig. 13, wherein several piles of sagers are shown in the
background. After the kiln is completely filled, the door
is sealed tight and the kiln is ready for firing. To correctly
burn a kiln of grinding wheels is an operation calling for
long practice. It consists of bringing the kiln up to the
correct heat, keeping it there for the necessary period and
7 1
76.
ABRASIVES AND ABRASIVEWHEELS
then letting it cool gradually. Too much heat would result
in over-burning, the effect being the destruction of the bond,
leaving it in a burnt-up or honeycombed condition, while too
little heat would produce an under-vitrified wheel. Again,
if the kiln is brought up to full heat too rapidly, wheels
Fig. 13. Interior of a grinding-wheel kiln.
having hard and soft spots are liable to result. Further,
if the kiln is allowed to cool too rapidly 75 per cent, of its
contents will come out in a cracked state, being absolutely
of no value, for, unlike the good housewife's pie-crust,
grinding wheels cannot be worked over again.
Arranged around the base of the kiln, are approximately
ten fire boxes, the fuel used being a good grade of either
anthracite or bituminous coal. Two fires are started at a
time and allowed to burn for some time, after which two
more are started at regular intervals until all are burnr'ng.
The kiln is now brought up to the first, or red heat, which
takes fifteen hours. The heat is gradually increased until
the kiln is at what is termed the "low melting point."
Tests are frequently made by means of sets of pyrometric
cones which, are inserted in the kiln through test holes.
There are several of these test holes in every kiln arranged
at regular intervals and it is important that the readings of
each test hole tally, otherwise it is a sign that the heating is
uneven. The test cones are made of clays having different
melting points. Three cones having different melting tem-
peratures are placed on one base. When the first one melts
nd topples over, it is a sign that the kiln is at "red heat."
72
77.
THE VITRIFIED PROCESS
Thenext one succumbs at low melting point and when the
third one wilts under the heat, it signifies that the kiln is
up to full heat or a trifle higher than 2,500 Fahr. A set of
the cones used is illustrated in Fig. 14. For many years, the
pyrometrical cone was the only means used for determining
the heat of the kiln. Of late years, however, owing to the
Fig. 14. Pyrometric cones used for measuring degree of temperature in
grinding-wheel kilns.
high degree of perfection reached in the manufacture of
various types of pyrometers for accurately determining high
temperatures, the latter are now used in connection with the
former in grinding-wheel kiln burning.
After the kiln has reached full heat, it is sealed up and
allowed to cool for several days. As much care has to be
exercised in cooling the kiln as in heating it, for sudden or
uneven cooling would bring about disastrous results to the
contents. It takes three days to load a kiln, five days to
burn it, a week is allowed for cooling and three days for
unloading. Small wonder, then, that the grinding-wheel
manufacturer cannot ship special wheels a few days after
the order for the same has been entered. Burning a kiln of
grinding wheels is an operation that cannot be carried on
too carefully, as a slight error in judgment is sufficient to
turn success into failure. The men who have charge of this
important work become skilled through long experience, and
it is needless to state that they are numbered among the
grinding-wheel manufacturer's trusted employees.
From the kilns, the grinding wheels go to the sorting room
73
78.
ABRASIVES AND ABRASIVEWHEELS
where they are sorted according to size, grit and grade.
The grits and grades are determined by markings scratched
on the wheels while in the "green" state, before vitrifying.
The wheels are next inspected for soundness by tapping them
with a light hammer. A sound wheel will emit a faint, bell-
like tone when tapped, this tone having a distinct reverbera-
tion, whereas a cracked wheel gives out a dead sound in
which no reverberation is detected.
The wheels that pass this inspection go to the lathe room,
where they are faced and edged. The type of lathe used
for facing is not unlike an ordinary engine lathe with the
possible exception that the former is slightly heavier than
the latter. The wheel is firmly gripped in a universal chuck
and a cut taken over one side, bringing the surface as near
to a true plane as possible within practical limits. The
wheel is now reversed in the chuck and the other side faced,
care being exercised to make sure that the sides are parallel ;
otherwise the wheel might be out of balance, which feature
is to be avoided.
For facing large wheels, star-toothed dressers of the type
familiar to every mechanic are used. These are mounted
in suitable holders which are gripped in the tool post. For
fine, comparatively small wheels, diamonds mounted in
copper bars are used. Being in constant use, these stones
soon wear out; thus the diamond bill of the grinding-
wheel manufacturer amounts to a large sum annually.
After being faced, the wheels are ready for the first in-
spection for grade. This operation is done by hand as
shown in Fig. 15. The instrument used looks not unlike
a short, wide screw-driver mounted in a heavy handle. To
determine the grade, the operator depends wholly on his
senses of hearing and touch, which, through constant prac-
tice, are very reliable. The testing is done simply by
gouging into the wheel in several places, noting the sound
given out and feeling the amount of resistance met in separat-
ing the particles of abrasive from the bond.
Constant practice makes these operators very expert,
74
79.
THE VITRIFIED PROCESS
especiallyin grading medium hard, medium and medium
soft wheels. With the very hard wheels, however, it is
almost impossible to make an impression with the grading
tool. In this case, the operator relies almost wholly upon
the sound emitted. Several mechanical means have been
Fig. 15. Grading grinding wheels by the hand-test method.
devised for grading grinding wheels, but as yet not one has
been perfected that is as reliable as the simple hand-grading
tool in the hands of an expert.
The next step is to provide the wheels with lead bushings.
In this operation, the wheel is held in a special fixture which
locates it centrally. A mandrel of the desired size is now
inserted and the space between the mandrel and the grind-
ing-wheel hole filled with molten lead. As soon as the lead
cools sufficiently, the bushing is stamped with the grit and
grade, and, in the case of Carborundum wheels, the bond
also, as a means of permanent identification. This practice
originated with The Carborundum Company, and it is need-
less to state that it fills a long-felt want as the consumer
has at hand a reliable guide in duplicating a successful
wheel.
75
80.
ABRASIVES AND ABRASIVEWHEELS
The next operation is to true the periphery of the wheel.
This is done by men called wheel edgers. The wheels are
mounted on heavy grinding stands and the edging done by
means of star-shaped dressers fed by hand. Diamonds
are used on the smaller and more delicate wheels. The
grinding-wheel stands are equipped with guards to eliminate
danger from flying fragments in case a wheel should hap-
pen to burst, and the workman's health is also taken into
consideration as an efficient exhaust system is provided to
carry away the dust.
The wheels are now ready for another important oper-
ation, that of balancing. Owing to the high speed at which
they are operated, it is very necessary for grinding wheels
to be in almost perfect running balance. Carefully worked-
out tables, prepared by the engineering department, show
the exact amount any size of wheel can be out of balance,
and all wheels failing to come up to this predetermined
standard are rejected.
The balancing is done by mounting the wheel on an arbor
which is placed on balancing ways. If a heavy side is in
evidence, a weight of the required number of ounces allowed
on this particular size of wheel is clamped on the periphery
opposite the heavy side. If this weight fails to counter-
balance the wheel, it shows that the wheel is out of balance
to the extent of warranting rejection for the particular
size in question, although it can be turned smaller when,
in all probability, it will pass a satisfactory test. It is very
necessary that the balance of wheels intended for precision
grinding be almost perfect ;
otherwise accurate work on the
part of the grinding-machine operator is sometimes im-
possible.
Owing to the fact that grinding wheels are used under
various conditions, some of which are far from ideal,
chances for serious accidents owing to the bursting of the
wheel must be guarded against by the manufacturer who
aims to market reliable goods. To this end, grinding wheels
are given a speed test before going to the shipping-room.
76
81.
THE VITRIFIED PROCESS
Asthe centrifugal force of a body moving with different
velocities in the same circle is proportional to the square
of the velocity, it is evident that if the velocity is doubled
the centrifugal force will be four times as great. Thus it
is seen that if a wheel is speeded fifty per cent, faster than
the recommended operating speed, the centrifugal force
would be twice as great. The Carborundum Company
make a practice of speeding all wheels above eight inches
in diameter seventy per cent, higher than the recommended
operating speed. After this test, it is safe to assume that
the wheel is sound and when used under the proper oper-
ating conditions the danger of breakage is practically nil.
The speed-testing machines consist of substantial grinding-
wheel stands equipped with variable-speed counter-shafts
for increasing and decreasing the speed as desired, accurate
tachometers for registering the number of revolutions, and
stout, iron-bound oak boxes surrounding the wheels to
retain the fragments in case a wheel fails to withstand the
speed test. Two testing machines are shown in Fig. 16.
The tests are conducted in a very deliberate manner by
men whose integrity can be depended upon and at the com-
pletion of each day's work these men subscribe and swear
before a notary public to the tests they have made. The
number and conditions of each test are kept in a book pro-
vided for this purpose and a certificate is attached to the
tested wheel, showing both the test speed and the recom-
mended operating speed.
Accidents caused by grinding-wheel imperfections are
indeed very rare. The writer has personally investigated
many cases of broken grinding wheels and has yet to find
a case where the accident was caused directly by imper-
fections in the manufacture of the wheel. That all grinding-
wheel manufacturers intend to market dependable wheels is
borne out by the following paragraph taken verbatim from
The Carborundum Company's Number Five catalogue.
"In May, 1902, the Association of German Engineers
began an exhaustive series of speed tests of abrasive wheels.
77
82.
ABRASIVES AND ABRASIVEWHEELS
These tests were conducted by Professor Griiber of the
Technical High School, Dresden. All manufacturers were
invited to submit a 2o-inch wheel to be speeded until it
burst. About sixty wheels, including almost all standard
makes, were tested in this manner. The result, as a whole,
Fig. 1 6. Speed-testing grinding wheels for safety.
demonstrated the entire safety of all makes of wheels when
properly used; for, while the proper operating speed for a
2o-inch wheel is 955 revolutions per minute, the poorest
record made by any wheel tested was 2,615 revolutions
per minute before bursting. The regular grade of Car-
borundum wheel tested made 4,340 revolutions per minute
before bursting, which was the best record made by any
wheel tested."
The above statements bear out the writer's opinion, i. c.,
73
83.
THE SILICATE PROCESS
thatthe specific gravity of Carborundum, being less than
that of other abrasives, makes it a very efficient and safe
wheel.
THE SILICATE PROCESS
In making wheels by the silicate process, silicate of soda
and the abrasive material are first mixed together in the
proper proportions in mechanical mixers. This mixture is
then tamped by hand in iron molds. The operation of
tamping the mixture calls for a high degree of skill, thus
the work can only be intrusted to experienced men. Ma-
chines have been devised for tamping silicate wheels, but
the mechanical process does not produce as satisfactory
results as are obtained with the hand-tamping process.
Why this is so is a matter of conjecture. Nevertheless, the
fact remains that hand-tamped wheels are turned out in
large lots daily by grinding- wheel manufacturers.
On first thought, it would appear that silicate wheels
could be readily pressed in molds by the same process used
in making pressed vitrified wheels as heretofore explained.
This method has been the basis of lengthy experiments
without tangible results, the product always showing in-
ferior in actual tests.
The process of hand tamping is comparatively slow and
laborious as it has to be done in a thorough manner, but when
properly carried out excellent wheels are the result. After
tamping, the wheels are baked slightly under low heat,
which sets the bond. For many years it was considered an
impossibility to make Carborundum wheels by the silicate
process, inasmuch as the glassy nature of this abrasive
and the same characteristic in the bonding material, after
baking, did not form a good contact. Of late years, how-
ever, this difficulty has been overcome.
Silicate wheels are very close in texture and they are
successfully used on grinding operations where a compact,
but at the same time a comparatively free cutting wheel
is desired. For tool grinding in the machine shop, saw
79
84.
ABRASIVES AND ABRASIVEWHEELS
gumming and knife grinding in wood-working establish-
ments and on other operations of like nature, silicate wheels
are successfully used. Again, the silicate process is exten-
sively used by small grinding-wheel manufacturers who
have not the facilities for turning out vitrified wheels in
large lots. Further, an inferior abrasive, one containing
an excess of mica or garnet, for instance, can be used in
the manufacture of silicate wheels, whereas these impuri-
ties would ruin a vitrified wheel. Inasmuch as the silicate
process is of short duration, hurry orders for grinding wheels
can be filled in far less time than is required to make them
by the vitrified process. This factor is, of course, worth
consideration in a few specific cases.
In the early days of the grinding-wheel industry, the
silicate process was quite popular owing to the fact that
wire-web wheels, wherein a screen of brass wire was in-
serted, were considered as an ample safeguard against
accidents. At the present day, however, owing to the
high development of the vitrified process and the subse-
quent safety of the finished product, there is no logical
excuse for using silicate wheels purely as a matter of safety.
THE ELASTIC PROCESS
In making wheels by the elastic process, wherein the
binding medium is shellac, the first step is to melt the shel-
lac, which is afterward cooled and broken into lumps.
The lumps are next finely ground and the proper propor-
tions of shellac and abrasive mixed together. This mixture
is then transferred to a hot mold and thoroughly melted
under pressure. A slight baking in specially constructed
ovens completes the process.
Shellac-bonded wheels are very cool cutting, imparting
a high degree of finish to the work, and, owing to the firm
nature of the bonding material, they are the safest form of
wheel to use for any purpose. This bond is especially de-
sirable for comparatively thin wheels as used for grinding
80
85.
THE RUBBER PROCESS
outslots, fine saw gumming, marble coping, etc. Small,
delicate cup and dish wheels, as used for certain kinds of
cutter sharpening in the machine shop, are generally made
by the shellac process. For the finish grinding of the large
calender rolls used in paper making, the shellac bond is the
accepted favorite, owing to the high degree of finish im-
parted. Hones of various shapes used in polishing marble
are also made by this process.
The layman is inclined to associate shellac with the
sticky variety used in liquid form' by the pattern maker
and other wood workers and therefore is sometimes in-
clined to think that a grinding wheel bonded with this
material would soon fill up, and consequently refuse to cut.
Actual tests, however, have proven beyond all doubt that
the shellac-bonded grinding wheel is very free cutting;
probably owing to the fact that the heat used in baking
brings about a chemical change in the bond which elimin-
ates the tendency of the material to retain the minute
particles removed from the work by the action of abrasion.
THE RUBBER PROCESS
In cases where grinding wheels are subjected to very severe
strains, especially when very thin wheels are used, the
rubber process makes a very satisfactory wheel. Many
years ago, before the present-day state of perfection in
grinding-wheel manufacture, large wheels were made by
the rubber process, and in a very few cases, there is a demand
for these wheels at the present time. The majority of
rubber wheels used today, however, are comparatively thin
ones used for such purposes as grinding slots in cast-iron
stove doors, sawing stone, etc., or in fact for any operation
where an exceedingly durable wheel is desired.
The process of making rubber bonded wheels is quite
simple, consisting of passing carefully selected crude rubber
and abrasive material between steam-heated chilled iron
rolls. The material is passed and re-passed until all the
81
86.
ABRASIVES AND ABRASIVEWHEELS
abrasive material is thoroughly imbedded in the rubber.
When the required amount of material is worked up, the
Operator scribes a circle of the desired diameter on the
sheet of material with a pair of dividers, cuts the outline
thus made with a sharp knife, punches a hole in the center
of the disc and the wheel is ready for the final process, that
is vulcanizing the rubber. This is done in a small furnace,
electrically heated, and takes but a short time
87.
CHAPTER FOUR
ARTIFICIAL SHARPENINGSTONES
Properties of artificial stones Carborundum stones Method of manufac-
ture Bond Grit Grade Finishing Combination stone^-Carboran-
dum rubs.
to. 01 mar
i&s Carb
"
ARTIFICIAL
sharpening stones have been on the mar-
ket for many years, dating from the time when the
early grinding-wheel manufacturers put them on the market
in small lots. It is a fact that when any abrasive material
is crushed, much of the same is reduced to a fine powder,
which is of no value in the manufacture of grinding wheels.
Thus, one reason for the introduction of artificial "sharpening
stones in competition with the natural product was that the
grinding wheel and abrasive manufacturer sought a market
for the fine grains that otherwise have but little market
value.
Artificial sharpening stones possess one merit that should
not be undervalued, in that they are generally very uniform
in grit and grade. Absence of hard and soft spots is an-
other good characteristic which is not always present in
natural stones. Any good abrasive material can be made
into sharpening stones, but the artificial abrasives seem to
hold the preference, owing to their purity and uniformity as
compared to natural abrasives.
The first artificial abrasive to be put. on the market in the
form of sharpening stones was Carborundum. During the
last few years, the demand for these stones has advanced
by leaps and bounds, so to speak, two reasons being assigned
for this. First, they are carefully made by skilled workmen,
which procedure always results in a superior product, and,
83
88.
ABRASIVES AND ABRASIVEWHEELS
again, they are universally advertised, being on sale in
every town and city throughout the civilized world. Over
a million and a quarter of Carborundum sharpening stones
are sold annually in more than one hundred and fifty dif-
ferent sizes, styles, etc.
Carborundum sharpening stones are made in vitrified
bond by the pressed process, the principle being the same
Fig. -1 7. Finishing Carborundum sharpening stones on rotary laps.
as employed in making pressed wheels, with the exception
that the work is carried on on a smaller scale. Great care is
exercised in molding the stones. Careful workmen deter-
mine the amount of grain and bond mixture by weight;
thus, exactly the same amount of material is incorporated
into all stones of a given size. This material is evenly dis-
tributed in the mold, otherwise the finished stone would
have what is technically termed "heavy spots." Again,
the amount of pressure exerted on the mixture after the
mold is placed in position in the hydraulic press must be
84
89.
ARTIFICIAL SHARPENING STONES
watchedcarefully, otherwise the finished product would
vary in grade. As the stones are very delicate in the
"green" state, and thus easily damaged, it is necessary to
handle them carefully. They are loaded ;n sagers and
vitrified by the same process and in the same kilns used
in the manufacture of vitrified Carborundum wheels.
Carborundum sharpening stones are made in three grits,
Fig. 1 8. Part of the specialty department at The Carborundum Company's
plant.
namely, coarse, medium and fine. The coarsest grain is
used in number 120, while number 180 is used in medium
stones. Fine stones are made in F, FF, and FFF powders.
A superfine powder called 6o-minute powder (so called
because it takes 60 minutes to settle in water) is used in
making several very fine stones.
Large flat stones are made in G 7 bond for fine grits and
in G-5 bond for coarse grits. For other stones, points,
sticks, etc., G-i2 bond is used. For making razor hones
and other fine instrument stones a special bond is used to
give the desired hardness, the nature of this bond being
a trade secret.
85
90.
ABRASIVES AND ABRASIVEWHEELS
In making combination stones, that is, stones composed of
two grits, fine on one side and coarse on the other, two
methods are used. One method is to level the fine mixture
in the mold and over this place the coarse mixture, both
being pressed together. The other method consists of
cementing two finished stones, a coarse one and a fine one,
together.
After the stones come from the vitrifying kilns, they are
Fig. 19. A few varieties of Carborundum sharpening stones.
carefully inspected for imperfections such as cracks, burned
spots, etc., arid all imperfect specimens thrown aside. The
stones which pass this inspection go to the finishing de-
partment, where skilled artisans rub them smooth on hori-
zontal rubbing beds, or rotary laps. The abrasive used
in tliis operation is Carborundum grain mixed with water.
This operation is shown in Fig. 17.
The stones are now transferred to the specialty depart-
ment, where they are carefully buffed, cleaned, inspected
and packed in boxes and display cases. A view of this
department is shown in Fig. 18. As before stated, Car-
borundum sharpening stones are made in upwards of one
hundred and fifty different styles, being used for a diversity
of purposes too numerous to mention here. Some of the
well-known varieties are shown in Fig. 19.
A form of stone technically called a "rub" is much used
for smoothing castings, marble, granite, cement, etc. These
are made in the same manner as sharpening stones, with
the exception that the grits are coarser and no extra finish
is imparted after they come from the vitrifying kilns.
86
91.
ARTIFICIAL SHARPENING STONES
Considerableskill has been developed in the manufacture
of Carborundum sharpening stones 'and rubs, through the
study of proper bonding materials, methods of manufac-
ture, etc., thus the finished products are very uniform and
do not vary to any noticeable extent.
92.
CHAPTER FIVE
GRITS ANDGRADES
Designation of grits and grades Mixed grits ^rits of abrasive papers-
Standard grades Wheels Relation of speed to grade and grit Wheel
speeds for various operations.
THE grit, or grain as it is sometimes called, of a grinding
wheel alludes to the size of the particles of abrasive
material of which it is composed. Thus, a wheel in 24 grit
is made up of particles of abrasive material that were
separated from the mass that passed over the grading ma-
chine by a screen having 24 meshes to the linear inch.
It is sometimes erroneously stated that the particles of
grit composing a 24-grain grinding wheel are 1/24 inch in
diameter. This is not true, because the size of the wire of
which the screen is made must be taken into consideration.
Therefore, if the screen was made of very coarse wire,
the particles of grit passing through it would be somewhat
finer than those passing through a screen having the same
number of meshes per inch but made of finer wire.
Grinding-wheel grits are referred to as straight, mixed,
combination and combination mixed. A straight grit is
one wherein the abrasive is of one size only; thus if 40 grit
was used the wheel would be a 40 straight grit. For con-
venience, the word ''straight" is generally omitted in
speaking of a straight grit wheel. When a 40 grit wheel is
ordered, it is understood that a straight grit is required.
A mixed grit is one composed of two or three different
kinds of abrasive materials. Thus, a wheel designed for
grinding steel castings, for an illustration, made of a mix-
ture of emery, corundum and adamite, would be a mixed-
grit wheel.
88
93.
GRITS AND GRADES
Bya combination grit, which term is sometimes errone-
ously used to designate a mixed grit, is meant a combina-
tion of various-sized grits, scientifically selected, and in-
corporated into one wheel. A combination mixed grit is
one wherein two or more abrasives are used, the grains
being of different sizes.
A wheel composed of a combination of 24, 36 and 80
grit is known as a 24-combination grit. Successful grit
combinations are standardized only through long experi-
ment and actual tests, and the grinding-wheel manufacturer
generally keeps them secret. The Norton Company make
many combination grits, referring to them simply as 24
combination, 36 combination, etc. The Carborundum Com-
pany, who have investigated the theory and practical
results derived from combination grits in a very thorough
manner, have originated a simple means for designating
their grit combinations, which is of great benefit to the cus-
'tomer in re-ordering. They use a number of grit combina-
tions designated i, 2, 3, 4, etc. This number is annexed
to the grit number, thus a 365 combination grit has 36
grain for its base while 5 stands for the combination number.
For certain operations, combination grits offer decided
advantages. On cylindrical grinding, for instance, a wheel
in a combination grit with a comparatively coarse base,
24 to 36, cuts very fast and at the same time leaves a smooth
finish, leading to the deduction that the coarse grains
remove material rapidly, while the finer grains impart the
desired finish. On certain operations where a very durable
wheel is required, on car-wheel grinding, for example, a
combination grit gives entire . satisfaction, showing high
efficiency over a straight grit used for the same purpose.
Manufacturers of abrasive paper and cloth designate the
different grits by numbers: i, 1-1/2, 2, 2-1/2, etc. At one
time, the various grits used by different manufacturers
varied to quite an extent even though they were designated
by the same number. This often led to confusion and some-
times enabled one manufacturer to gain an unfair ad-
89
94.
ABRASIVES AND ABRASIVEWHEELS
vantage over another. For instance, a certain manufac-
turer of garnet paper uses a specified size of grain which he
calls No. 1-1/2. A competitor uses a slightly coarser grain
which he, too, designates as No. 1-1/2, and while the sizes
of the two grains are so near alike that detection with
the naked eye is impossible, it often happened that the
manufacturer using the coarser grain was enabled to show
a slight efficiency over his competitor, the consumer in the
meanwhile being ignorant of the fact that the grains were
not the same. To eliminate' misunderstandings among the
consumers, and to bring competition to a fair basis, the
majority of abrasive paper and cloth manufacturers of the
present day use the same sizes of grains for each grade.
Thus 2-1/2, for an illustration, designates a grain that has
passed through a standard sieve, the mesh of which has
been agreed upon.
In chinking of the various grit numbers used to designate
the sizes of abrasive papers and cloths, it is sometimes
advantageous to know how they compare with the grain
numbers commonly used in sizing abrasive materials. The
following table is authentic and up to date, being recently
furnished by The Carborundum Company.
Carborundum. Flint. Ga net. Emery. Aloxite.
FF
F
220
i 80 3/0 4/0 3/0 3/0
150 3/0 2/0 2/0
I 2O 2/O O O
100 O 2/0 100 100
90 1/2 O 1/2 1/2
80 I I
7O 1-1/2 1-1/2
60 I 1/2 2 2
50 1-1/2 1
40 2 1-1/2 2-1/2 2-1/2
36 2-1/2 2
30 2-1/2 3 3
24 3 3 3-1/2 3-1/2
20 3-1/2 3-1/2
90
95.
GRITS AND GRADES
Bythe expression "grade" we refer to the relative hard-
ness of a grinding wheel. In the early days of the grinding-
wheel industry, a few grades sufficed. These were known
generally as medium, medium hard, hard, medium soft and
soft. As the industry grew, however, and the grinding
wheel became adapted to a diversity of operations, closer
and more accurate grades were required which led to the
adoption of somewhat elaborate grade scales. A grade is a
certain value, within very close limits at least. An L grade
wheel offers the same resistance to disintegration by means
of the hand-grading tool as the grinding -wheel manu-
facturer's master block in the same grade. By way of
explanation, it may be well to state that all reliable grinding-
wheel manufacturers have a set of master grade blocks as
standards. These are carefully made from the correct
proportions of grain and bond to form the various grades,
and are referred to as a check in determining the actual
grade of doubtful wheels. Thus an M grade wheel made
by a reliable manufacturer is not somewhere between L
and M or M and N in which case it might be a de-grade.
De-graded wheels are used in some cases, to be sure, but
they are made as such. The Carborundum Company make
three de-grades: G plus, H plus, and I plus.
The various grinding-wheel manufacturers use different
markings to designate their various wheel grades. Some
use the letters of the alphabet (not always arranged the
same) while others use numbers, including whole numbers,
mixed numbers and fractions. All grinding-wheel manu-
facturers have comparative grade lists, the object of which
is to show the difference between their grades and those
of their competitors. The writer has, from time to time,
examined and compared many of these grade lists and,
unfortunately, they vary to such an extent that it is an
impossibility to state for a fact which one is absolutely
correct.
To compile a comparative grade list that would satisfy all
grinding-wheel manufacturers, and, at the same time, im-
91
96.
ABRASIVES AND ABRASIVEWHEELS
part reliable information to the layman, the writer used the
following method in arranging the list here given. Taking
Norton Company's grade list as a basis, a chart was drawn
up on tracing paper including the letters used, with spaces
between each for de-grades. A number of blue prints were
made from this chart, one being sent to every prominent
grinding-wheel manufacturer in this country with the request
that they fill in on the same, their wheel grades, showing
the comparison with Norton Company's grading. Many
complied with the request, while some declined, and the chart
in question was compiled from the date thus obtained.
Inasmuch as every individual grinding-wheel manufacturer
knows more about his own grades than does his competitors,
and supplied his wheel grades in comparison to a given
standard, in this case Norton Company's grading, it is safe
to assume that a comparative grade scale compiled in this
manner is as reliable as it is possible to arrange the same.
The grinding-wheel manufacturers who use the letters
of the alphabet in regular order as a grade scale designate
the letter M as showing their medium grade. This has led
many technical writers who are not conversant with the
grinding-wheel industry to show the comparison between
Carborundum and Alundum wheels with the two M's
together. This is a fallacy, as The Carborundum Com-
pany's M grade is equal to Norton Company's K, which
brings the L's of both grade scales together. While both
The Carborundum Company and Norton Company con-
sider their respective M grades as medium, they do not
agree as to what constitutes a medium grade.
It is to be regretted that the various grinding-wheel
manufacturers do not standardize on a universal grade
scale, which procedure, it is needless to state, would elim-
inate much confusion. In all probability they will never
agree on a universal grade scale, the nature of which would
cause them to abandon their gradings for a standard already.
92
ABRASIVES AND ABRASIVEWHEELS
in use, but perhaps if they all agreed to adopt a universal
grade scale, the nature of which would cause every manu-
facturer to discard his present grade scale and adopt a new
one, the change might be brought about.
By referring to the bottom of the comparative grade
scale here shown, it is seen that the writer has had the pre-
sumption to take a step toward standardizing wheel grades.
Figures i to 22 are used, a space being left between each
for de-grades. Thus The Carborundum Company's G-plus
grade would be designated 13 plus. A leading grinding-
wheel manufacturer, with whom the writer had some cor-
respondence regarding wheel grades, has the following to
say concerning a standard grade list: "Nevertheless, go
ahead. We will never get anywhere unless some one makes
the attempt." If a universal grade scale is to be adopted
eventually, the one shown has merit in one respect that
should not be undervalued; that is to say, it would require
each manufacturer to discard his present grade scale, put-
ting all on the same level. In this case, no one manufac-
turer would be in a position to 'state that other manufac-
turers adopted his grade scale because it was the most com-
prehensive, or because he was regarded as the leading grind-
ing-wheel manufacturer.
It is often stated on good authority, that it is impossible
to arrange a grade scale which is absolutely reliable in all
respects and cases. In a measure, the above statement is
correct, owing to the fact that the abrasive efficiency of
wheels of the same grade, but made of different abrasives,
or combinations of different grits, is not always the same.
For an illustration, a Carborundum wheel in 20 grit, G-plus
grade, is universally acknowledged to be highly efficient
for grinding gray iron castings. Now if we should test an
Alundum wheel in Q .plus, which corresponds in grade to
Carborundum G plus, the latter would prove low in abrasive
efficiency because Alumdum is an alumina abrasive not
adapted for grinding materials of low tensile strength.
Again, suppose we had a wheel made of pure corundum in
94
99.
GRITS AND GRADES
46grit, M grade, vitrified bond and tested it in competition
with a wheel made of the same material, in the same grit
and grade, bonded by the silicate process. In this case, we
would find that the wheel made by the vitrified process would
show the highest efficiency, inasmuch as the silicate bond
is closer;
thus making the wheel more compact and less
free in cutting. Further, if we should test a wheel in a
combination grit against one in a straight grit, both being
of the same material in a like grade, one will show high
efficiency over the other. However, let it be assumed that
several manufacturers agreed to make a 24 x 3 wheel in
20 grit, 13 universal grade for the purpose of grinding drop
forgings, and let it be further assumed that they used the
same material, which could be corundum from one mine,
Aloxite, Alundum, Boro-Carbone, or in fact any standard
abrasive. In this case, it is very probable that the abrasive
efficiency of the several wheels would be so close that it
would require the services of an expert abrasive engineer to
accurately determine which wheel really was the most efficient.
It may seem out of place
'
to many to consider wheel
speeds in connection with grades, but, as a matter of fact,
one bears on the other to a remarkable degree, as shown
in the data supplied by the Abrasive Company in another
chapter. Let it be assumed that we are using a wheel
made of artificial corundum for grinding the flash marks
from drop forgings, running the same at a peripheral speed
of 5,000 feet per minute, and that the wheel seems to wear
readily. We state at once that the wheel is too soft. How-
ever, if we speed up the wheel slightly, say to a peripheral
speed of 5,300 feet per minute, it seems to appear harder,
for while it cuts just as good as it did previously, it does
not wear away so readily. Again, if at a surface speed of
5, ooo* feet per minute the wheel glazed and refused to cut,
the objection could be overcome by reducing the speed
slightly. In other words, it is a good rule to speed up a
wheel that appears soft and to decrease the speed of one
that seems to be unduly hard.
95
100.
ABRASIVES AND ABRASIVEWHEELS
From the foregoing, it is seen that speed has everything
to do with, what the writer will call for want of a better
expression, the running or working grade. As wheels wear
away, their speed should, of course, be increased slightly
to keep them working at their maximum efficiency. It is
not always possible to do this, however, and hundreds of
thousands of grinding wheels are worn out prematurely.
To overcome this difficulty by providing a constant work-
ing grade, regardless of the peripheral speed, an American
inventor recently obtained a patent on a grinding wheel
having a gradually increasing grade from the periphery to
the hub. Thus as the wheel wears, its hardness at the
periphery keeps increasing, which offsets the tendency to
wear away rapidly, owing to the reduced surface speed.
Wheels made by this process should be productive of
economical results.
For different grinding operations, wheel speeds vary
to quite a remarkable degree. The following table shows
the speeds generally recommended for various grinding
operations.
Cylindrical grinding.
Surface grinding
Automatic knife grinding
Automatic knife grinding
Drill grinding
Tool grinding (dry)
Tool grinding (wet)
Cup wheels in general . . .
General grinding
Set-up polishing wheels. .
Vulcanite wheels
5,000 to 7,000 feet
4,000 to 5,000
2,500 (disc wheels)
2 ,000 (cup wheels)
4,000 to 4,500
4,000
3>500
3,500
5,000
7,500
10,000
minute
 Most read
 Most read
 Most read